
6061 aluminum heat-treatment guide
How to Anneal 6061 Aluminum at 775°F: Cooling and Verification Guide
A legacy ASM reference for wrought 6061 uses about 775°F (415°C), a 2–3 hour hold and furnace cooling at about 50°F per hour to 500°F (260°C). That is a starting reference, not a universal recipe: a NASA 6061-O process used a one-hour hold. The governing specification and a validated facility procedure must define the actual soak, monitoring and acceptance requirements.

The drawing and service requirement must allow the strength loss that comes with a full anneal.
Use the approved metal-temperature target, soak criterion and cooling profile for the actual product and load.
Record alloy, temper, load profile, dimensions and the property or forming evidence required by the job.
Also stop when the assembly, distortion limit, furnace capability or certification route is not approved.
Quick answer
What Is the 775°F Annealing Schedule for 6061 Aluminum?
Full annealing changes the material state. It makes 6061 easier to bend and form, but it removes most of the precipitation strengthening that makes T6 and T651 useful. If the finished part must keep its original strength, 775°F full annealing is usually the wrong default.
For the typical route discussed here, the important temperature is the actual metal temperature. A controller can show 775°F before a heavy part or the center of a load has reached it. The same problem exists during cooling: a programmed 50°F-per-hour ramp is only a command until a qualified load profile proves what the metal did.
Scope boundary: this page is a process-planning guide for wrought 6061. It is not a released furnace procedure, product certification, aerospace process approval, home-oven instruction or substitute for the applicable material specification.
Choose the right route first
When Should You Anneal 6061 Aluminum at 775°F?
Start with the finished-part requirement. A full anneal is appropriate only when the job can accept a much softer final condition. The table links each common situation to an action, the evidence needed and a clear stop boundary.

| Condition | Recommended starting action | Evidence required | Stop boundary |
|---|---|---|---|
| Severe forming; lower final strength is allowed | Investigate a full-anneal trial on representative 6061. | Material identity, load-temperature record, bend/forming result, dimensions and required property tests. | Stop if the drawing or service requirement still calls for T6/T651 properties. |
| Only limited softening is needed | Review bend radius, stock temper, forming sequence or a separately qualified partial-softening route. | Representative bend trial, springback, cracking, dimensions and final strength requirement. | Do not invent a lower-temperature recipe when no approved process or property evidence exists. |
| A machined T651 part is moving | Perform a residual-stress and machining-sequence review before choosing heat treatment. | Free-state dimensions, stock history, machining order, fixture influence and allowable property change. | Stop if the geometry or strength cannot tolerate stress release and loss of the original temper. |
| Certified 6061-O feedstock is required | Compare buying certified O-temper material with using a qualified heat treater. | Certificate of conformance, invoked product specification, traceability and required acceptance tests. | Do not label material 6061-O from the thermal chart alone. |
Swipe or scroll sideways to compare all four decision columns.
Typical full-anneal route
What Is the Full 6061 Annealing Cycle?
A defensible cycle links the part identity, approved temperature channels, soak criterion, controlled cooling and acceptance evidence. A legacy ASM table and a published NASA process use the same 775°F-to-500°F endpoints but different hold times, which is why the applicable procedure must control.
Parts must be clean, dry and free of uncontrolled oil, solvent, paint, adhesive, polymer, loose chips and sealed or pressurized cavities. Classify, ventilate and interlock the furnace for the actual load and any vapors it can release.
Space parts for circulation. Support thin panels and complex shapes against sagging, but avoid fixtures that produce uneven contact, cosmetic marks or large thermal gradients.
During process development, measure slow-heating, fast-heating, thick, thin, center and edge locations as needed. Routine sensor requirements then follow the approved pyrometry plan.
The furnace display can reach 775°F before the workpiece does. Begin soak only when the governing procedure’s required channels satisfy its start criterion. One thermocouple proves only its local temperature, not whole-load uniformity.
The legacy ASM table lists 2–3 hours for typical 6061 full annealing, while NASA documented one hour for its qualified test material. Product form, section, load and invoked specification control the production value.
Demonstrate product response during qualification and monitor production with the approved pyrometry plan. A controller command alone does not prove the load followed the intended curve.
Review the chart, identification, dimensions, distortion, surface condition, hardness and the property tests specified by the job. A subjective “soft feel” is not controlled evidence.
Published schedule provenance: the NIST-hosted ASM Handbook chapter presents typical, not universally optimum, annealing treatments. NASA TP-20230013695 (2023) documents a separate 6061-O preparation using a one-hour hold at 775°F and controlled cooling to 500°F at no more than 50°F/h.
Furnace safety boundary: aluminum at 775°F may not visibly glow. Use controlled hot-part identification and handling, and select PPE through the workplace hazard assessment. Quenching belongs to a different thermal route and introduces separate splash, steam, handling and distortion hazards. The legally adopted furnace and workplace requirements in the operating jurisdiction control.
Interactive planning aid
6061 Cooling-Time PlannerCalculate the arithmetic for a 775°F-to-500°F reference segment and a user-entered hold. The tool does not approve the rate, choose the soak, qualify the furnace or certify the final temper.
At 50°F/hour, cooling from 775°F to 500°F takes 5.5 hours. With a 1-hour entered hold, the calculated time from hold start to 500°F is 6.5 hours.
Furnace control
Why Must You Measure Metal Temperature Instead of Furnace Setpoint?
“Load temperature” means the temperature of the aluminum at a representative location. It is not automatically the same as the controller display or furnace-air sensor.
A dense batch stores more heat and can lag during heating or remain hotter during a programmed cool.
A thin sheet and thick boss may not follow the same curve. Measure locations that represent both risks.
Tightly nested parts restrict circulation. A qualification run must represent the production stack and support method.
Fan pattern, door leakage, element cycling and work-zone uniformity change the relationship between setpoint and part.
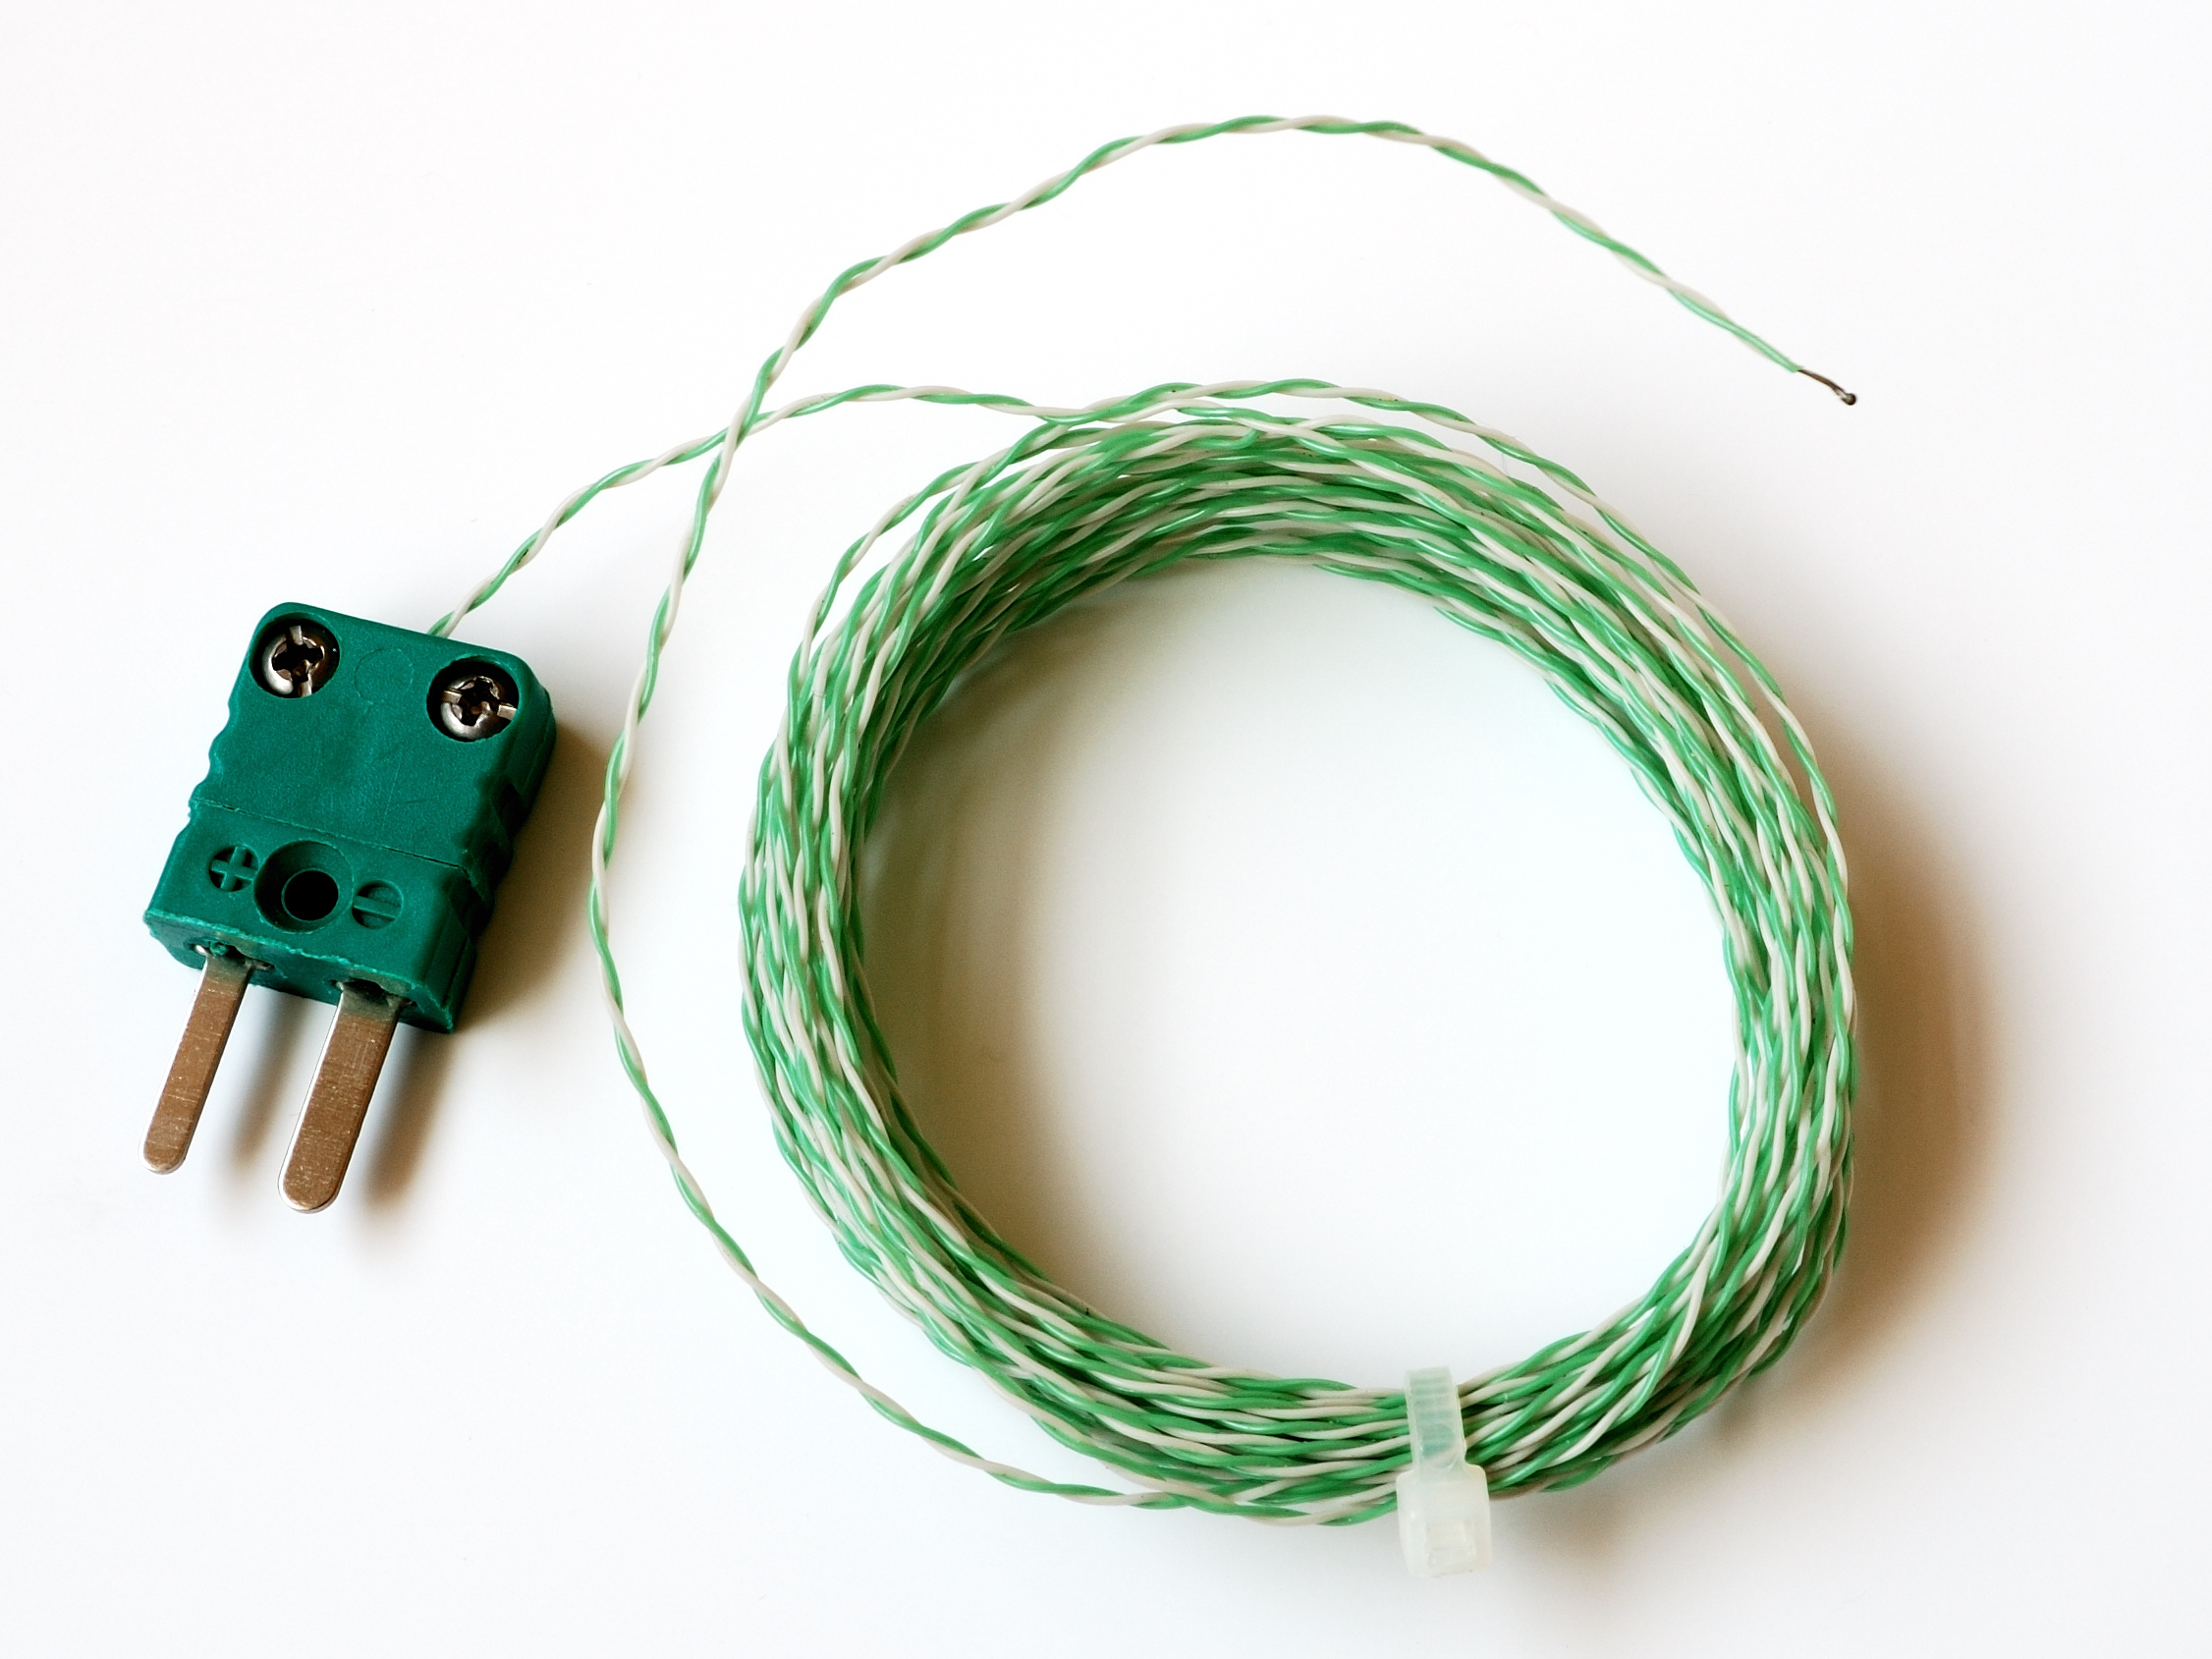
Thermocouple type, attachment, wire routing, recorder accuracy, calibration and cold-junction compensation can affect the record.
Practical rule: use representative load thermocouples or an approved correlation during qualification to show how the product follows furnace temperature. Routine monitoring then follows the released pyrometry plan. AMS2750H addresses sensors, instrumentation, system accuracy tests and temperature-uniformity surveys when it is invoked.
What the heat changes
What Happens to T6 and T651 During Full Annealing?
6061 gains useful strength from magnesium-silicon precipitation. A full anneal deliberately changes that distribution so the alloy becomes softer. The benefit is formability; the cost is strength and hardness.

| Condition | Plain-language meaning | Relative formability | Relative strength | What the 775°F full anneal does |
|---|---|---|---|---|
| 6061-O | Annealed condition released under the applicable product and property requirements. | Highest of these three | Lowest of these three | The route is intended to approach an annealed condition, but schedule compliance alone does not certify it. |
| 6061-T4 | Solution heat treated and naturally aged to a substantially stable condition. | Often better than T6 | Below T6 | Removes the T4 condition. Later artificial aging changes the temper designation and must follow an approved route. |
| 6061-T6 | Solution heat treated and artificially aged. | Lower than O; forming limits matter | High | Removes most precipitation strengthening. It is not a T6 restoration cycle. |
| 6061-T651 | T6-type condition with specified stress relief, commonly by stretching for relevant product forms. | Process-dependent | High | Removes the strength condition and the purpose of the original stress-relieved temper. |
Swipe or scroll sideways to compare every temper column.
Do not mix thermal routes
How Is Full Annealing Different from Restoring T6?
The 775°F route aims for softness and uses slow cooling. T6 production uses solution heat treatment at a higher temperature, rapid quenching and controlled aging. One cannot be substituted for the other.

Nominal 775°F metal temperature, typical hold, then slow controlled cooling to promote a soft condition.
Uses a substantially higher approved temperature to place soluble constituents into solid solution.
Rapid cooling preserves a supersaturated condition. This cooling objective is the opposite of the slow full-anneal ramp.
Controlled lower-temperature treatment develops precipitation strength after solution treatment and quench.
Acceptance evidence
How Do You Verify a Successful 6061 Anneal?
Hardness and eddy-current conductivity can support inspection only when the invoked specification defines the method and limits. Scale, thickness, support, surface condition, calibration, lift-off and specimen temperature can affect the result. Neither measurement alone identifies O temper or replaces required tensile testing and traceability.
Confirm alloy, product form, starting temper and lot or supplier certificate when required. A perfect chart cannot correct unknown material.
Review work-zone/furnace status, sensor identification, actual load-temperature curve, hold start/end, cooling rate and deviations.
Measure after supports and fixtures are released. Check sagging, twist, flatness, oxidation, imprints and any orange-peel risk after forming.
Use the method, scale, thickness limits, surface preparation and acceptance band required by the quality plan. Treat results as part of the evidence set.
Where service risk requires it, use tensile, bend, formability or other tests selected by the product specification or responsible engineer.
Define who can identify the final condition and what furnace, load, fixture, cycle or material changes require review.
Welded and assembled parts
What Changes When the 6061 Part Is Welded or Assembled?
Welding already softens areas near a 6061-T6 joint. Heating the completed assembly to the full-anneal range extends the low-strength condition across the part and can release restraint or distortion.

Review every component before heating
Filler metal, braze or solder, fasteners, inserts, seals, adhesives, coatings and dissimilar alloys can have different temperature limits. Correctly controlled 775°F treatment is far below Hydro’s published 6061 melting range, but another assembly material may fail earlier.
Expect dimensional movement
Residual stress can relax as the part softens. Fixtures may prevent movement during the cycle and then reveal distortion after release. Measure the free part, not only the clamped part.
Do not call the result “restored T6”
Full annealing removes strengthening; it does not reverse weld-zone property loss. Any later strengthening route must be approved for the alloy, product, filler, geometry and service.
Oceanplayer Laser’s role: we can help review how material condition affects an aluminum welding trial and equipment discussion. Formal furnace heat-treatment approval and temper certification belong to the responsible material/process authority and qualified heat-treatment provider.
Troubleshooting
How Do You Troubleshoot a 6061 Anneal That Missed the Target?
Start with evidence. Reheating the load without identifying the cause can increase distortion, oxidation or grain problems while making traceability worse.
| Observed condition | Likely causes to investigate | Evidence to collect first | Safe corrective direction |
|---|---|---|---|
| Properties vary across the load | Part temperatures did not follow the same curve; load spacing, mass or circulation changed. | Compare center, edge, thick and thin thermocouple records; inspect the rack and batch pattern. | Requalify the representative load and lock the spacing, support and recipe. Do not average away a cold or hot location. |
| Part remains too hard | Wrong alloy/temper, insufficient metal hold, rapid cooling, poor sensor placement or incomplete equalization. | Traceability, metal-temperature chart, soak timing, cooling segment and hardness method. | Diagnose before reprocessing. Confirm the required final condition and revise only the approved procedure. |
| Part distorts or sags | Unsupported geometry, uneven fixture contact, thermal gradients or residual-stress release. | Pre/post free-state dimensions, support marks, temperature differences and fixture-release measurements. | Improve support, spacing and thermal uniformity; validate with representative parts and acceptance datums. |
| Surface becomes rough after forming | Grain-size sensitivity, prior cold work, incoming product condition or excessive exposure. | Incoming form/temper, deformation history, furnace exposure and surface/microstructure evidence. | Use the minimum validated exposure, review stock condition and qualify the forming route. Do not assume a hotter or longer cycle helps. |
| Customer expects original T6 strength | The process goal was confused with solution treatment and aging. | Drawing, material specification, structural allowables and purchase requirement. | Stop release. Select another forming route, buy a different temper, or use a qualified solution-treatment/quench/age process if permitted. |
| Controller shows a perfect 50°F/h ramp | The recorder may show setpoint or furnace air rather than the slowest metal location. | Channel definitions, thermocouple placement, recorder mapping and load correlation study. | Treat the result as planning data until the metal profile is demonstrated. |
Swipe or scroll sideways to compare causes, evidence and corrective direction.
Illustrative decision scenarios — not reported customer results
Should You Anneal In-House or Buy 6061-O?
Tight-radius sheet bracket
The shop has known 6061-T6 sheet and the design can accept an annealed final condition. A representative full-anneal trial may be reasonable. The team should qualify the actual sheet, bend radius, surface appearance, springback, distortion and final property acceptance before releasing production.
Machined T651 fixture
The fixture is moving after machining, but it must retain strength and precise geometry. A blanket 775°F anneal is a poor default because it removes the intended temper and can release more distortion. Review stock stress, machining sequence, fixturing and allowable thermal treatment first.
Buyer needs soft 6061 feedstock
Purchasing certified 6061-O from a qualified supplier may be simpler than buying T6 and converting it in-house. Compare minimum quantity, lead time, product availability, certification, internal furnace qualification, inspection cost and rework risk—not only raw stock price.
Buyer and supplier handoff
What Should You Include in a 6061 Heat-Treatment RFQ?
A useful RFQ tells the heat treater what the material is, what the finished part must do and what evidence must accompany it. “Anneal at 775°F” is not enough.
Frequently asked questions
Frequently Asked Questions About Annealing 6061 Aluminum
What temperature and hold time are used to fully anneal 6061 aluminum?
A legacy ASM table lists a typical full-anneal target of about 775°F (415°C) for 2–3 hours, followed by slow cooling. NASA TP-20230013695 used 775°F for one hour for its specific 6061-O preparation. The difference matters: the governing specification, product form, load and qualified facility procedure must set the production hold.
How long does 6061 take to cool from 775°F to 500°F?
At a reference rate of 50°F per hour, 275°F divided by 50 equals 5.5 hours. That is arithmetic only and excludes heat-up, equalization, hold and final cooling. For the cited legacy route, air cooling can begin after 500°F; another approved procedure may require different instructions.
Does annealing 6061-T6 or T651 at 775°F remove the temper?
Yes. A full anneal removes most precipitation strengthening, so the part cannot be treated as unchanged T6 or T651. T651 also represents product-form-specific stress-relief history. If the design needs those properties, stop and choose a different forming, stock-temper or approved heat-treatment route.
Can 6061 be returned to T6 after a full anneal?
Potentially, but not by aging alone and not for every finished part. Re-establishing T6 requires approved solution heat treatment, quenching and artificial aging, plus the specified property and dimensional checks. Assemblies, welds, fillers and quench distortion may make the route impractical. T651 normally cannot be recreated merely by reheating a finished part.
Can a household oven be used to anneal 6061?
No. A household or food oven is not suitable for controlled production heat treatment, certified parts or safety-critical work. It normally lacks qualified temperature uniformity, traceable records and industrial safety controls. Contaminated or assembled parts can also release vapors or create fire, pressure and handling hazards.
How do you prove the metal reached temperature and the anneal worked?
During qualification, use representative load thermocouples or an approved correlation to show how the product follows furnace temperature. Then combine material traceability, the complete thermal record, free-state dimensions, surface inspection, hardness or conductivity only when the invoked specification defines them, and any required forming or mechanical tests. One sensor or one hardness reading is not enough.
Our team creates practical guides on laser cleaning, welding, marking and industrial automation. We combine application experience with cited engineering sources to help manufacturers compare materials, evaluate processes and plan equipment trials with clearer requirements.
Technical references
Sources and engineering boundariesThe cycle is based on established heat-treatment references, while production release must follow the current licensed specification, customer drawing and qualified facility procedure that apply to the part.
- NIST-hosted ASM Handbook chapter: Heat Treating of Aluminum Alloys — typical full-anneal schedules and metallurgy context.
- NASA TP-20230013695, Assessing Flow Formability of Aerospace Aluminum Alloys via DIC Tensile Testing (2023) — its material-preparation section documents a 6061-O cycle with a one-hour hold at 775°F and controlled cooling to 500°F at no more than 50°F/h.
- SAE AMS2770R — heat treatment of wrought aluminum alloy parts; consult the licensed standard for controlled work.
- SAE AMS2772H — heat treatment of aluminum alloy raw materials.
- SAE AMS2750H — pyrometry requirements relevant to furnace instrumentation and system control.
- SAE AMS2658E, revised May 2026 — hardness and conductivity inspection of wrought aluminum alloy parts when the specification is invoked.
- The Aluminum Association: Aluminum Standards and Data 2024 — alloy, temper, properties and product context.
- Hydro Alloy 6061 technical data — alloy properties and melting-range orientation.
- SAE ARP7500, reaffirmed July 2024 — recommended practice for minimizing high-temperature oxidation during aluminum heat treatment.
- NFPA 86:2027, Standard for Ovens and Furnaces — current furnace-safety reference; the edition legally adopted by the operating jurisdiction may differ.
- OSHA 1910.132 and OSHA 1910.147 — PPE hazard assessment and lockout/tagout requirements in relevant U.S. workplaces.
Plan the whole process
Send the alloy, temper, geometry and final requirement—not only “775°F”Oceanplayer Laser can help connect the aluminum condition to a welding or fabrication trial. Share the actual material, joint or part, earlier processing and acceptance goal so the equipment discussion starts with the real manufacturing problem.