

6061 vs 2024 Aluminum for Aerospace
Choose 2024 when a qualified, protected wrought part needs higher strength. Choose 6061 when corrosion resistance, extrusion, welding, or easier fabrication carries more weight. The final choice still depends on the exact temper, product form, load path, environment, joining route, and approved program data.
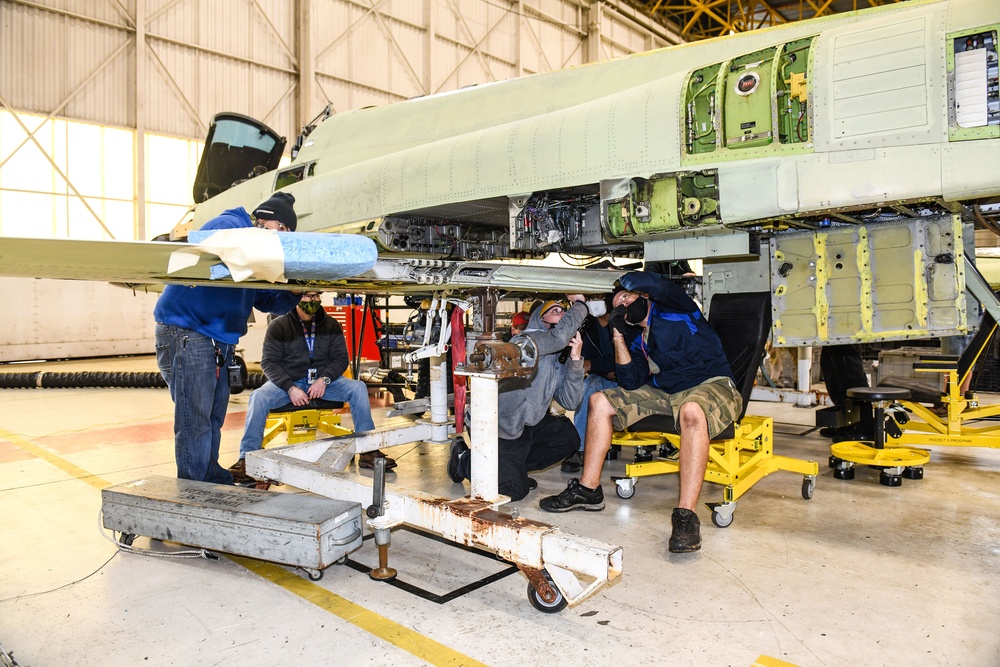
Common 2024 tempers provide a stronger starting point for qualified sheet, plate, fittings, and machined load-carrying details.
6061 offers a balanced route for extrusions, frames, enclosures, tooling, ground equipment, and weldable assemblies.
2024-T3 sheet is not the same article as 2024-T351 plate; 6061-T6 extrusion is not interchangeable with every 6061 product.
Use the governing drawing, specification, approved allowable source, qualification route, and actual supplier evidence.
Which alloy is the better aerospace starting point?
The answer changes with the article. A fastened wing-skin detail, a machined fitting, a welded equipment frame, and a ground-support enclosure do not share the same governing requirement.
Strength and protected wrought-product performance lead
2024 is an aluminum-copper-magnesium 2xxx alloy. In the cited producer data, 2024-T4/T351 has much higher typical ultimate tensile strength and moderately higher yield strength than 6061-T6/T651. That makes it a credible starting point when a design uses qualified sheet, plate, bar, or a machined fitting and can support the required corrosion-control and inspection system.
- Likely manufacturing routeForming, machining, fastening, bonding, or another program-qualified joining method.
- Likely control burdenExact temper and form, grain direction, cladding or coating, faying surfaces, fastener interfaces, drainage, and traceability.
- Important limitDo not select 2024 only because a typical tensile number is higher. Buckling, bearing, fatigue, fracture, corrosion, and certification can govern.
Fabrication, corrosion, and extruded geometry lead
6061 is an aluminum-magnesium-silicon 6xxx alloy. It provides moderate strength with much friendlier corrosion and fusion-welding behavior. It is often the practical choice for extrusions, frames, brackets, housings, fixtures, tooling, ground-support equipment, and permitted aerospace articles that benefit from a weldable route.
- Likely manufacturing routeExtrusion, forming, machining, fastening, brazing, or qualified welding.
- Likely control burdenExact temper, extrusion or plate specification, dimensions, post-weld HAZ properties, distortion, finish, and traceability.
- Important limitCalling 6061 weldable does not preserve T6 base-metal strength beside the weld. The finished joint needs its own qualified property basis.
A part must be selected as a system: load spectrum, stiffness, thickness, product direction, fasteners or welds, corrosion exposure, surface protection, manufacturing history, inspection access, repair route, and governing approval data. For aircraft maintenance, current manufacturer instructions and applicable approved data take precedence over a general comparison.
How Do 2024-T4/T351 and 6061-T6/T651 Properties Compare?
The table below uses one producer's typical sheet, coil, and plate data so the direction of the trade-off is easy to see. It does not provide minimum design values for every thickness, direction, product, or program.
| Property at the stated producer condition | 2024-T4/T351 | 6061-T6/T651 | How an engineer should read it |
|---|---|---|---|
| Ultimate tensile strength | 68 ksi / 469 MPa | 45 ksi / 310 MPa | The cited 2024 condition has a large screening advantage. Do not convert this typical comparison into a universal section reduction. |
| Yield strength | 47 ksi / 324 MPa | 40 ksi / 276 MPa | The yield gap is smaller than the ultimate-strength gap in these listed conditions. |
| Elongation, 4D | 19% | 17% | Specimen, thickness, direction, form, and temper matter. This is not bend-allowance data. |
| Elastic modulus | 10.6 Msi / 73.1 GPa | 10.0 Msi / 68.3 GPa | Stiffness differs much less than strength. Geometry often has more leverage on deflection and buckling. |
| Shear strength | 41 ksi / 283 MPa | 30 ksi / 207 MPa | Useful for initial comparison only; real joints also need bearing, bypass, fastener, edge-distance, and direction checks. |
| R.R. Moore endurance figure | 20 ksi / 138 MPa | 14 ksi / 97 MPa | Both producer tables state 5 × 10⁸ reversed-stress cycles. This is not a spectrum-fatigue allowable or a universal fatigue limit. |
| Nominal density at 20°C | 2.77 Mg/m³ | 2.70 Mg/m³ | The rounded difference is about 2.6%. Required geometry and allowable-driven section size can matter far more to finished mass. |
| Thermal conductivity at 20°C | 120 W/(m·K) | 167 W/(m·K) | Confirm temperature and product condition before thermal modeling or heat-input decisions. |
A thin panel can be buckling-limited and a beam can be stiffness-limited. If elastic modulus changes only modestly, section shape and boundary conditions may dominate.
Mean stress, holes, fretting, surface condition, corrosion, residual stress, load sequence, direction, and inspection interval all affect crack initiation and growth.
2024 is slightly denser, yet higher usable strength can support a different section. The lightest compliant article emerges from the full design, not a density row.
Which Alloy Fits Your Aerospace Application?
Choose the closest article and manufacturing route. The result helps organize the next engineering question; it does not select or approve flight hardware.
A certified or flight-critical article cannot be released by an online alloy comparison. Establish the design authority and allowable set first.
- Screening directionCompare the exact product, temper, orientation, protection, and joint route already permitted by the program.
- Evidence to requestDrawing and specification revision, approved allowables, mill certificate, heat/lot traceability, and special-process qualification.
- Failure mode to closeStatic strength is only one check; include fatigue, fracture, bearing, buckling, corrosion, joining, and inspection access as applicable.
- Do not assumeDo not substitute 6061 for 2024, or 2024 for 6061, without the required engineering and quality approval.
Why Do Temper and Product Form Change the Comparison?
A callout that says only "2024 aluminum" or "6061 aluminum" is incomplete. T3, T351, T6, and T651 describe different processing histories, while sheet, plate, extrusion, bar, tube, and forging have different specifications and property bases.
Do not compare a thin Alclad 2024-T3 sheet value with a thick 6061-T651 plate value as if both represented every supply form. State thickness or diameter, test direction, surface condition, and the governing material specification beside the property.
Verify the ordered alloy, temper, product form, specification revision, heat or lot, and cladding condition before cutting or machining. Recovering identity after irreversible processing is slower and more expensive.
Strength, formability, residual stress, dimensional stability, corrosion response, and post-weld condition change with temper. Never silently replace T3 with T351 or T6 with T651.
Sheet, plate, bar, extrusion, tube, and forging can use different specifications, dimensions, straightening routes, test locations, and mechanical-property limits.
Minimums can change with thickness. L, LT, and ST orientations can matter for strength, fatigue, fracture, forming, stress-corrosion response, and crack growth.
Bare, Alclad, anodized, conversion-coated, primed, sealed, or machined surfaces create different corrosion, bonding, welding, and repair requirements.
2024 chemistry explains the trade-off
Copper is the principal addition, with magnesium and manganese supporting the heat-treatable high-strength response.
6061 chemistry supports a balanced route
Magnesium and silicon form the 6xxx precipitation system, with smaller copper and chromium additions.
Why Does 2024 Need More Corrosion Protection?
The Aluminum Association describes 2xxx alloys as high-strength and tough but less resistant to atmospheric corrosion than many other aluminum families; painting or cladding is common for exposure. In Kaiser's source-specific relative scale, 2024-T4/T351 receives a lower general-corrosion rating than 6061-T6/T651.
- Bare versus protected must be statedA comparison without Alclad, anodize, conversion coating, primer, sealant, paint, or service exposure is incomplete.
- Faying surfaces can govern lifeControl cleanliness, primer and sealant compatibility, fastener stack, water traps, drainage, coating restoration, and inspection access.
- 6061 is not corrosion-proofCrevices, galvanic couples, trapped electrolyte, damaged coating, and poor drainage can still create serious attack.
- Maintenance data has authorityFAA AC 43-4B is guidance; when the manufacturer has a corrosion inspection and treatment program, that applicable program takes precedence.
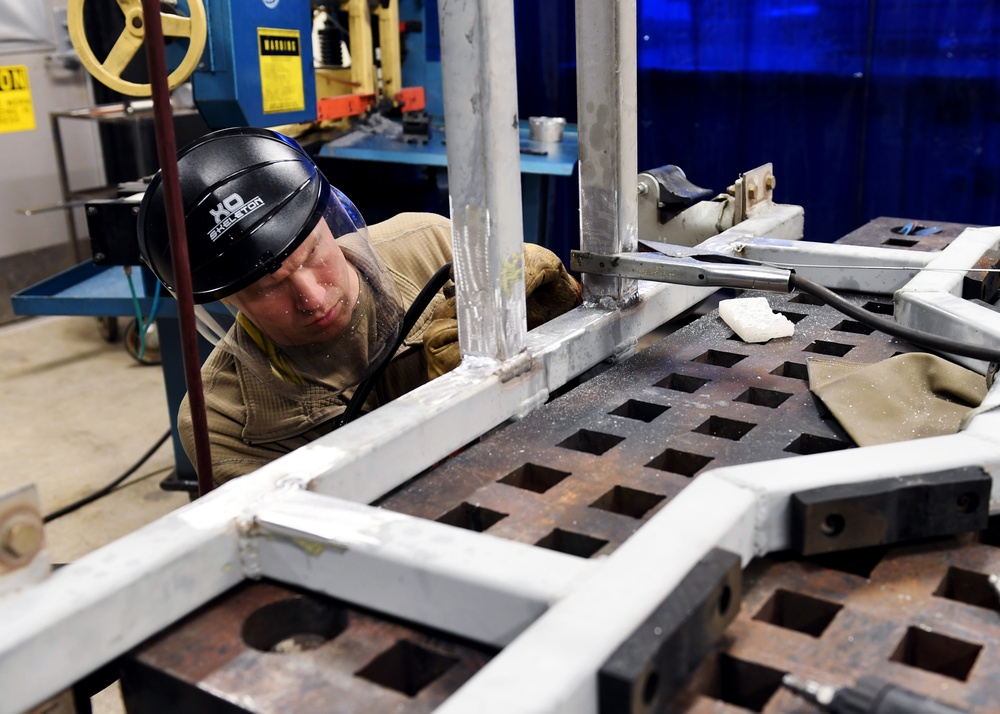
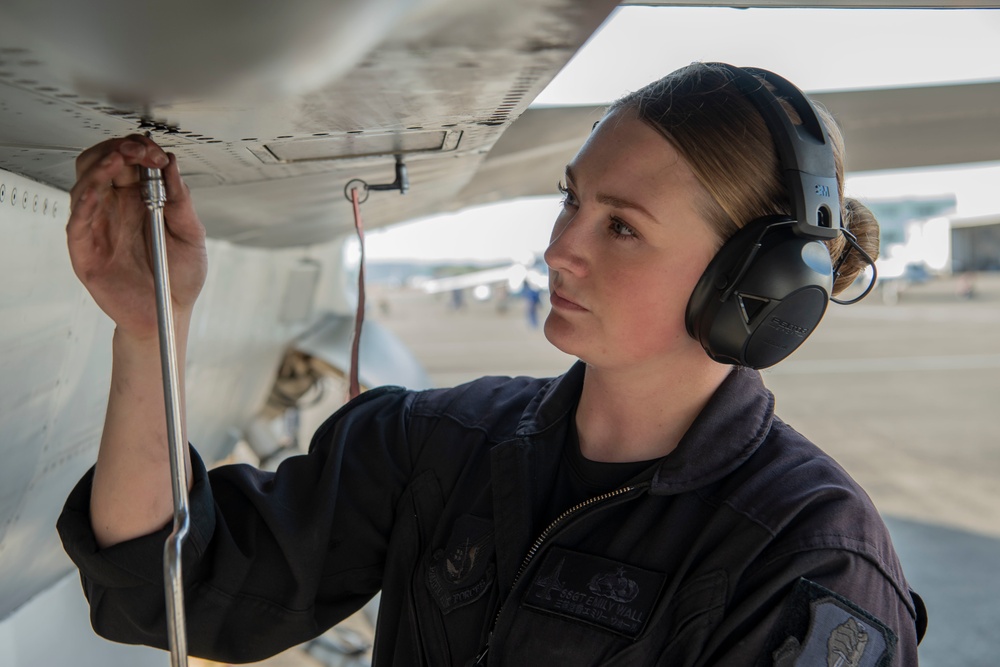
Fastened sheet structures make the hidden interfaces important
Aircraft panels illustrate why alloy selection cannot stop at a tensile table. Holes, fasteners, edge distance, sealant, coating damage, moisture paths, access, and repair procedures influence both structural and corrosion performance.
- For a 2024 pathDefine cladding or coating, faying-surface preparation, sealing, fastener isolation, drainage, and restoration after machining or repair.
- For a 6061 pathKeep the same disciplined interface design; better relative corrosion behavior does not cancel galvanic or crevice risk.
- For either pathUse approved inspection and repair information rather than inferring material identity from appearance.

Which Alloy Is Better for Welding?
6061 is generally the more natural starting point when a production concept requires a fusion-welded aluminum assembly. The producer data rates 6061-T6/T651 as generally weldable by common commercial procedures. That statement is about process suitability, not retained T6 strength.
The thermal cycle changes the precipitate condition near the fusion zone. Local hardness and strength can fall, distortion can shift fit-up, and the weakest region may be the heat-affected zone rather than the visible bead. A qualified procedure must address filler, cleaning, shielding, joint gap, restraint, thickness, heat input, inspection, and the property basis of the finished joint.
Practical, but qualify the as-built joint
Use representative coupons and the real geometry. Confirm fusion, crack and porosity limits, HAZ properties, distortion, corrosion response, and any required NDT or mechanical tests.
Do not assume routine fusion welding is acceptable
Kaiser's ratings describe limited gas weldability and a more restricted arc-welding path because crack sensitivity or loss of corrosion and mechanical performance may matter. Mechanical fastening, bonding, another alloy, or a specialized qualified process may be safer.
Narrow heat input helps control, not eliminate, metallurgy
Laser welding can reduce the heat-affected width and distortion compared with broader heat-input processes, but reflectivity, fit-up, porosity, solidification cracking, filler choice, and local softening still require a process window and evidence.
Which Failure Mode Controls the Material Choice?
The useful question is not "Which alloy has the larger UTS?" It is "Which property, joint, environment, or inspection requirement controls this article in its actual geometry?"
Check bearing, net section, bypass, fastener load transfer, notch sensitivity, temperature, direction, and the approved minimum or allowable basis.
Model section shape, boundary conditions, local instability, tolerance, load introduction, and modulus before crediting a higher-strength alloy.
Include mean stress, holes, fretting, surface condition, corrosion, residual stress, manufacturing marks, inspection interval, and crack-growth behavior.
Specify coating, faying surfaces, sealant, drainage, galvanic isolation, handling, maintenance, and restoration after cutting or repair.
Do not apply base-metal T6 values to the finished 6061 weld or treat a narrow bead as proof of qualified strength and durability.
Fatigue performance must connect to inspection and damage tolerance
A single rotating-beam endurance figure cannot represent a notched aircraft joint under a variable-amplitude spectrum. Crack initiation and growth change with temper, thickness, direction, environment, surface state, fastener holes, fretting, residual stress, and starting flaw.
- Use the applicable fatigue and fracture data for the exact product and orientation.
- Define inspectable locations, method capability, intervals, and allowable damage.
- Evaluate corrosion and fatigue together when surface attack can create crack starters.
- Do not write that 2024 always has better fatigue life than 6061; state the test boundary.
Where Does 2024 Fit, Where Does 6061 Fit, and When Does Neither Fit?
These are screening patterns, not substitution authority. A program specification, drawing, repair manual, or approved material list can narrow the choice before a general comparison begins.
Common examples include qualified aircraft sheet, plate, formed details, fittings, and machined parts where higher strength or fatigue and damage-tolerance performance matter.
Confirm before releaseExact temper, thickness, direction, cladding or coating, joint details, corrosion system, traceability, allowables, and inspection plan.
6061 can be a strong fit for corrosion-tolerant profiles, frames, housings, brackets, fixtures, ground equipment, and permitted flight or space articles.
Confirm before releaseExtrusion or plate specification, temper, wall thickness, joint and HAZ basis, finish, dimensional stability, traceability, and program approval.
A highly loaded structure may require a different 2xxx or 7xxx product. Cryogenic tanks, pressure hardware, castings, additive parts, high-temperature service, or extreme corrosion can need a separate alloy and test program.
Decision ruleDo not force a two-alloy choice when the governing specification or failure mode has already changed the candidate set.


How Should Aerospace Teams Select and Procure the Alloy?
A good material decision survives quotation, receiving, machining, joining, finishing, assembly, inspection, and change control. Write the evidence before the supplier starts work.
Classify the article as flight hardware, repair, space hardware, ground support, tooling, or general industrial work. Identify the design and approval authority.
Capture static, fatigue, accidental, thermal, vibration, fluid, salt, humidity, galvanic, storage, and maintenance conditions.
Choose sheet, plate, bar, extrusion, forging, forming, machining, fastening, bonding, or welding before requesting a quotation.
Use exact temper, product, thickness, direction, cladding, temperature, test method, and applicable allowable or minimum.
Develop corrosion protection, faying surfaces, drainage, coating, fasteners, welding, inspection, and repair as one system.
Specify certificates, heat or lot traceability, special-process records, inspection, NDT, coupons, and change notification.
Confirm final machining, forming, heat input, finish, assembly, geometry, properties, inspection access, and performance.
A supplier cannot quote the intended condition when the order gives only an alloy number.
Paperwork is necessary, but it must connect to the received material and the real acceptance requirement.
Which Comparison Mistakes Create the Most Risk?
Most errors come from dropping the conditions around a property, then treating a convenient number or supplier statement as if it applied to the finished article.
The phrase does not state product form, temper, specification, evidence, process history, or approval route.
State the compared temper, form, thickness, direction, property source, and whether the number is typical, minimum, or allowable.
Producer data helps screening. It cannot replace statistically established design data accepted by the program or authority.
The fusion zone and HAZ need an as-built property and inspection basis tied to the qualified process.
A better statement is that common fusion-welding routes are limited and require application-specific procedure development and qualification.
Bare, Alclad, anodized, primed, sealed, scratched, and repaired surfaces do not share one corrosion outcome.
Supplier similarity is not engineering equivalence for a regulated, qualified, or repair-controlled component.
Frequently Asked Questions About 6061 vs 2024 Aluminum for Aerospace
Is 2024 aluminum stronger than 6061 aluminum?
In the compared producer-typical conditions, yes. Kaiser lists 2024-T4/T351 at 469 MPa ultimate and 324 MPa yield strength, compared with 310 MPa and 276 MPa for 6061-T6/T651. That does not prove 2024 is stronger in every product, thickness, direction, temperature, or failure mode. Use approved values for the exact article.
Is 6061 or 2024 better for aircraft parts?
Neither is universally better. 2024 is often selected for protected, qualified, higher-strength wrought aircraft details. 6061 is often selected when corrosion resistance, extrusion capability, fabrication flexibility, or a weldable route is more important. The drawing, load path, environment, approved data, and manufacturing plan decide.
Can 2024 aluminum be welded for aerospace work?
Do not describe 2024 as impossible to weld, but do not assume a routine fusion weld is acceptable. Public producer ratings describe limited weldability because crack sensitivity or losses in corrosion and mechanical performance can matter. Use a program-qualified joining process and validate the real joint, or select fastening, bonding, or another alloy when appropriate.
Does welding 6061-T6 preserve its T6 strength?
No automatic credit should be taken. Welding changes the precipitate condition in the fusion zone and heat-affected zone, which can reduce local hardness and strength. Design and qualify the finished assembly using the actual process, filler, thickness, geometry, restraint, test data, and acceptance criteria rather than base-metal T6 values alone.
Why is 2024 aluminum often clad or coated?
2024 belongs to the copper-bearing 2xxx family, which has lower atmospheric corrosion resistance than many other aluminum alloys. Cladding, anodizing, conversion coating, primer, paint, sealant, and careful faying-surface design may be used according to the product, environment, drawing, and approved process.
What should appear on an aerospace aluminum RFQ?
State alloy, exact temper, product form, material specification and revision, dimensions and tolerances, cladding or surface condition, orientation when required, certificates, heat or lot traceability, special-process controls, inspection evidence, packaging, change notification, and the approval route for any substitution.
Our team creates practical guides on laser cleaning, welding, marking and industrial automation. We combine application experience with cited engineering sources to help manufacturers compare materials, evaluate processes and plan equipment trials with clearer requirements.
Sources and Technical Review
These sources support comparison, process planning, corrosion context, and regulatory boundaries. Confirm the current revision and applicability before using any value or procedure for a released article.
- Kaiser Aluminum: Alloy 2024 Sheet, Coil & Plate Technical Data - producer-typical properties, chemical limits, and relative corrosion and weldability ratings.
- Kaiser Aluminum: Alloy 6061 Sheet, Coil & Plate Technical Data - producer-typical properties, chemical limits, and relative fabrication ratings.
- The Aluminum Association: Standards and Alloy Series - 2xxx and 6xxx family composition, heat treatment, corrosion, formability, and weldability context.
- The Aluminum Association: Aluminum Standards & Data 2024 - official reference scope for compositions, product standards, mechanical limits, and typical physical properties.
- FAA AC 43-4B: Corrosion Control for Aircraft - current corrosion-control guidance and manufacturer-program precedence.
- 14 CFR 145.109 - repair-station equipment, material, calibration, and current-data requirements.
- FAA AC 25.613-1 - guidance on material strength properties and statistically established design values.
- DLA ASSIST: MMPDS document record - current document status and controlled access route for metallic-material design data.
- U.S. Department of Energy / LANL: 6061 Aluminum Laser-Welding Study - process-specific fusion-zone and HAZ evidence that should not be generalized beyond its test conditions.
Get an Aluminum Welding Recommendation for Your Joint
Send the technical team the alloy and temper, product form, thickness, joint drawing, fit-up range, protection system, required property or defect limits, production target, and the evidence your program needs. That creates a useful sample plan instead of a generic machine recommendation.
- Material: exact alloy, temper, form, specification, surface or cladding condition
- Geometry: thickness, joint type, gap, access, restraint, and critical dimensions
- Acceptance: fusion, cracks, porosity, distortion, HAZ, strength, corrosion, and NDT needs
- Production: takt time, quantity, automation level, traceability, and change-control boundary