

Handheld Laser Welder ROI: Calculate Real Shop Payback
A useful business case measures the complete route from fit-up to finished, accepted part. It does not multiply a sales-video travel speed by annual volume.
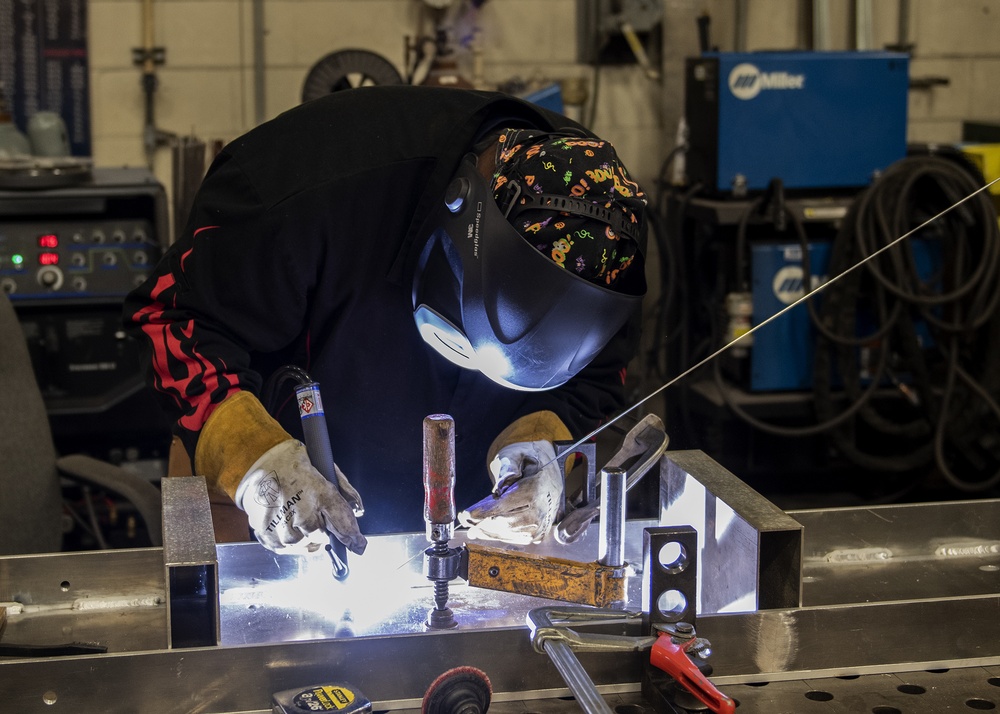
Not one fast weld bead.
When is a handheld laser welder ROI case credible?
Use this decision table before trusting a payback result. Each condition needs a recommendation, evidence and a clear reason to stop or exclude volume.
| Condition | Recommendation | Evidence required | Stop boundary |
|---|---|---|---|
| A recurring job family has high welding, finishing, rework or overtime cost. | Build a separate ROI case for that job family. | Representative parts, full-route baseline time, annual volume and acceptance criteria. | Exclude the family if the proposed process cannot make accepted parts repeatedly. |
| Saved minutes may release the shop bottleneck. | Count only value the business can actually recover. | Overtime records, outside invoices, an avoided-hire plan or supported contribution margin. | Report released hours as capacity—not cash—if no financial path exists. |
| A supplier demonstration shows a fast weld on an ideal coupon. | Use the result only for initial process screening. | Repeated runs with normal fit-up, setup, finishing, inspection and changeovers. | Do not annualize demonstration travel speed or a single best result. |
| The quotation excludes safety, facility or qualification work. | Price the complete production-ready installation. | Hazard review, layout, controls, extraction, power, gas, training and approval plan. | Reject or redesign the project if the safe installed route is not practical. |
| The shop has a mixed, high-mix workload. | Test and model each important job family separately. | Three to eight representative families, including difficult parts and normal operators. | Keep failed or untested families out of qualified annual volume. |
A fabrication shop sells finished parts that pass inspection. That is why the right comparison follows the entire route: preparation, positioning, clamping, tacking, welding, gas and wire changes, cooling or handling, spatter removal, grinding or polishing, straightening, cleaning, inspection, rework and scrap.
Laser welding may reduce several steps at once. It may also add a controlled work area, stricter gap control, fixtures, protective-optics service, qualification work or changeover time. A real business case measures both sides under normal production conditions.
Which job families belong in the ROI model?
Start with parts that create a bottleneck, high finishing time, cosmetic rejects, distortion, overtime, outsourced work or long delivery queues. Then ask whether the exact joint can be welded safely and repeatedly with the proposed configuration. Only the qualified annual volume belongs in the ROI model.
How should you compare the current and laser routes?
- Ignores setup and changeovers
- Ignores grinding and polishing
- Uses one ideal coupon
- Assumes every saved minute becomes cash
- Measures representative job families
- Includes quality and post-weld work
- Uses loaded local labor cost
- Separates cash saving from unused capacity
How do you calculate handheld laser welder ROI and payback?
Simple ROI and payback are useful screening measures. NPV is better when timing, financing, ramp-up or different project lives matter.
How do you calculate the fully installed investment?
Add equipment, installation, controls, extraction, tooling, training, qualification, launch interruption and initial spares.
Investment = all one-time launch costsHow do you calculate annual net benefit?
Add recoverable labor, quality, consumables, avoided outside work and verified contribution. Subtract annual incremental costs.
Net benefit = annual benefits − annual costsHow do you calculate simple ROI?
Use annual net benefit relative to investment for an early comparison. This does not show when cash arrives or the time value of money.
ROI = net benefit ÷ investment × 100%When should you use payback or NPV?
Payback shows months to recover cost. NPV is more useful when cash-flow timing, financing, ramp-up or project life differs.
Payback = investment ÷ net benefit × 12If released hours create new contribution margin, do not also count those same hours as removed labor cost unless a real labor cost is eliminated.
What does your handheld laser welder payback look like?
Replace the example values with measured shop data. This calculator is a first screen, not a supplier quote, accounting opinion, safety approval or weld qualification.
Use the least optimistic defensible number where evidence is incomplete.
The screening case is positive. Validate each benefit by job family and run a safety-gated production pilot before approval.
Where does handheld laser welding actually save time and cost?
A laser process may create value by reducing heat distortion, finishing or rework—not only by moving the torch faster.
- Time the same start and finish point for both routes.
- Include setup, fixture, wire/gas, optics and inspection tasks.
- Use several normal production runs, not one polished sample.
- Keep quality acceptance identical.
Operator minutes directly used by the job, including normal rework.
Queues, waiting and bottlenecks that affect delivery but may not be labor.
What belongs in the fully installed cost?
Compare a production-ready laser system with the current production route. Comparing a bare laser source with a complete TIG station creates a false payback.
Define the exact configuration needed by the qualified job mix.
- Laser source, fiber and hand torch
- Cooling and electrical supply
- Wire feeder and gas hardware
- Optics, nozzles, carts and spares
Budget the installation that can be operated responsibly in the intended shop.
- Hazard assessment and controlled area
- Access, interlocks and beam termination
- Warning systems, PPE and oversight
- Extraction, fire and environmental controls
Include the work between delivery and accepted production.
- Fixtures and part preparation
- Training and supervised practice
- Procedure development and testing
- Launch scrap and production interruption
Availability matters as much as energy cost.
- Service and breakdown repair
- Protective optics and nozzles
- Cooling-water treatment or filters
- Software, support and verification
Model the cost of a machine that cannot run when the bottleneck needs it.
- Response time and warranty boundary
- Spare-part lead time
- Backup production route
- Training refresh and operator coverage
Match financing treatment to the decision method.
- Interest or lease cost
- Ramp-up and working capital
- Approved hurdle or discount rate
- Residual value only with evidence
Which safety costs must be included before approval?
FDA identifies Class 4 lasers as immediate eye and skin hazards from direct or reflected beams and as potential fire hazards. OSHA describes controlled areas, beam termination, trained authorized people, appropriate eyewear and ventilation for laser-generated fumes.
The exact controls depend on the product, wavelength, beam path, workpieces, layout and jurisdiction. ISO 11553-1 covers laser-processing-machine hazards, while the current ISO 11553-2:2026 edition addresses safety requirements for hand-held or hand-operated laser processing machines.
Read the laser eyewear guide →Assess direct and reflected paths, nominal hazard zone, specular surfaces, service access and abnormal conditions.
Design the area, entry system, warning, interlock strategy and beam stop with competent safety professionals.
Document operating, maintenance, emergency, visitor and change-control procedures. Training is not a one-time demo.
Review the metal, oil, coating and consumables. Provide suitable local extraction, filtration and fire controls.
Check key control, emergency stop, external interlock connection and other required features against manuals and standards.
Operator laser authorization and weld-process acceptance are different gates. A good-looking coupon proves neither.
If the safe installed route is not practical, change the layout, compare an enclosed solution or reject the project.
Which fabrication jobs are better ROI candidates?
These are screening clues, not process approvals. The exact material, joint, quality requirement and installation must still be tested.
Which jobs are strong starting candidates?
Look for a costly, repeatable problem that a qualified laser route can remove.
Which jobs need more caution or another process?
Add the extra preparation, fixture and approval burden—or keep another process.
How do cooling and wire feed change the business case?
A cheaper configuration can cost more if it cannot sustain the work mix. A more complex configuration can also weaken ROI when its capability is rarely used.
Air-Cooled vs Water-Cooled Handheld Laser Welders
Can simplify mobility and infrastructure for suitable intermittent or lower-duty work. Verify actual duty, ambient limits and service plan.
May suit a different thermal and production duty, but add chiller maintenance, water quality, floor space and facility needs.
Wire Feed vs No Wire Feed
Can keep the process simpler when fit-up and joint requirements allow autogenous welding.
Can help when approved filler is needed for gap, chemistry or reinforcement, but adds setup, consumables and control variables.
Handheld vs Enclosed or Automated Laser Welding
Mobility is valuable only when a safe controlled area and repeatable manual process are practical. Compare a cell when risk, repeatability or volume demands it.
How should a fabrication shop validate the ROI?
Select three to eight representative job families. Keep unfavorable results; they define the real eligible volume.
Material, thickness, joint, gap, access, filler, finish, annual volume and acceptance criteria.
Time the current full route and capture rework, scrap, consumables, overtime and outside work.
Approve the trial area, controls, procedures, extraction, training and authorized roles before emission.
Use representative operators, parts, fit-up, changeovers, cleaning and expected interruption—not only ideal coupons.
Apply the needed visual, dimensional, destructive, mechanical, leak, corrosion or customer tests.
Calculate each family separately. Exclude failures and apply conservative uptime and recoverability.
If every result is forced into the annual ROI model, the exercise is marketing—not investment control.
How does the illustrative 14.4-month payback work?
This is the same editable example loaded in the calculator. It is not a quote, benchmark, promise or claim about a specific Oceanplayer Laser model.
The example assumes 8,000 qualified parts per year, 9 whole-cycle minutes saved per part, 60% recoverability and a fully loaded labor cost of $48 per hour.
| Illustrative line item | Calculation basis | Annual value |
|---|---|---|
| Recoverable labor benefit | 8,000 × 9 min ÷ 60 × 60% × $48/h | $34,560 |
| Quality, rework and scrap benefit | Measured annual reduction after validation | $9,600 |
| Incremental contribution | Supported demand after variable costs | $12,000 |
| Incremental consumables and ownership | Optics, nozzles, gas/wire, service and spares | -$6,000 |
| Annual net benefit | Annual benefits minus annual incremental cost | $50,160 |
| Initial installed investment | System, safety, extraction, tooling, qualification and launch | $60,000 |
| Simple ROI / payback | $50,160 ÷ $60,000; $60,000 ÷ $50,160 × 12 | 83.6% / 14.4 months |
Which assumptions can break the payback?
Run conservative, base and upside cases. The project should not depend on every uncertain input reaching its best value.
Use recurring, qualified work. Do not include every welded part in the shop or uncommitted “possible” business.
Test: -20% and delayed rampUse repeat runs with normal setup, changeover and inspection. Do not use one best cycle.
Test: lower quartile resultAsk which overtime, subcontract invoice, hire or booked constraint will actually change.
Test: 25%, 50%, 75%Lower uptime reduces eligible volume and can create backup-process cost at the same time.
Test: downtime + spare delayUse accepted parts, not attractive top beads. Include finishing, rework and scrap that remain.
Test: no quality benefitAdd facility work, controls, training and approval before comparing suppliers.
Test: +15% launch costUse verified margin after variable cost, not gross revenue or theoretical capacity.
Test: no new demandFor longer comparisons, include discount rate, recurring costs, ramp and residual-value evidence.
Use NPV for final capexWhy do handheld laser welder ROI models fail?
A model can be mathematically correct and still be commercially useless when its inputs describe a demo instead of the production system.
Whole-cycle setup, fit-up, finishing, inspection and rework disappear from the model.
Redeployed minutes may remove no cost and create no additional margin.
The installed cost becomes artificially low and the launch date unrealistic.
Gap, access, material, filler and customer acceptance vary by job family.
The same released hour appears under labor, finishing, capacity and margin.
Revenue ignores material, commission, freight and other variable costs.
Utilization, downtime and quality drift can erase the forecast after launch.
What evidence should you send suppliers?
A useful request lets machine, safety, tooling and process assumptions be compared on the same boundary.
0 of 7 input groups confirmedThese checks are local to your browser and are not submitted.
Submit the ApplicationFrequently Asked Questions About Handheld Laser Welder ROI
These questions cover practical gaps that remain after the main calculation. Final decisions still need the actual machine, application, safety review and qualification evidence.
There is no universal payback period. It depends on qualified workload, complete-route minutes saved, labor recoverability, quality, utilization, installed safety cost, service and demand. A controlled pilot and conservative model are more useful than an average supplier claim.
Not across an entire shop. It may replace or complement current processes for qualified job families. Variable gaps, difficult access, thick joints, coatings, code requirements or low volume may keep TIG, MIG or another method as the better route.
Calculate ROI from the annual volume of the job families that pass the required quality and safety gates. Keep TIG, MIG or another process for the remaining work. Do not add failed or untested parts to the laser volume just to improve payback.
Use simple payback for an early screen because it is easy to understand. Use net present value for the final decision when cash-flow timing, financing, ramp-up, project life or the shop's discount rate could change which option creates more value.
Use these related guides to refine machine, process, configuration and operating-cost questions before requesting a trial.
Review the system category, applications and configuration path.
Open machine page → Budget planningHandheld Laser Welder CostUnderstand acquisition and installed-cost drivers before supplier comparison.
Read cost guide → Process learningLaser Welding GuideBuild a stronger technical baseline for material, joint and process discussions.
Read the guide → Industry applicationSheet Metal FabricationConnect the welding decision with the wider fabrication workflow.
Explore the industry → ConfigurationAir-Cooled vs Water-CooledCompare duty, infrastructure, mobility and ownership tradeoffs.
Compare cooling → Joint capabilityWire Feed vs No Wire FeedDecide when filler capability supports the job mix.
Compare wire feed → Operating cost toolShielding Gas Cost CalculatorEstimate one variable-cost line with your own flow and schedule.
Open calculator → Application reviewSend Parts for EvaluationShare part, joint, baseline and facility details for a safety-inclusive discussion.
Contact Oceanplayer Laser →Sources and Engineering Boundaries
- NIST — A Guide to the Smart Investment Tools. Manufacturing investment analysis, payback, NPV and sensitivity methods.
- U.S. Bureau of Labor Statistics — Employer Costs for Employee Compensation. Defines compensation as wages/salaries plus employer benefit costs; use the shop's own loaded rate.
- FDA — Frequently Asked Questions About Lasers. Laser classifications and Class 4 direct, reflected, skin and fire hazard context.
- OSHA Technical Manual — Laser Hazards. Controlled areas, training, beam termination, eyewear, ventilation and other controls.
- ISO 11553-1:2020 — Safety of machinery: Laser processing machines. Laser-processing-machine hazard and manufacturer-information scope.
- ISO 11553-2:2026 — Safety requirements for hand-held or hand-operated laser processing machines. Current second edition for the hand-held machine category; apply it with the exact equipment, site rules and competent review.
- American Welding Society — Handheld Laser Welding Safety. Qualified-person and equipment safety-feature guidance.
Send representative parts, material and thickness, joint and gap, current routing and finishing minutes, annual volume, acceptance criteria, facility context and cost assumptions. Oceanplayer Laser can help organize a safety-inclusive sample and configuration discussion.