
7 Medium Carbon Steel Grades: Uses and How to Choose
For general shafts and pins, 1045 is a useful starting point. Consider 1050 or 1055 when greater hardness potential matters, and 4140 or 4340 when deeper hardening and core properties become important. Choose the grade and heat-treatment condition together. Carbon content alone does not tell you how a finished part will perform.
What is medium carbon steel?
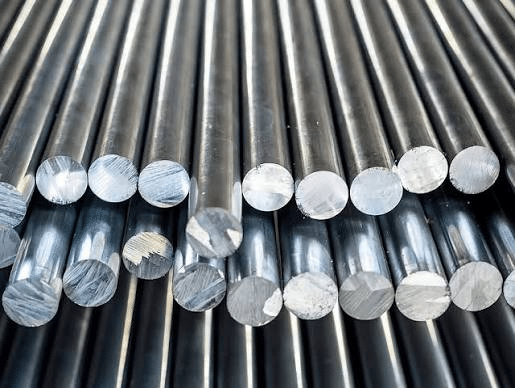
Medium carbon steel commonly refers to steel containing roughly 0.30–0.60% carbon by mass. The boundaries vary between references. Compared with low-carbon steel, it offers greater hardening potential, but usually needs more care during welding, cold forming, and quenching.
There are two groups in this comparison. 1040, 1045, 1050, 1055, and EN8/080M40 are plain or unalloyed carbon-steel options. The 4140 and 4340 grades are low-alloy steels within the medium-carbon range. Their chromium, molybdenum, and, in 4340, nickel change how the steel responds to cooling.
The grade identifies a chemistry—not a fixed strength. A soft starting bar, a quenched-and-tempered shaft, and an induction-hardened journal can share a grade name while having different properties.
Two terms worth separating: hardness is resistance to local indentation. Hardenability is the ability to develop a hardened structure below the surface during a given cooling cycle. A steel can reach high surface hardness yet have limited hardening depth.
How do the seven medium carbon steel grades compare?
Use this table to build a shortlist, not to release a material specification. The carbon values are rounded nominal levels for orientation; the ordered standard and heat analysis control the actual limits.
| Grade | Carbon basis | Common applications | Reason to consider it | Main check |
|---|---|---|---|---|
| 1040 | About 0.40% | Couplings, bolts, forged levers, moderate-duty shafts | General mechanical parts without a high surface-hardness target | Core properties in the actual section |
| 1045 | About 0.45% | Pins, axles, shafts, gears, wear journals | Versatile bar grade with useful local hardening response | Surface hardness versus hardened depth and core strength |
| 1050 | About 0.50% | Wear parts, axles, blades, selected spring parts | Higher attainable hardness than lower-carbon plain grades | Cracking, distortion, and forming requirements |
| 1055 | About 0.55% | Springs, hand tools, blades, wear edges | Hardness and wear resistance after suitable treatment | Toughness at the specified final hardness |
| EN8 / 080M40 | About 0.40% | Shafts, studs, rollers, connecting rods | Established British general-engineering supply route | Exact designation, product standard, and condition |
| 4140 | About 0.40%; Cr-Mo alloy | Loaded shafts, gears, fasteners, tooling | Greater hardening depth than plain-carbon options | Size-specific quenched-and-tempered properties |
| 4340 | About 0.40%; Ni-Cr-Mo alloy | Severe-duty shafts, axles, gears, high-strength components | High hardenability and demanding strength-toughness combinations | Required heat quality, treatment, and inspection |
On narrow screens, scroll within the table. Plain-grade chemistry reference: Summit Steel’s carbon-steel ranges. The grade discussions below identify additional product sources and limits.
What is each grade best suited for?
1040: general forgings and moderate-duty parts
Consider 1040 for couplings, bolts, levers, and shafts that need more hardening response than low-carbon steel but do not need the highest hardness in this group. It is a plain-carbon starting point rather than a deep-hardening alloy.
Its lower carbon level can leave more processing flexibility than 1050 or 1055, although the delivered condition still matters. If the part has a thick load-carrying center, verify that center instead of relying on a hard surface reading.
1045: shafts, pins, and locally hardened wear surfaces
1045 is a practical benchmark for many machined components. It can be supplied in different bar conditions and used for parts that combine moderate core loads with wear at a journal, tooth, or contact surface.
Atlas Steels identifies 1045 as suitable for flame and induction hardening. These processes can harden selected regions without treating the whole section in the same way. Specify both the hardened depth and the underlying core requirement. For the individual grade, see 1045 properties, uses, and machinability.
1050: a higher-hardness plain-carbon option
1050 is worth comparing when a 1045 design needs more attainable hardness, particularly for wear-oriented components, axles, or selected blade and spring applications. The small increase in nominal carbon is a change in hardening potential—not an automatic increase in usable load capacity.
Check the final temper, thickness, and edges. A part that gains hardness but cracks during quenching or loses too much toughness has not improved. If the core is the problem, compare an alloy grade rather than increasing carbon alone.
1055: springs, tools, and wear edges
1055 sits near the upper end of the usual medium-carbon range. It is a candidate for hardened edges, selected hand tools, and spring parts where hardness must be balanced with resistance to fracture.
Do not read “spring steel” as “more flexible.” Heat treatment helps a spring resist permanent set; its geometry is still central to how far it deflects. Control the final hardness, surface carbon loss during heating, and edge defects. Welding should be treated as a separate engineering problem.
EN8 / 080M40: general engineering with a British designation
EN8 is a legacy trade name commonly associated with 080M40. It remains familiar for shafts, studs, bolts, rollers, and connecting rods. West Yorkshire Steel lists 080M40 at 0.36–0.44% carbon and offers it in several product and delivery conditions.
That does not make it identical to 1045. Confirm what the drawing means by EN8 and what the supplier is actually certifying. The supplier’s 080M40 data is a useful reference, not blanket approval for substitution.
4140: parts that need deeper hardening
4140 adds chromium and molybdenum. Consider it when a plain-carbon grade cannot reliably develop the required properties through the controlling section. Typical candidates include loaded shafts, gears, fasteners, and tooling.
“Prehardened 4140” is still an incomplete requirement: ask for the hardness range, section, and mechanical-property evidence. Related European grades also need specification review. The 4140 grade guide covers its processing options in more detail.
4340: demanding strength and toughness in heavier sections
4340 adds nickel to the chromium-molybdenum alloy system. It is considered for high-stress shafts, axles, gears, and other components that need high hardenability and a carefully balanced quenched-and-tempered condition. Atlas Steels’ 4340 bar data illustrates these uses and the role of section size.
Choose it because a defined requirement justifies it—not because its grade number is larger. Material quality, surface finish, heat treatment, and crack inspection remain important. An application that depends on fatigue or fracture resistance needs evidence for those requirements, not just a tensile-strength figure.
Application examples describe candidate uses, not approved designs. AMS Resources lists shafts, machinery parts, bolts, pinions, and gears among applications for the plain-carbon group.
Why do strength values change with heat treatment and diameter?
The center of a thick section cools differently from its surface. A heat treatment that produces the required structure in a small bar may not produce the same result through a larger one. Tempering then changes the balance of strength and toughness.
This is why the same grade name can appear beside several valid strength ranges. The important comparison is grade + delivery condition + product form + size + test requirement.
Example: reading a supplier’s size-dependent data
Ovako’s published data for 42CrMo4 M, variant 6082, quenched-and-tempered round bar gives different ranges by size. The following diameters fall within three of its listed bands:
| Bar diameter | Minimum yield strength | Tensile strength range |
|---|---|---|
| 30 mm | 750 MPa | 1,000–1,200 MPa |
| 80 mm | 650 MPa | 900–1,100 MPa |
| 120 mm | 550 MPa | 800–950 MPa |
Reading lesson: the 30 mm entry does not establish the requirement for a 120 mm bar. These are the named producer variant’s data, not universal 4140 values or an Oceanplayer Laser test. Source: Ovako, mechanical-properties table.
Yield strength indicates the onset of permanent deformation. Tensile strength is the maximum engineering stress in the tensile test. Neither alone proves impact toughness, fatigue life, or resistance to wear. Request the property that addresses the part’s failure mode.


How does hardenability affect a thick shaft or gear?
Hardenability describes how deeply the steel can develop a hardened structure under stated cooling conditions. Carbon affects attainable martensitic hardness; alloying and the cooling path strongly influence how far that response extends.
The Jominy end-quench test cools one end of a heated specimen and measures hardness at increasing distances from that end. The resulting curve compares response at different cooling rates. It is not a direct drawing of the hardened layer in your finished shaft.
A hard journal over a softer core may be exactly what a wear application needs. If the center must carry a high load, the same result may be unacceptable. Specify which region matters. See the Jominy test explanation in the TLP teaching library.
Which heat-treatment route fits the part?
Choose the desired property distribution before choosing the heating cycle. There is no single temperature, holding time, or quenching-medium rule that suits all seven grades and all geometries.
Quench and temper for load-carrying properties
Quenching forms a hard structure where cooling is fast enough. Tempering reduces brittleness and adjusts the strength-toughness balance. This route is useful when the specified section needs controlled mechanical properties.
Check the controlling thickness, quench response, distortion allowance, and test location. Through-hardening capability is not unlimited, even with an alloy steel.
Surface hardening for localized wear
Induction or flame hardening can treat a journal, tooth, or contact surface while leaving the core in a different condition. The aim is a defined hardened layer, not the largest possible surface hardness.
Specify surface hardness, effective hardened depth, core requirements, grinding allowance, and crack checks. One surface reading cannot prove the full profile.
Plan machining around treatment. Normalizing or annealing may provide a useful starting condition. Rough machining, final heat treatment, and finish grinding should be sequenced with expected movement in mind. Your heat treater needs the geometry and target properties, not only the grade name.
How should you shortlist a grade for your application?
Use the failure mode to decide what to verify first. These are conditional selection examples, not reports of completed customer tests.
- A journal wears while the shaft remains mechanically sound: compare a qualified surface-hardening route for 1045 or 1050. Check hardened depth and finish before paying for a higher-alloy core.
- A larger shaft misses its core-property requirement: compare 4140, then a higher-hardenability option such as 4340 if needed. Confirm that the heat treatment and section—not an unrelated surface problem—are the limit.
- A hardened blade or spring breaks: review temper, surface damage, carbon loss, and loading. Moving from 1050 to 1055 simply to raise hardness may worsen the wrong problem.
- A component must be welded as part of normal fabrication: review the steel and joining route together. The easiest grade to harden may not be the easiest grade to weld.
For purchase comparisons, include processing and rejection risk in the cost. A lower-priced bar is not economical if it needs extra machining, distorts beyond tolerance, or fails the required inspection.
What changes when you machine, form, or weld these steels?
Machining depends on the delivered condition
Compare actual hardness and microstructure, not a single machinability percentage from a general chart. A soft 4140 bar and a hardened 4140 bar are different cutting jobs. Cold-worked or prehardened stock can also move as machining releases residual stress.
For a long shaft or a tight bore, agree the starting condition, stock-removal sequence, and finish allowance before ordering. Use cutting-tool data for the actual material condition and operation.
Forming needs suitable stock and edge quality
Higher strength and harder conditions generally leave less cold-forming margin. Tight bends, sheared edges, and holes can concentrate strain. Choose the forming condition and process before hardening rather than assuming every grade can be bent after treatment.
Welding needs control of the heat-affected zone
These steels can form a hard, crack-sensitive heat-affected zone (HAZ) beside a weld. Actual chemistry, hydrogen, restraint, section thickness, and cooling conditions all matter. Carbon equivalent is a useful screening quantity, not a complete procedure.
TWI’s guidance for carbon-manganese steels explains the need for composition knowledge, hydrogen control, and qualified welding conditions. Alloy grades need their own procedure review; do not copy a generic preheat temperature across the list.
Laser welding does not remove this metallurgy. A narrow heat-affected zone can still contain hard or softened regions. Qualify the real joint for cracking, hardness changes, fusion, and the mechanical performance the part requires. A neat bead is not sufficient evidence.
Are EN8, 1045, C45, and other “equivalents” interchangeable?
No automatic substitution should be assumed. Similar applications or overlapping carbon ranges do not make two standards identical. EN8/080M40 is often compared with 1040 or 1045, while C45 is often compared with 1045. Review the intended specification rather than translating the trade name alone.
The same rule applies to 4140 and 42CrMo4. A supplier may offer a variant that meets a particular SAE requirement, but that does not make every product under the broader European name interchangeable.
- Compare the full chemistry: carbon, alloying elements, and controlled residuals—not only the grade’s final two digits.
- Match the product and condition: bar, forging, or plate; annealed, normalized, as-rolled, or quenched and tempered.
- Match the acceptance evidence: size range, sampling location, tensile properties, hardness, impact requirements, and any hardenability requirement.
- Keep traceability: link the heat certificate to the supplied stock and preserve identification after cutting.
For a critical substitution, obtain engineering approval against the drawing and service conditions. A comparison chart is a starting point for that review, not its conclusion.
Sources and material-data references
- Summit Steel: carbon-steel chemical ranges — reference ranges for the plain SAE carbon grades; actual orders require the governing specification.
- AMS Resources: 1040, 1045, and 1050 medium-carbon steels — common machinery applications and supplied product forms.
- West Yorkshire Steel: 080M40 — chemistry, supply conditions, applications, and treatment considerations.
- Ovako Steel Navigator: 42CrMo4 — named variants and size-dependent mechanical-property data; revised February 3, 2026.
- Atlas Steels: through-hardening low-alloy steel bar 4340 — historical producer data, revised April 2006. Used for metallurgy and application context, not current stock or pricing.
- TLP Library: hardenability and Jominy testing — explanations of hardness versus hardening depth and the end-quench test.
- TWI: avoiding hydrogen cracking in C-Mn steels — welding conditions and the need to assess the heat-affected zone.
Published grade data does not replace the agreed material specification or the certificate for your supplied product. Do not combine values from different conditions into one assumed property set.