

How to Remove Mill Scale from Steel: Best Methods Compared
For small weld zones, compare grinding or stripping abrasives. For broad coating-prep areas, compare blasting; for compatible batches, consider controlled pickling. Laser cleaning may suit selective paths if samples confirm scale removal without unacceptable steel change. The best choice meets the next welding or coating requirement.


Quick Answer: What Is the Best Way to Remove Mill Scale from Steel?
Choose the process by matching four things: how firmly the scale is attached, the part's size and access, how much change to the underlying steel is acceptable, and the condition required after cleaning. For an occasional weld repair, a well-controlled abrasive tool may be simpler than setting up a batch process. For a run of large frames headed to protective coating, blasting may remove the scale while producing the specified texture. If the work consists of many similar parts that can be immersed and fully rinsed, pickling may be worth evaluating. If only a narrow path needs treatment or the motion can be repeated consistently, a laser trial may be useful.
Which Methods Work Best for Large Areas, Small Parts, and Localized Cleaning?
Large, open faces are usually where a blast process deserves an early comparison. It reaches broad surfaces and can create a coating profile, although recesses and thin features still need attention. A grinder or flap disc can be more practical around a few joint faces or edges, where the operator can see and control the removal. Pickling is a production process rather than a hand-tool substitute: the part must fit a qualified treatment, rinse, and drying route. Laser cleaning is worth considering when the removal area is selective, access is designed into the cell, or repeatability is important. None of these descriptions is a speed guarantee.
Quick Comparison: Grinding vs. Blasting vs. Pickling vs. Laser Cleaning
| Method | Good starting situation | Main question before choosing it |
|---|---|---|
| Grinding or stripping abrasive | A few accessible weld zones or local repairs | Can the oxide be removed without changing thickness, edge shape, or fit-up? |
| Abrasive or shot blasting | Broad steelwork, especially when a coating profile is specified | Can all required faces be reached, and will the specified cleanliness and profile be achieved? |
| Industrial pickling | Compatible batches or continuous steel-processing lines | Can chemistry, rinsing, drying, and waste be controlled for this grade and geometry? |
| Laser cleaning | Selective or repeat paths with a qualified process | Does it remove this scale while leaving an acceptable substrate and finish? |
Ordinary wire brushing belongs in the evaluation too, but it is often a cleanup step for loose material rather than a reliable answer for firmly attached scale. The rest of this guide explains why these methods behave differently and how to test the result.
What Is Mill Scale, and Why Should It Be Removed?
Mill scale is the oxide layer that develops on steel during hot processing. It often appears as a dark gray or blue-black skin on hot-rolled plate, sections, or tube. Storage rust is a later corrosion product; both can occur on one part. That distinction matters because a process that removes loose orange rust may leave tightly bonded dark scale behind. Before descaling, identify the layer: dark paint, galvanizing, or another specified surface treatment should not be removed because it merely resembles scale.
How Mill Scale Forms on Hot-Rolled Steel
Hot steel reacts with oxygen during heating and rolling, forming iron oxides at the surface. Cooling and later handling can leave some areas tightly attached and others cracked or flaking. This uneven attachment is why a sample with light, loose scale can clean quickly while another piece from the same stock form resists the same process. The operator needs to inspect both the easy flat face and the difficult corners, edges, and pits.
The oxide is a separate surface layer, not the sound steel beneath it. Removing it may expose bare steel, but the route used can also change the substrate: a disc may cut metal, blasting can create a profile, chemistry may attack the surface if uncontrolled, and laser exposure may alter it thermally. “Scale removed” and “steel ready for the next operation” are therefore separate findings.

When Mill Scale Must Be Removed—and When It Can Remain
Remove scale where the welding procedure, coating system, bonding process, or inspection requirement calls for a clean prepared substrate. Protective coatings on structural steel commonly rely on removal of residual mill scale and on a suitable surface profile; Steel Construction Info's preparation guidance explains those two functions of blast cleaning. For welding, the specified joint and nearby surfaces need preparation compatible with the process and materials, rather than a blanket assumption that every square centimeter of a large assembly needs identical treatment. TWI's joining guidance connects surface cleaning with joint geometry and the qualified welding procedure.
Scale can remain on an as-received surface when the design and next operation genuinely permit it—for example, on a portion that is neither joined nor coated and for which its condition is acceptable. That is a specification decision, not a universal exemption. If a later coating or weld will be added, plan the access and preparation now instead of discovering an unreachable scaled face after assembly.
How Do the Main Mill Scale Removal Methods Compare?
The quick table identifies candidates; a final choice requires a fair comparison on the same steel and acceptance target. A clean-looking patch may still fail because it is too smooth for the coating, because abrasive contact changed a weld edge, or because oxide remains in a recess. Decide what must be preserved as well as what must be removed.
Compare Removal Effectiveness, Surface Finish, Speed, and Cost
Removal effectiveness is the fraction of the required area that reaches the defined endpoint after all passes and touch-up—not the brightness of one easy patch. Surface finish means the condition left behind: texture, edge shape, contamination, and any heat or chemical effect. Speed should be measured over the whole accepted job, including handling and inspection. Cost should be assigned to accepted parts or accepted prepared area, not to a machine's advertised pass rate.
These criteria can point in different directions. Blasting can both remove adherent scale and create texture, but it needs media, containment, and access. Grinding is portable but exposes the steel to operator-dependent cutting. Pickling can treat many suitable pieces together but adds solution management and post-treatment. Laser cleaning uses no abrasive contact, yet it still needs beam control, extraction, and a scale-specific process window; a separate profiling operation may remain necessary. Use the same downstream acceptance rule for every candidate so the comparison does not reward one method for doing less work.
How Steel Thickness, Part Geometry, and Production Volume Affect Method Selection
A heavy flat plate and a thin, formed part can tolerate different mechanical actions. Aggressive abrasion on a thin edge can change its dimensions; a fixture or controlled tool path may be needed. Deep slots and back faces can escape a blast stream or a laser scan, while acid can enter crevices that are difficult to rinse and dry. A large immersion bath makes little sense for one local repair; hand grinding may become inconsistent across thousands of identical parts.
Volume changes which setup costs can be spread over accepted output. A repeatable, enclosed process may justify fixture and automation work when the same part is cleaned many times. For one-off maintenance, a qualified portable process or buying suitably descaled stock may be more practical. These are process-selection deductions; neither a particular cost nor throughput follows without an actual production trial.
How Can You Remove Mill Scale Mechanically?
Mechanical methods dislodge or cut away oxide by contact or abrasive impact. Their strength is direct action on attached scale; their principal limit is that the same action can also change the steel. The tool, abrasive, angle, pressure, dwell, and geometry all affect the result. A sample should include edges and hard-to-reach features, not just the center of a flat plate.
Grinding and Flap Discs: Effective Local Removal and the Risk of Metal Loss
A grinding wheel cuts through scale and can cut into the steel beneath it. A flap disc or suitable stripping abrasive can blend the transition and may give the operator finer control, but it is still a material-removal tool. It fits a few accessible weld strips, bevels, and repair zones when the area is small enough to inspect closely.
Mark the required cleaning zone first. Then inspect the joint face, edge radius, remaining thickness, and fit-up as well as the absence of dark oxide. If repeated passes are needed to chase isolated islands, compare another abrasive or method before enlarging the ground area. The correct wheel, guard, speed rating, and working face must be used under the tool instructions; a cutting disc is not a substitute for a grinding disc.
Wire Brushing: Why Surface Brightness Does Not Guarantee Complete Removal
A wire brush is useful for loose flakes and debris. Its bristles can pass over firmly attached scale without breaking it free, and repeated brushing can polish or burnish the surrounding surface. A brighter color therefore does not establish descaling. Purpose-designed abrasive brushes or other powered descaling tools are separate choices and should be tested for the actual steel and finish.
Look for dark islands after brushing, especially beside welds and at surface depressions. If they remain, confirm whether they are attached oxide rather than discoloration; then change the removal mechanism instead of assuming more brushing will eventually work. For painting, also check whether the resulting texture matches the coating requirement rather than merely looking smooth and clean.
Abrasive and Shot Blasting: Removing Scale While Creating a Surface Profile
Abrasive particles strike the surface and fracture or dislodge the oxide. The impacts can also roughen the exposed steel, which is useful when a protective coating specifies an anchor profile. Air blasting can reach varied structures with an appropriate nozzle path; wheel-shot equipment can suit repeated parts that fit its handling and exposure pattern. Neither method automatically reaches hidden faces or leaves every edge at the correct condition.
Select the abrasive and process around both the required visual preparation and the coating's texture range. Inspect recesses, backs, sharp edges, and thin sections; record contamination and media condition. A specified blast grade is not interchangeable with a hand-tool grade simply because both reveal steel. ISO 8501-1:2007 addresses visual rust and preparation grades, while ISO 8503-1:2012 concerns comparators for blast-cleaned surface profile. Neither alone proves the whole coating system will perform.
When Should You Use Chemical Pickling to Remove Mill Scale?
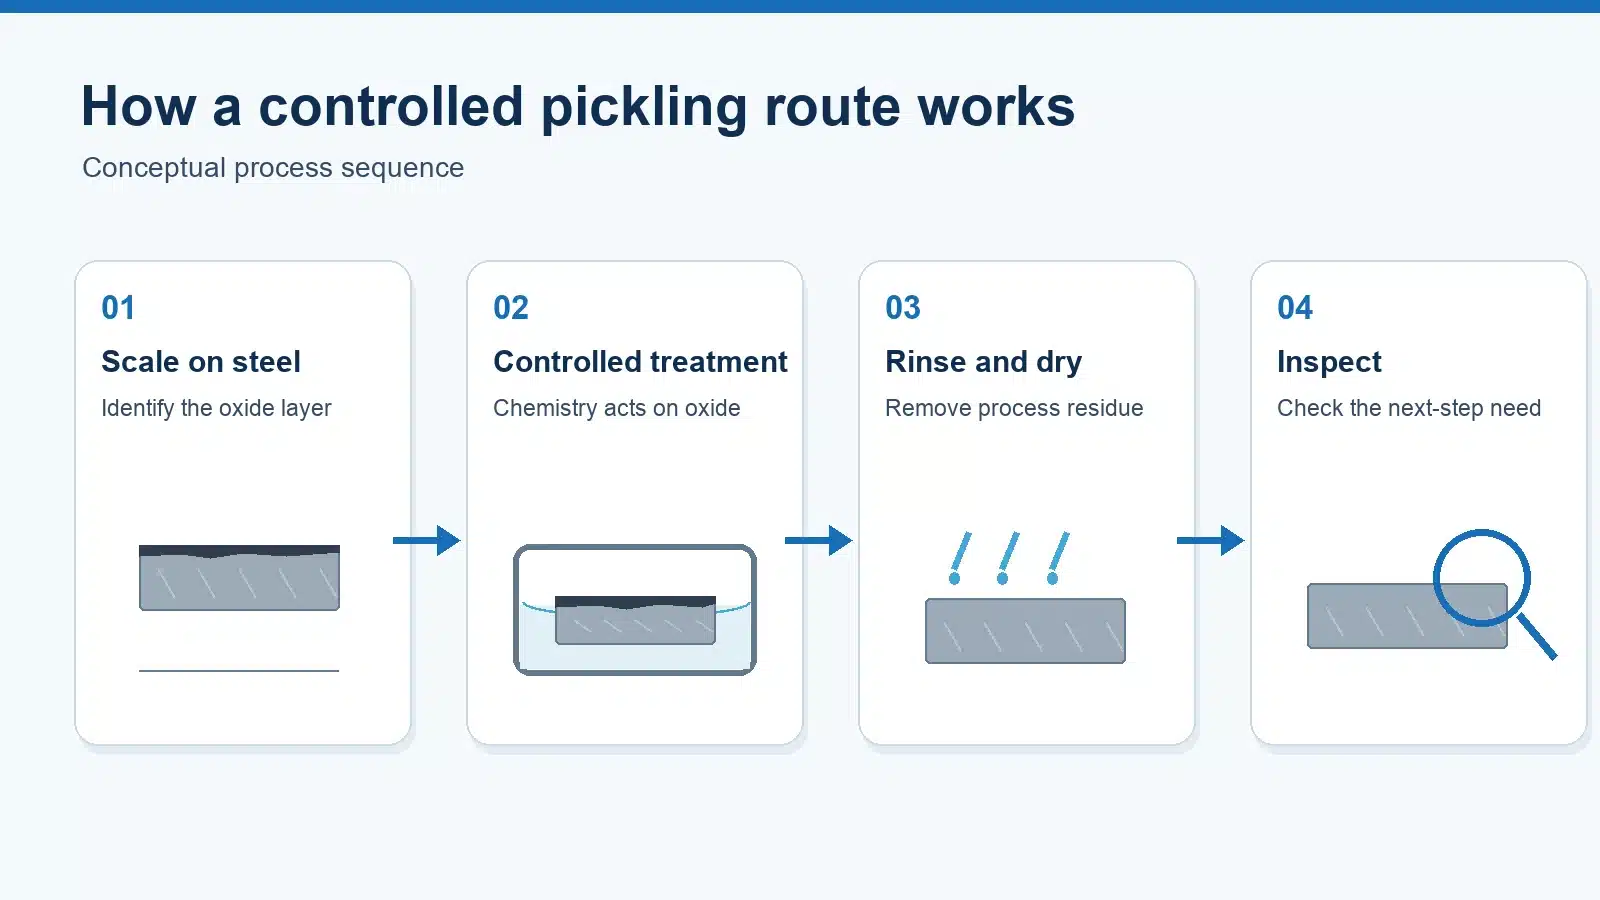
Industrial pickling is a candidate when suitable steel can pass through a controlled chemical line or be processed as a compatible batch. Its value is that chemistry reaches exposed surfaces without an abrasive tool cutting each location. Its limitation is that oxide removal is only one part of the job: a correctly treated part must also be rinsed, dried, handled, and accepted for the next process.
How Acid Pickling Removes Oxide Layers from Steel
The pickling solution reacts with and dissolves the iron-oxide scale. Process chemistry, bath condition, temperature, exposure, inhibitor use, steel grade, and the amount and condition of scale affect how much oxide and base metal are attacked. The goal is a qualified treatment that removes the required layer without unacceptable loss or residue. A household acid or rust remover cannot be assumed to reproduce an industrial pickling process.
Evaluate the most difficult geometry, not only a flat coupon. Liquid can reach a gap that a disc cannot, but rinse water and spent chemistry can also remain there. The work instruction needs a way to confirm both removal and complete post-treatment. If the next step is painting, the surface still needs whatever texture and contamination controls the coating system specifies.
Suitable Applications, Process Limitations, and Waste Treatment
Suitable batch or strip-line work can justify bath control and repeatable handling; a single local weld repair often cannot. Include racks, part spacing, rinse quality, drying, protection against re-rusting, and the treatment of spent solution in the route. US EPA steel-manufacturing guidance identifies rinse water and spent pickling liquor as distinct wastewater streams; disposal and treatment must follow the actual facility and applicable rules, not a generic article recipe.
Acid treatment can introduce hydrogen into susceptible steels. This is particularly important when assessing high-strength or hardened components, not a reason to declare every pickled mild-steel part unusable. TWI's hydrogen-embrittlement guidance calls for control of the electrochemical conditions that can release hydrogen at the component surface. Any required post-treatment must come from the qualified material/process specification; do not invent a universal bake time.
Can Laser Cleaning Remove Mill Scale from Steel?
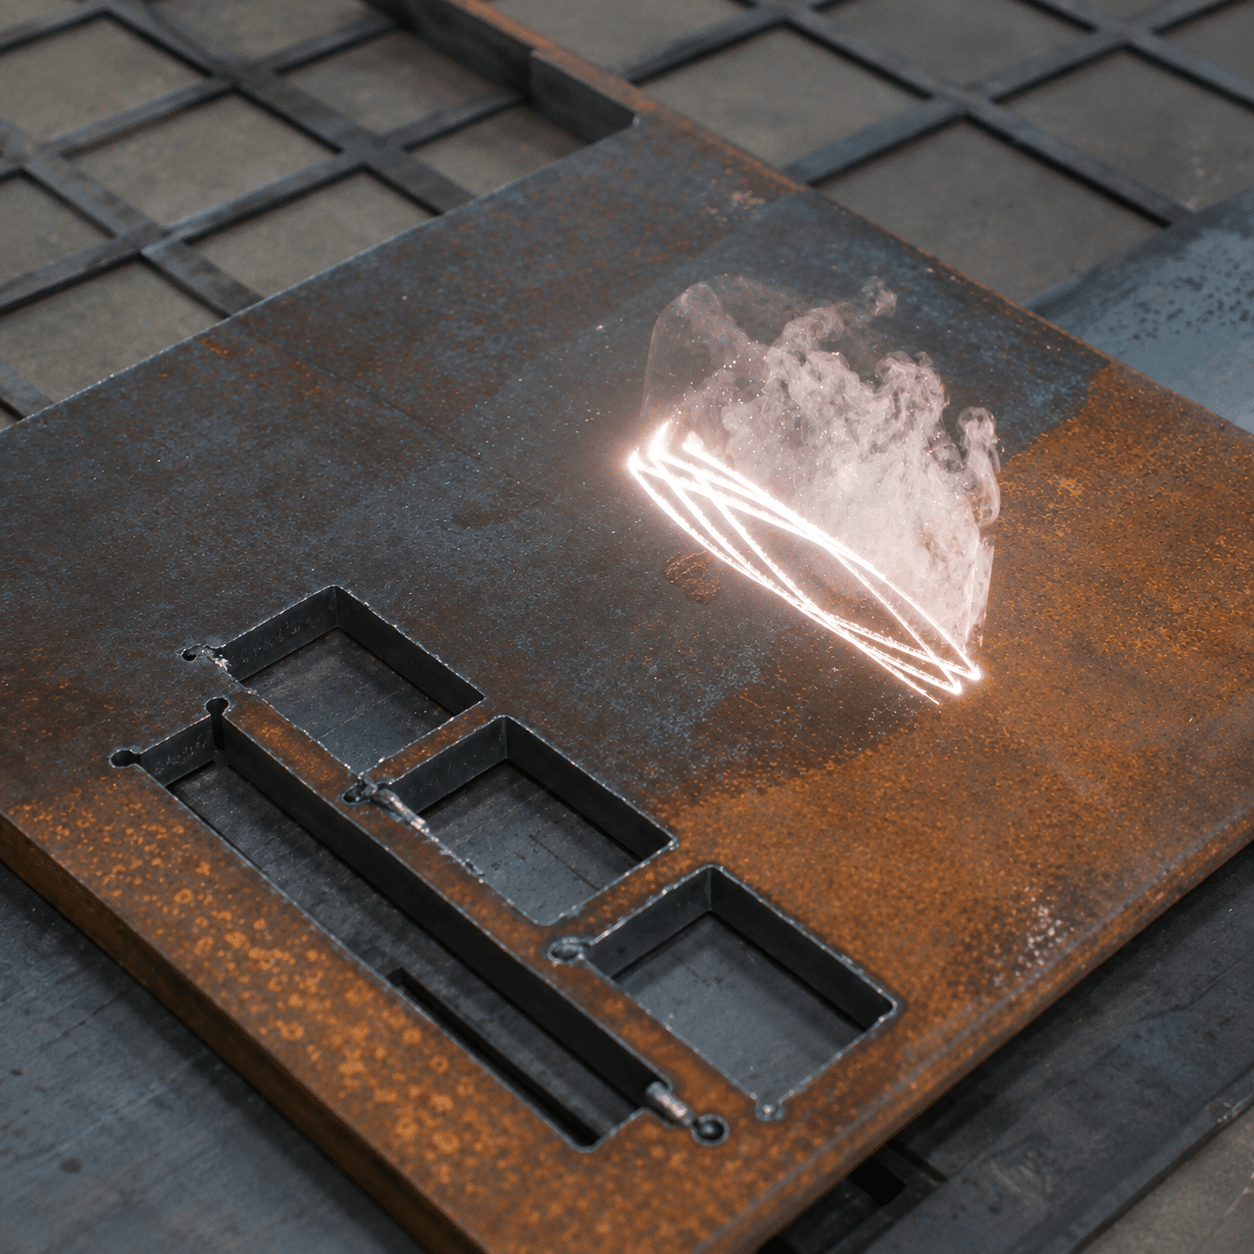
Yes, laser processing can remove scale from selected steel surfaces, but the viable window has to be established for the actual scale, steel, geometry, and endpoint. It is a non-contact energy-delivery method, not an automatic guarantee of zero substrate change. Compared with grinding or blasting, the laser head does not rub abrasive media on the part. It may be useful where local treatment and repeat motion matter; thick or tightly attached scale can demand more passes or make another method more economical.
How Laser Cleaning Removes Oxide Layers Without Abrasive Contact
The beam deposits energy in the surface layer. Depending on the oxide and exposure, heating, expansion, phase change, and rapid stress can loosen or destroy the scale, while some material may be ejected. Calling every removal event “vaporization” oversimplifies the process. The steel beneath can also absorb energy once scale thins or an area is exposed, so the same scan may behave differently at the beginning and end of a pass.
The engineering question is whether there is a repeatable set of conditions that removes enough scale while leaving the substrate acceptable. A 2024 continuous-wave fiber-laser study reported thermomechanical scale destruction under its studied conditions. A separate pulsed-laser study on oxidized SUS409 stainless steel reported oxide-film removal under its own conditions. Together, these show possible routes—not a head-to-head ranking, a transferable setting, or a test of an Oceanplayer system.
Pulsed vs. Continuous-Wave Laser Cleaning: What Changes in Practice?
A pulsed source delivers energy in separated bursts; a CW source delivers light continuously while it is on. For a regular pulse train, average power equals pulse energy multiplied by repetition rate. Pulse energy divided by pulse duration gives a peak-power estimate; the exact peak also depends on pulse shape. These distinctions are set out in Newport's laser power-and-energy tutorial. CW operation has no separate per-pulse energy in the same sense. Matching two machines by average watts therefore does not match how each exposes a point on the steel.
Spot size at the workpiece, scan or travel speed, line spacing, pulse repetition rate, overlap, and number of passes determine the local exposure history. A short pulse can localize much of the interaction during that pulse, but repeated exposure can still accumulate heat in steel; that study concerns high-repetition femtosecond processing, not a universal cleaning limit. A moving CW beam also has a finite dwell time at each location; it does not imply that the whole part is heated uniformly. Neither mode is automatically faster, harmless, or preferable for mill scale. The relevant comparison is accepted finish and complete cycle time on the same representative material, with the actual optical and scan settings recorded.

How Scale Thickness, Laser Parameters, and Steel Properties Affect Results
A loose, fractured layer and a dense attached layer do not absorb and separate identically. Mixed rust, oil, or coating over scale further changes the interaction. The apparent steel thickness can matter indirectly because a thin edge and a heavy plate tolerate different heat and geometry changes; it is not a shortcut for specifying a laser setting. Grade, prior surface condition, heat treatment, reflectivity, and access also deserve attention where they could change the result.
Begin a trial with labeled samples covering the light and difficult scale conditions. Record the source mode and optics, actual working distance, spot or treated width at the part, scan path, speed, line spacing, pulse settings if applicable, and pass count. Inspect residual oxide and the exposed steel after each relevant condition. A single bright strip is not evidence that recesses, weld edges, or an entire batch are clean.
When Laser Cleaning Needs Multiple Passes or Additional Surface Preparation
If scale remains after one pass, a repeat pass may help, but it changes time and accumulated exposure. The decision is not simply to increase power. Recheck whether the remaining dark material is oxide, whether the steel is discoloring or distorting, and whether the added pass remains within the acceptable surface condition. If the required removal or geometry cannot be achieved consistently, compare blasting, a suitable abrasive, pickling, or another qualified route rather than forcing the laser process.
For painting, removing oxide and creating the specified anchor profile are separate tasks. A laser-cleaned surface may require an additional approved profiling step or coating-system qualification. Laser texturing is possible in some configurations, but it cannot be assumed from a cleaning pass or treated as equivalent to a specified blast profile without measurement and approval.
Which Mill Scale Removal Method Is Best Before Welding or Painting?
The process that best removes scale is not necessarily the process that completes the next operation's preparation. Welding requires the specified joint condition and geometry. Painting requires the specified coating substrate condition across the area to be coated. If a frame will be welded and then painted, plan two connected preparation stages rather than declaring it finished after the weld strips are cleaned.
Before Welding: Remove Scale from the Required Joint Area Without Damaging Geometry
Start with the welding procedure specification or work instruction: identify the joint faces, adjacent cleaning zone, and any back-side access requirement. Remove scale and other contamination without rounding a bevel, altering root opening, thinning an edge, or leaving media or chemical residue. TWI's joining guidance treats cleanliness and joint geometry as linked parts of preparation and notes that the needed extent varies with material and process.
The welding procedure, not a general blog, decides how much preparation is acceptable for the actual process and consumable. Some processes or consumables may be more tolerant of surface oxide than others, but that cannot be extended to a different joint by analogy. After cleaning, check fit-up and condition; weld quality still depends on the rest of the procedure, including consumables, shielding, and parameters. For the broader laser-specific workflow, Oceanplayer's laser cleaning before welding page is a related application resource, not proof that a particular mill-scale trial has passed.
Before Painting: Meet Surface Cleanliness and Anchor Profile Requirements
Read the project coating specification and the actual coating manufacturer's application instructions together. The required visual grade, roughness or profile, permissible contamination, edge treatment, environmental conditions, and allowed time before coating may differ between a decorative indoor finish and a demanding protective system. Do not select a method only because it exposes bare-looking steel.
ISO 8501-1:2007 supplies a visual preparation-grade framework within its scope; it does not by itself measure profile or invisible contamination. Blast-profile comparators have their own scope under ISO 8503-1:2012. If a specification requires a blast-cleaned condition, a laser- or hand-cleaned appearance cannot simply be relabeled as the same grade. Use the inspection methods and limits actually required by the coating system and project authority.
When Combining Cleaning and Surface Profiling Methods Makes Sense
A selective method may remove scale from intricate details without producing the texture the coating needs; a later, controlled profiling step may complete the route. Conversely, blasting a large face may still leave a recess that needs a local follow-up. Combining methods is justified only when each step supplies a distinct required result and the sequence avoids recontamination or damage.
Plan the complete route on representative parts: what is removed first, how any residues are cleared, when profiling occurs, and when the final surface is inspected and coated. If the combination takes longer or costs more than a single qualified process, its selectivity must provide another real benefit, such as protecting geometry or accessing a difficult feature. Do not call the first stage “paint-ready” while the second remains unverified.
How Can You Verify That Mill Scale Has Been Completely Removed?
Define “completely” against the specified area, inspection method, and acceptance criterion. Visual inspection can locate remaining dark patches and changes to the steel, but it cannot prove the absence of every microscopic oxide or contaminant. A coating or welding decision may therefore need additional checks. Select a sample set that includes the worst scale, not just the easiest part, and keep an untreated comparison area or labeled original sample where practical.
Visual Inspection: Residual Scale, Surface Discoloration, and Hard-to-Reach Areas
Inspect under consistent lighting and at the angles needed to see edges, holes, recesses, weld faces, and the back of sections. Compare the cleaned area with the required visual condition, not with a marketing before-and-after photograph. Dark islands after brushing can be attached scale; orange rust appearing after wet treatment can indicate inadequate drying or delayed protection. A laser-treated patch that develops new color, melting, or distortion calls for a pause and substrate assessment, not an automatic extra pass.
If color alone cannot distinguish remaining oxide from a harmless surface tint, use an appropriate additional method agreed by the process or quality owner. Record the observation and decision. The goal is a reproducible acceptance rule, not a promise that one visual cue always diagnoses the surface.
Check Base-Metal Condition, Surface Profile, and Remaining Contaminants
Inspect what the removal method might have changed. For grinding, this can include edge shape, thickness, scratches, and fit-up. For blasting, include the specified profile and any contamination or media-related issue. For pickling, confirm the qualified rinse and dry result and examine crevices. For laser processing, look for unacceptable heat-related changes as well as residual oxide. The actual checks should follow the material and downstream process; no single instrument substitutes for all of them.
For coating work, a visually clean surface may still carry dust, soluble salts, oil, or an unsuitable profile. A roughness average and a blast profile grade are not interchangeable merely because both describe surface texture. Use the test method and limit named in the project or coating specification, and record where on the part it was measured.
Follow the Applicable Welding or Coating Preparation Specification
Before treating production parts, write down the required surface, who approves it, which method measures it, and what happens if a result fails. Include both typical and difficult parts. Retain the steel identification, pre-clean condition, method settings, passes, operator or cell, inspection result, and any rework. For welding, carry the prepared joint into the specified weld checks; for coating, carry the surface through application under the specified conditions. Neither a bright joint nor a measured blast profile alone proves the final weld or coating will meet its service requirements.
What Safety Precautions Are Required for Each Method?
The hazards depend on the process, the material being removed, and the actual work area. A known, uncoated steel oxide is different from scale beneath an old lead-containing coating or other unknown deposit. Identify the layer before selecting extraction, containment, handling, and disposal controls. The following distinctions guide a site-specific risk assessment; they are not a universal PPE specification.
Dust, Flying Particles, Noise, and Abrasive Blasting Hazards
Grinding and blasting can throw particles and generate dust, sparks, and noise. Blasting dust may contain material from both the abrasive and the surface being cleaned. NIOSH's abrasive-blasting guidance describes why containment and exposure controls depend on those materials. “Sandblasting” does not mean silica sand is the correct medium, and changing the medium does not remove every dust hazard.
Guard the tool, secure the work, control nearby combustibles, and assess ventilation and worker protection under the equipment and workplace requirements. The relevant controls differ between a small guarded grinder, an enclosed wheel-blast machine, and open-air blasting.
Chemical Exposure, Acid Handling, and Wastewater Management
Pickling needs a qualified chemical process: compatible tanks and handling equipment, exposure and splash controls, a controlled rinse/dry route, and management of spent liquor and rinse water. A worker should not mix or substitute acids from a blog instruction. Review the actual chemical safety data, process design, material compatibility, and local discharge rules. A part that looks bare can still carry liquid or residues into a joint, coating operation, or hidden cavity.
Laser Radiation, Fume Extraction, and Controlled Work Areas
Assess the accessible laser beam in each operating and service mode, including reflections from the steel and possible openings beyond the work area. Health Canada's laser-product guidance identifies Class 4 direct, reflected, and scattered beam exposure and possible fire hazards; a fully engineered enclosure may have a different external classification from the embedded source. Determine barriers, beam termination, interlocks, access control, training, and wavelength-appropriate eye protection from the actual system and risk assessment.
Laser cleaning also creates removed material that must be captured or controlled. The plume composition depends on the scale and any other layer present. “No abrasive media” does not mean no airborne exposure or waste. Extraction, collection, and disposal need to match the workpiece and operating arrangement.
Which Method Is Most Cost-Effective for Your Application?
The cost-effective method is the one that repeatedly delivers the required result at an acceptable total cost—not the one with the lowest tool price or fastest visible cleaning pass. Compare methods on the same steel condition and part mix, with the same acceptance rule. If one route needs a second pass, separate profiling, or extra rinsing, include that work instead of comparing only the first pass.
Equipment, Consumables, Labor, and Waste Disposal Costs
Count the equipment or service charge, fixtures, abrasive media or discs, chemicals, utilities, extraction and containment, maintenance, inspection, rework, and waste treatment. Include operator time spent loading, repositioning, and dealing with inaccessible areas. A bath process might spread its setup cost over many parts but still add rinse and wastewater work; a portable abrasive may have low setup effort but variable consumable and labor cost. The relevant accounting period and production volume must be specified before a cost comparison means anything.
Cleaning Speed, Automation Potential, and Total Cost per Part
Measure elapsed time from the start of handling to an accepted prepared part, including repeat passes and checks. For large surfaces, accepted area per complete operating hour may be useful; for local weld zones, accepted joints or parts per hour can be clearer. A programmable cell can improve repeatability on a suitable part, but integration, fixturing, and inspection still consume time. Neither automation nor rated laser power proves a lower cost per accepted part.
A simple comparison is total relevant operating cost for the trial divided by the number of parts accepted under the same rule. This is a calculation method, not a claimed Oceanplayer cost or productivity result. Keep rejected and reworked parts in the record so the rate cannot be improved by omitting difficult cases.
Choosing a Method Based on Production Scale and Quality Requirements
For one repair, compare the practical setup and the risk to local geometry. For recurring batches, compare fixture time, process drift, consumable or bath changes, and acceptance consistency. For protective coating, any method that still needs an additional profile-creation stage must be costed as a combined route. For a qualified weld, the final decision includes whether joint preparation supports the welding procedure without added repair.
The buyer's best request is a trial plan: provide steel grade and thickness, part drawings or photos, scale condition, required area, next-process specification, annual or batch volume, and difficult geometry. Ask each candidate supplier or internal team to return the same record of method conditions, accepted result, full-cycle time, and unresolved limits. That creates a defensible comparison without pretending a generic price-per-square-meter figure applies to your plant.
Frequently Asked Questions About Mill Scale Removal
Can You Paint Directly Over Mill Scale?
Do not assume so for a protective coating. Residual mill scale is generally an unsuitable base for modern high-performance coating systems on structural steel, and the coating specification may require both its removal and a defined profile. If a particular product or service condition permits a different route, follow that documented system rather than transferring an exception to another paint.
Can You Weld Steel Without Removing Mill Scale?
Only when the actual welding procedure and joint requirements allow that surface condition. Some processes and consumables tolerate oxide differently, but visual tolerance is not a substitute for the approved procedure. Where preparation is specified, clean the required joint area and preserve its geometry; then verify the weld under the normal acceptance plan.
Will a Wire Brush Completely Remove Mill Scale?
An ordinary wire brush may remove loose flakes while firmly attached scale remains. Inspect the required area after brushing, especially dark islands and recesses. If attached oxide persists, use a suitable descaling abrasive or another qualified process rather than judging by shine alone.
Can Laser Cleaning Remove Thick or Tightly Adhered Mill Scale?
It can be investigated, but one pass and a fixed setting cannot be promised. Compare representative heavy-scale samples, track pass count and surface change, and measure the complete cycle. If the substrate is affected before removal is adequate, or the route becomes uneconomic, compare another method or a combined preparation sequence.
Does Removing Mill Scale Damage the Steel Surface?
It can. Grinding can cut steel, blasting intentionally changes texture, uncontrolled pickling can attack the substrate, and laser exposure can cause unacceptable thermal or surface changes. The relevant question is whether the chosen process stays within the part's dimensional, metallurgical, and next-operation limits on representative samples.
What Is the Difference Between Mill Scale and Rust?
Mill scale forms during hot processing; rust develops later when steel corrodes in its environment. A part can carry both. Their attachment and response to cleaning may differ, so identify the actual layers before accepting a method that only removes the loose orange material.
Technical References
- Steel Construction Info, “Surface Preparation” — mill scale, blasting, coating-surface context, and hand-tool limits.
- ISO 8501-1:2007 — scope of visual rust and preparation grades for steel substrates.
- ISO 8503-1:2012 — scope of blast-cleaned surface-profile comparators.
- TWI, “What is surface preparation for joining?” — joint geometry and cleanliness before welding.
- TWI, “What is hydrogen embrittlement?” — hydrogen-entry risks relevant to controlled pickling.
- US EPA, Guidance Manual for Iron and Steel Manufacturing Pretreatment Standards — industrial pickling and associated waste streams; US regulatory context only.
- Zhurba and colleagues, “Investigation of the Process of Laser Descaling of Mill Metal” (2024) — abstract-level evidence of a selected CW fiber-laser descaling route, not Oceanplayer equipment performance.
- Guo, Martukanitz and DebRoy, “Laser assisted cleaning of oxide films on SUS409 stainless steel” (2004) — abstract-level evidence of a selected pulsed oxide-cleaning route.
- Newport, “Average and Peak Power — A Tutorial” — definitions for pulse energy, repetition rate, average power and peak power.
- Florian and colleagues, “Influence of Heat Accumulation ... on Steel” (2023) — high-repetition femtosecond steel-processing study; not a mill-scale cleaning threshold.
- NIOSH, “Abrasive Blasting” — archived US occupational-health summary of blasting dust and exposure hazards.
- Health Canada, “Laser products” — laser class and direct/reflected/scattered-beam hazards; site assessment remains necessary.