

How to Remove Paint Overspray from Metal Without Damaging the Original Finish
The safest way to remove paint overspray from metal is to identify both the unwanted deposit and the finish that must remain, then test the least aggressive compatible method on a representative area. Start with cleaning and a controlled manual method where the finish permits it; use a finish-approved solvent only after compatibility testing; and consider laser cleaning only when the coating stack, geometry, safety controls, and acceptance criteria can be evaluated in a representative trial. Expand the process only after the cleaned, dry test area shows acceptable color, gloss, texture, coating condition, and function.
Key takeaways
- Overspray age matters, but the original finish usually sets the stricter limit.
- A successful method must remove the deposit and preserve the required finish; deposit removal alone is not a pass.
- Detailing clay, solvents, and laser cleaning work through different mechanisms and create different failure modes.
- Test one method at a time, remove residues, allow the area to dry, and compare it with an untreated reference.
- If the original coating is already softened, cracked, lifting, or chemically attacked, local refinishing may be more controlled than further cleaning.
Identify the Overspray and the Finish You Need to Protect
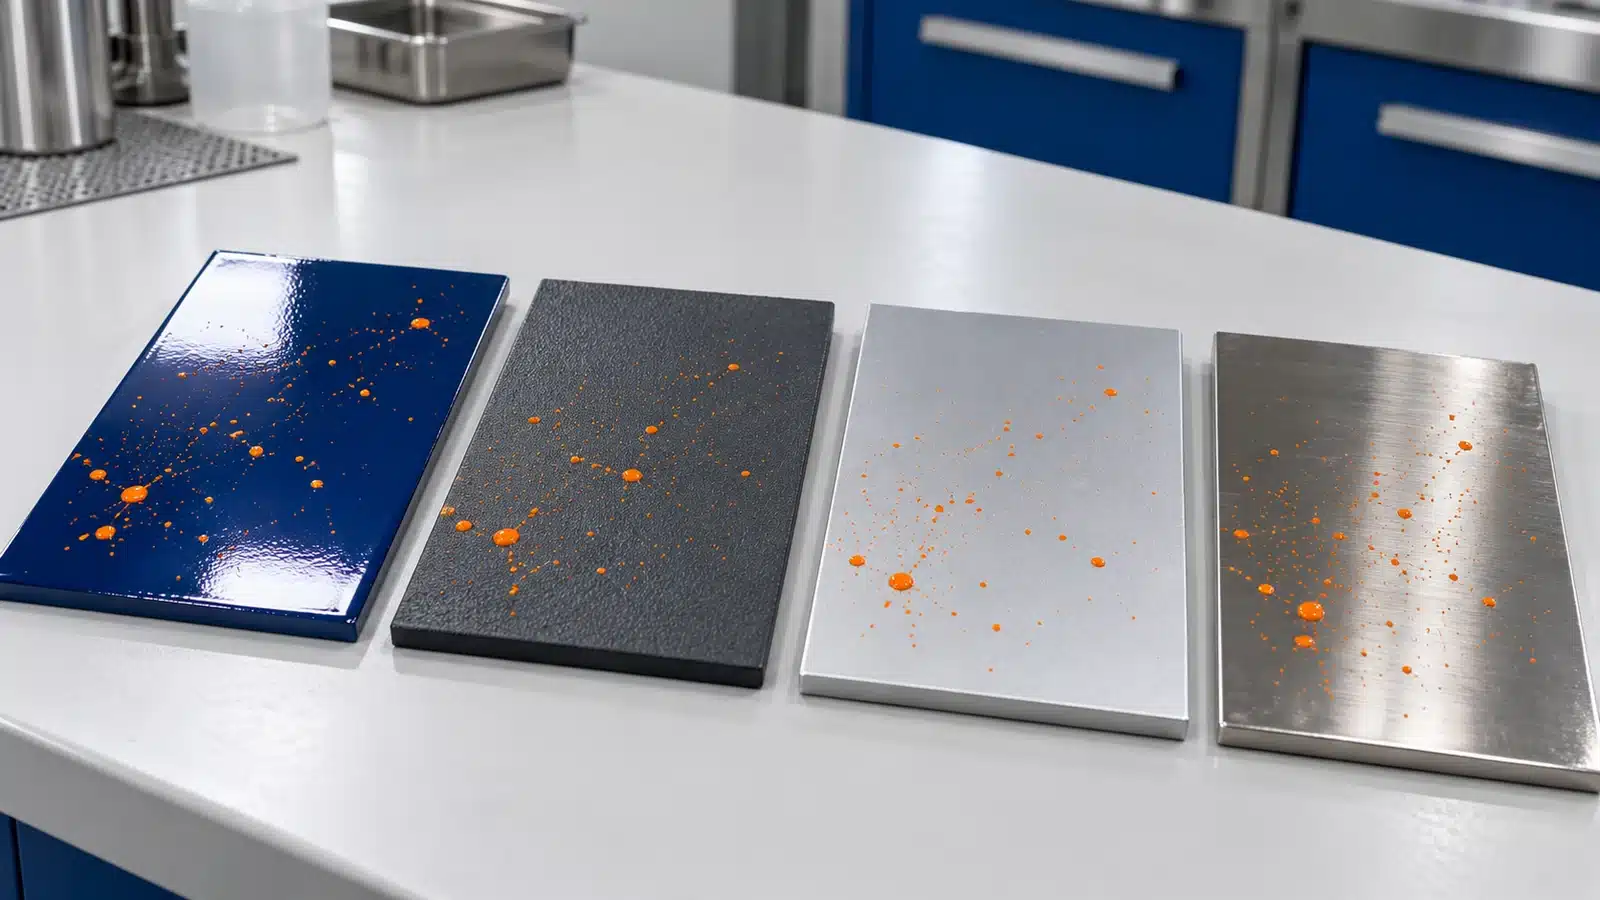
“Metal” describes the substrate, but it does not describe the surface the cleaning method will contact. The visible surface may be clear-coated paint, a single-stage liquid coating, powder coating, anodizing, plating, conversion coating, brushed bare metal, or a precision-machined face. Overspray removal succeeds only when the unwanted paint is removed without pushing that required surface outside its acceptance limits.
Before selecting a method, record four facts: the overspray product if known, its cure history, the original finish, and the condition that must remain. Also identify nearby seals, labels, plastics, adhesives, joints, openings, and electrical components. A method that is compatible with the exposed metal may still damage one of these adjacent materials.
Fresh, Dried and Fully Cured Overspray
Fresh overspray may still contain mobile solvent or water and may release with the cleaner specified for the original finish. Dried overspray has lost much of its carrier but may not have completed its chemical cure. Fully cured deposits are usually harder, more cohesive, and more resistant to mild cleaning. The boundaries between these states depend on paint chemistry, film thickness, temperature, humidity, and cure schedule; elapsed time alone is not a reliable classification.
This difference changes the risk of delay. AkzoNobel’s maintenance guidance for its Interpon D architectural powder coatings advises removing paint splashes before they dry because later removal can require more aggressive methods that may damage the powder-coated surface. That guidance is product-specific, but the engineering lesson is broader: identify the deposit early and consult the overspray paint’s technical data rather than assuming that “dry to the touch” means fully cured.
Do not wipe an unidentified fresh deposit immediately across the surface. A wipe can spread dissolved pigment, press particles into a soft finish, or enlarge the affected area. First isolate the work area, check whether the original finish is itself fresh or heat-softened, and blot or lift only when the applicable coating and cleaner instructions support that action.
Check the Original Coating and Acceptable Surface Condition
Inspect an unaffected reference area before cleaning. Record the original color, gloss, texture, orange peel, directional grain, and any pre-existing scratches, chalking, corrosion, or coating loss. If the part has a sealing, electrical, dimensional, or adhesion function, include that in the acceptance criteria. A cosmetic pass cannot substitute for a functional requirement.
The same method can produce different outcomes on different finishes. A durable glossy automotive coating may tolerate a lubricated clay product that would alter a matte coating. A solvent that softens the overspray may also swell the original coating. A laser setting that removes an opaque deposit from bare metal may heat, discolor, roughen, or strip a retained coating beneath it.
Define “no damage” as observable and measurable conditions, not as a promise. For example:
- no visible overspray under agreed lighting and viewing distance;
- no new haze, color shift, gloss patch, texture change, scratch pattern, or exposed substrate;
- no tackiness, swelling, whitening, lifting, or edge attack after drying;
- no unacceptable coating-thickness change where thickness is a valid control;
- no loss of fit, conductivity, sealing, adhesion, or other specified function.
Which Overspray Removal Method Should You Try First?
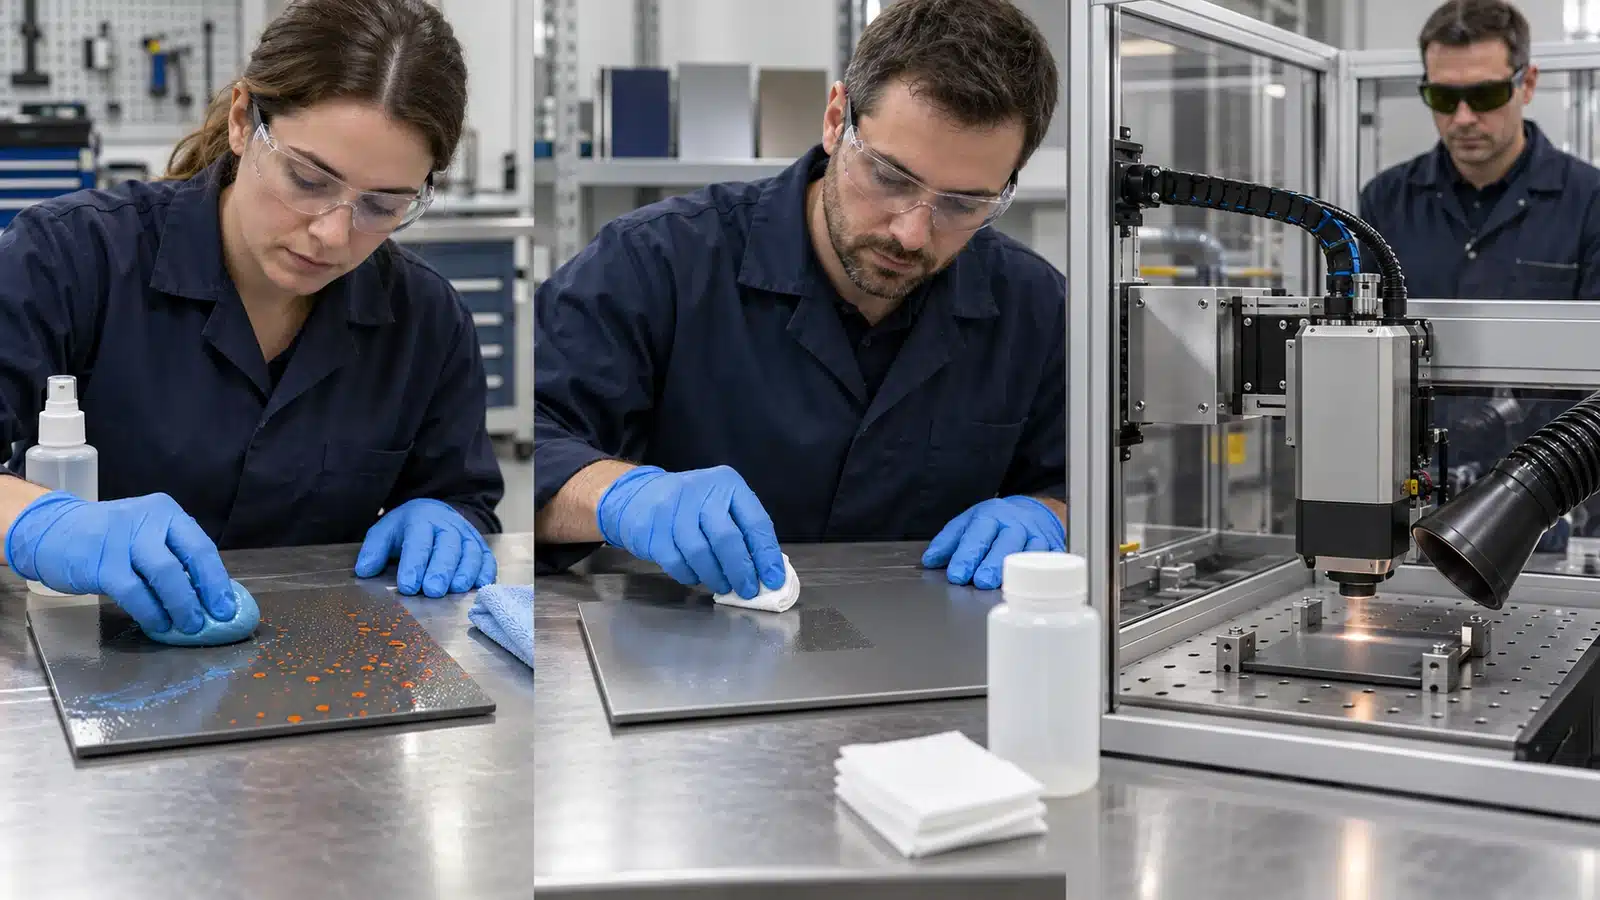
Choose the first trial by combining the overspray condition with the finish that must remain. The goal is not to start with the fastest-looking method. It is to start with the method that offers a plausible removal mechanism while creating the smallest irreversible change to the retained surface.
Compare Methods by Finish Type and Overspray Condition
| Surface and deposit condition | Reasonable first trial | Main risk to control | Move to another route when |
|---|---|---|---|
| Fresh or weakly attached deposit on a finish approved for washing | Finish-approved mild cleaner, soft cloth or sponge, and controlled lifting | Spreading pigment, trapping grit, or attacking a still-soft original coating | The deposit smears, the finish becomes tacky, or removal requires rising force |
| Light, raised cured particles on a durable glossy finish | A compatible detailing-clay system with its specified lubricant | Marring from contaminated media, inadequate lubrication, or excess pressure | The finish is matte/textured, the particles do not release, or gloss changes |
| Chemically susceptible deposit on a known resistant finish | Small, timed trial with a cleaner or solvent approved for that coating stack | Swelling, color transfer, gloss change, residue, and adjacent-material attack | The original finish softens, color transfers, or the cleaner evaporates before controlled removal |
| Industrial deposit where contact methods cannot reach or would create unacceptable secondary contamination | Qualified laser-cleaning trial with extraction and defined inspection | Removing or heating the retained coating, substrate change, incomplete extraction, and line-of-sight limits | A selective process window cannot be demonstrated on a representative sample |
| Overspray bonded to a damaged, porous, cracked, or lifting coating | Evaluate local repair or refinishing | Enlarging an existing coating failure while chasing complete removal | The original finish cannot meet acceptance even after the deposit is removed |
This table is a starting logic, not a universal recipe. The actual paint manufacturer, coating supplier, part owner, and applicable safety controls may restrict the available methods further.
Why the Least-Aggressive Method Is the Starting Point
Cleaning changes a surface through mechanical contact, chemical interaction, energy input, or some combination of the three. More rubbing increases the chance of abrasion. A stronger solvent may dissolve the unwanted paint more quickly but can also penetrate or soften the original film. Higher laser exposure may improve deposit removal while increasing heat accumulation or damage to the retained layer.
A least-aggressive sequence limits irreversible change while producing information. If a mild trial removes the deposit cleanly, escalation is unnecessary. If it fails without changing the finish, the result narrows the next choice. If the finish changes, the trial provides a stop signal before the whole component is affected.
“Least aggressive” does not mean repeating an ineffective action indefinitely. Repeated rubbing can cause more damage than one well-controlled alternative. Set a small test area, a defined number of passes or contact interval based on the product instructions, and a stop condition before starting.
Test the Removal Method Before Treating the Whole Surface
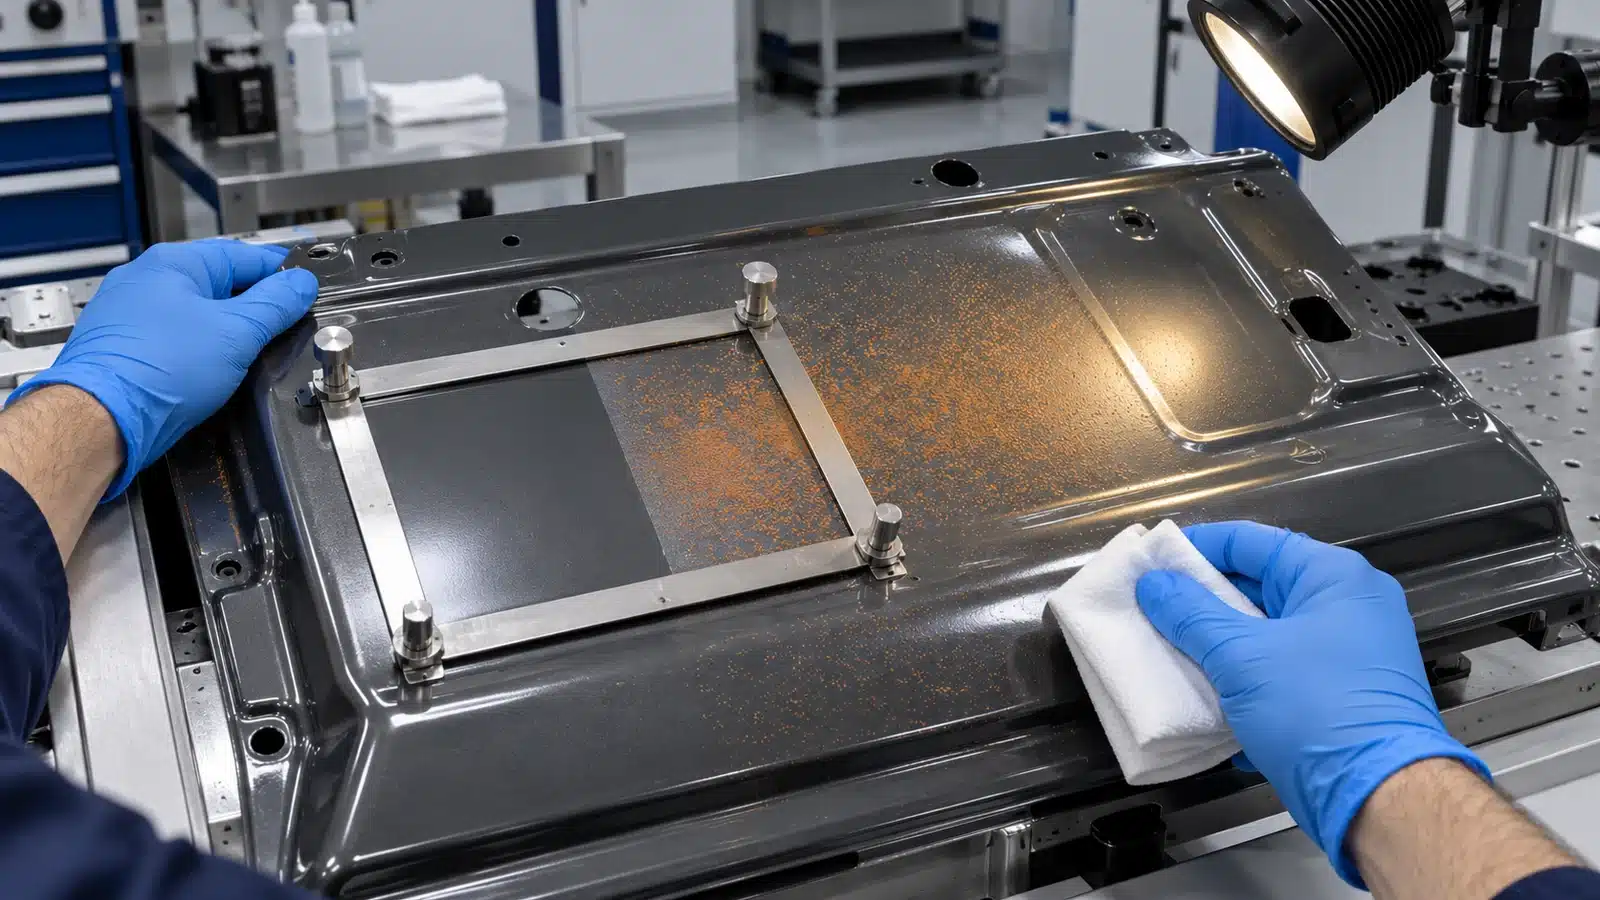
A representative test separates a plausible method from a production-ready process. It should reproduce the real coating stack, overspray condition, geometry, access, operator technique, residue-removal step, and inspection method. A test on bare scrap metal does not qualify a process for an intact painted or powder-coated part.
Clean, Document and Select a Representative Test Area
Remove loose dust with a method known to be safe for the original finish. Otherwise, grit can turn a soft cloth or clay into an uncontrolled abrasive. Photograph the test area and an unaffected reference under the same lighting. Mark the boundary in a way that does not introduce adhesive or ink contamination.
Choose an area that represents the hardest meaningful condition, not only the easiest flat patch. Include relevant edges, recesses, texture, coating thickness, and overspray density. If a hidden area has a different cure history or finish, it may be useful for compatibility screening but cannot alone prove the visible production area will pass.
Record at least:
- part and substrate identification;
- original finish and known coating system;
- overspray product, age, and cure history when available;
- starting photographs and observed defects;
- method, product, batch, tool, and operator;
- exposure, contact, or laser parameters that can be reproduced;
- residue-removal and drying procedure;
- acceptance checks and result.
Test One Method at a Time and Inspect After Drying
Changing several variables at once prevents diagnosis. If a clay step, solvent wipe, and polish are performed on the same spot, a good final appearance does not show which step removed the overspray or which one thinned or altered the original finish. Separate test cells or perform a documented sequence with inspection between stages.
Remove cleaner, lubricant, dissolved paint, and debris as directed. Then allow the area to dry and return to a stable temperature before judging it. Wetting can temporarily hide fine scratches, haze, whitening, or gloss differences. Inspect from several angles under consistent diffuse and directional light, and compare the result with the untreated reference rather than relying on memory.
Expansion should follow a passed test cell. Keep the same method, product, tool condition, contact technique, and acceptance checks. If geometry or contamination changes across the part, create another representative test rather than assuming the first window transfers unchanged.
How to Remove Light Overspray with Detailing Clay

Detailing clay can remove raised particles because the lubricated, conformable media contacts protrusions above the surface and pulls or shears them away during motion. The same contact can mar a finish if the media traps hard debris, lubrication fails, pressure rises, or the coating is too soft or too textured.
Suitable Finishes, Lubrication and Contact Pressure
Use a clay system only within the product’s stated surface scope. For example, 3M describes its 38070 Cleaner Clay as a mildly abrasive professional product for contaminants including paint overspray on exterior automotive paint, glass, and metal. Its directions specify washing first, using light pressure with soapy water as lubricant, rinsing and drying, folding the clay periodically, and discarding excessively contaminated material. Those instructions support that named product; they do not establish that every clay, lubricant, paint, or industrial coating is compatible.
During a trial, the media should glide rather than drag. Use clean sections of the clay and inspect both the media and surface frequently. Stop if resistance rises, visible color transfers from the original finish, the clay embeds sharp particles, or the test area develops haze. Do not carry contaminated clay from a heavily affected area onto a cleaner zone.
Matte, satin, textured, soft, recently applied, and powder-coated finishes need extra caution. AkzoNobel’s guidance for its Interpon D architectural powder coatings calls for warm water, a non-abrasive pH-neutral detergent, and soft cleaning materials; it excludes abrasive cleaner or polish and requires testing stronger products on a small inconspicuous area. That does not define every powder coating, but it shows why an automotive correction method should not be transferred to an unknown industrial powder film without supplier approval.
When Polishing Creates More Risk Than Benefit
Polishing does not simply “clean” a coating. An abrasive polish levels the upper surface to reduce visible defects, which may restore clarity on a compatible glossy finish but can also reduce film thickness, change texture, or create a glossy patch on a matte surface. It should not be treated as an automatic next step after clay.
Consider polishing only when the retained coating is designed for that correction process, sufficient film remains, and the acceptance criterion permits the resulting texture and gloss. If the overspray is still present as discrete particles, adding more polishing pressure can grind contamination across the surface. If the original finish is thin, weathered, textured, or functionally coated, local repair may be safer.
When Can Solvents Remove Paint Overspray Safely?
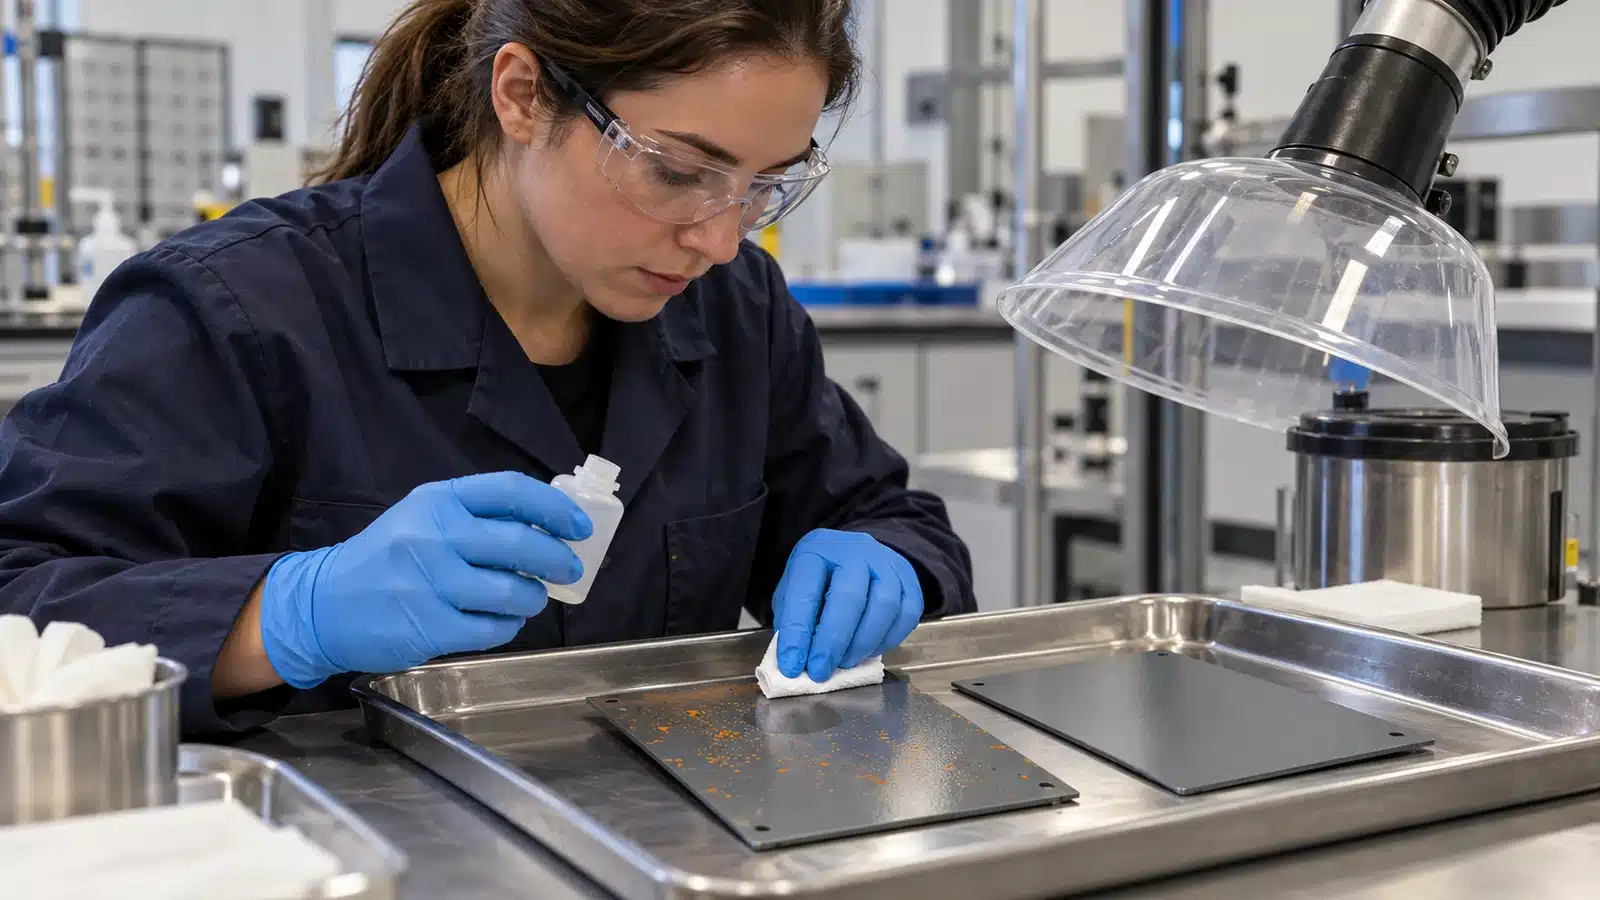
A solvent can remove overspray when it softens, swells, or dissolves the unwanted deposit enough to lift it while leaving the original coating and adjacent materials within acceptance. Safety depends on that chemical selectivity, controlled exposure, complete residue removal, and workplace controls. The word “solvent” does not identify a safe strength or compatibility class.
Match the Solvent to the Deposit and Original Coating
Start with the technical data for both the overspray paint and the original coating. Identify the binder chemistry, cure state, recommended cleanup materials, and prohibited cleaners. Also check plastics, seals, printed markings, adhesives, and previous repairs within the exposure area.
Run a small compatibility trial using the lowest exposure that can answer the question. Apply the product with a controlled tool rather than flooding joints or openings. Watch for pigment transfer from the original finish, tackiness, swelling, whitening, gloss change, edge lifting, or texture softening. A visually clean wet surface is not a pass; remove residues and inspect it dry.
Supplier rules can be narrower than general workshop practice. Interpon D guidance, for example, excludes cleaners containing ketones or esters for its stated architectural powder-coating scope and warns against strong solvents. This is one reason acetone cannot be recommended as a universal overspray remover.
Control Contact Time, Residues and Safety Risks
Contact time should come from the approved product process and the representative trial, not from a generic online dwell time. Long exposure can let a cleaner migrate into pores, seams, labels, or coating defects. Very rapid evaporation can encourage repeated application and increase vapor exposure without improving controlled removal.
Plan the entire sequence before opening the container: application, agitation if permitted, capture of dissolved paint, rinse or neutralization where specified, drying, waste collection, and inspection. Do not mix cleaners unless the product instructions explicitly permit it.
Workplace controls are part of method selection. OSHA notes that solvent exposure can affect the nervous system, reproductive system, liver, kidneys, respiratory system, skin, and cancer risk depending on the substance and exposure. Use the current SDS, ventilation or local exhaust, ignition controls, compatible gloves and eye protection, exposure assessment, and applicable local rules. In the United States, EPA’s current methylene-chloride risk-management rule prohibits most uses and sets specific protections for limited continuing uses; that U.S. rule should not be presented as a global solvent standard.
Can Laser Cleaning Remove Overspray Without Damaging the Finish?
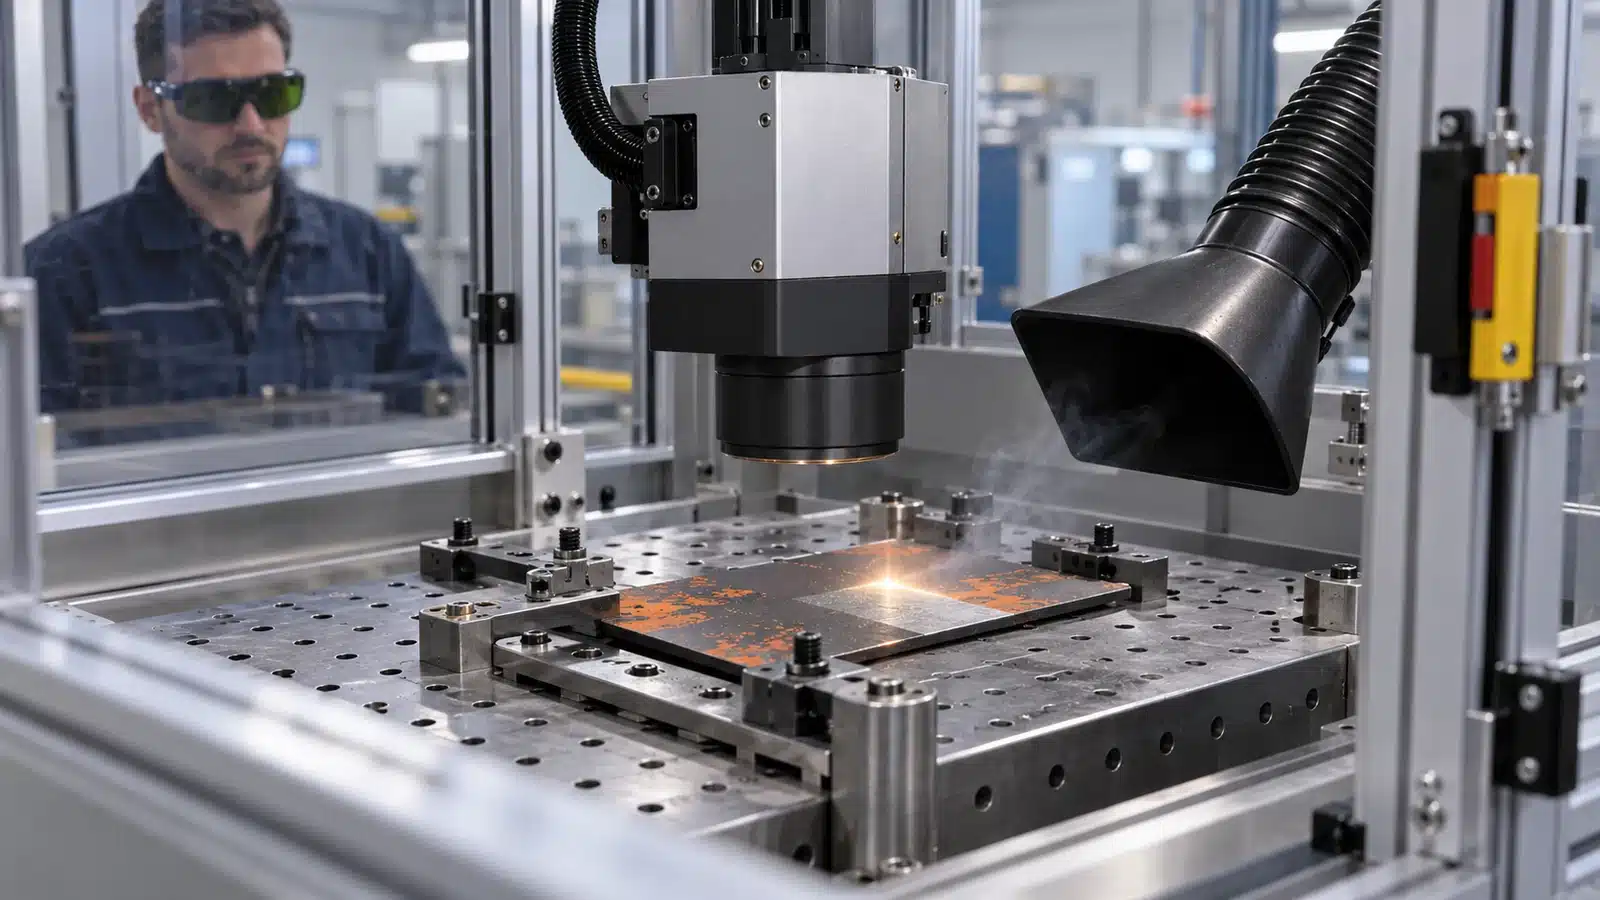
Sometimes—but only when the unwanted paint and retained surface have a controllable difference in optical absorption, ablation threshold, adhesion, thermal response, or layer behavior. Laser cleaning is not automatically selective merely because a scanner can place the beam accurately. A process window must remove the overspray while keeping the original coating, substrate, and adjacent features within acceptance.
How Laser Parameters and Coating Selectivity Affect the Result
Laser energy absorbed by the surface can heat, decompose, ablate, fracture, or debond a coating. The result depends on wavelength, pulse duration, pulse energy, repetition frequency, spot size, beam profile, scan speed, line spacing, pulse overlap, number of passes, focus, and the thermal and optical properties of every layer. Average power alone cannot predict the outcome.
Two controls must be separated:
- Footprint control determines where the beam travels and how evenly adjacent scan lines and pulses cover the area.
- Depth or layer selectivity determines whether the overspray releases before the retained finish changes.
A scanner can produce a precise footprint and still remove, melt, discolor, or roughen the underlying coating. Repeated passes can accumulate heat even when each pulse is brief, while insufficient exposure can leave removal incomplete and require a separate residual-paint check.
A 2025 study by Wang and colleagues illustrates why the process window is material-specific. The researchers used a 1064 nm, 100 ns pulsed laser on a particular paint system over 2A02 aluminum turbine-blade material and observed different removal and substrate-remelting outcomes as power, speed, frequency, and exposure changed. The study supports parameter qualification and substrate inspection. It does not establish settings for decorative overspray on clear coat, powder coating, steel, or an Oceanplayer system.
When Laser Cleaning Is Suitable—and When It Is Not
Laser evaluation is most plausible when the part is valuable, the target is localized, the surface can be reached by line of sight, contact media or liquid residues are undesirable, and the layer stack can be sampled and inspected. A manufacturer describes selective coating removal using controlled laser parameters and monitoring, showing the type of industrial application available from qualified systems. That capability still has to be proven for the actual part.
Laser cleaning may be a poor choice when the original finish is unknown, the overspray and retained coating respond similarly, the geometry hides critical areas, the surface is highly reflective or optically variable, heat-sensitive components are nearby, fumes cannot be captured, or the acceptance limit is tighter than available measurement can verify. For a large, lightly contaminated painted panel, a compatible manual method may be simpler and less risky.
The equipment and work area also require an application-specific laser-safety assessment. Beam enclosure, access control, protective eyewear, reflected-beam hazards, extraction, fire risk, and decomposition products depend on the actual system and materials. OSHA notes both beam and non-beam hazards in industrial laser workplaces and that certain laser outputs can injure the eye and skin. A paint-removal trial should not proceed from cleaning parameters alone.
What a Representative Laser Cleaning Trial Must Prove
A meaningful trial should use a sample or sacrificial area that represents the production substrate, original finish, overspray product, cure state, thickness, color, geometry, and heat-sinking condition. Record the laser source and delivery configuration as well as pulse, frequency, spot, focus, scan, overlap, pass, and extraction conditions.
The trial must prove both sides of the requirement:
- Removal: the defined overspray is removed to the required completeness, including edges and texture valleys.
- Retention: the original finish shows no unacceptable color, gloss, texture, thickness, adhesion, thermal, dimensional, or functional change after cleaning and cooling.
Test a small range around the provisional setting rather than a single “good-looking” point. This shows whether the process has usable margin or sits on a narrow threshold. Include start/stop zones and areas where the scanner changes direction, because local overlap can differ from the center of a straight pass.
If you want to evaluate laser paint removal for an industrial component, contact Oceanplayer with the substrate, original finish, overspray identity and cure history, geometry, photos, required retained condition, and acceptance method. A trial can then determine feasibility; it should not be treated as a promised production result.
How to Verify the Finish After Overspray Removal
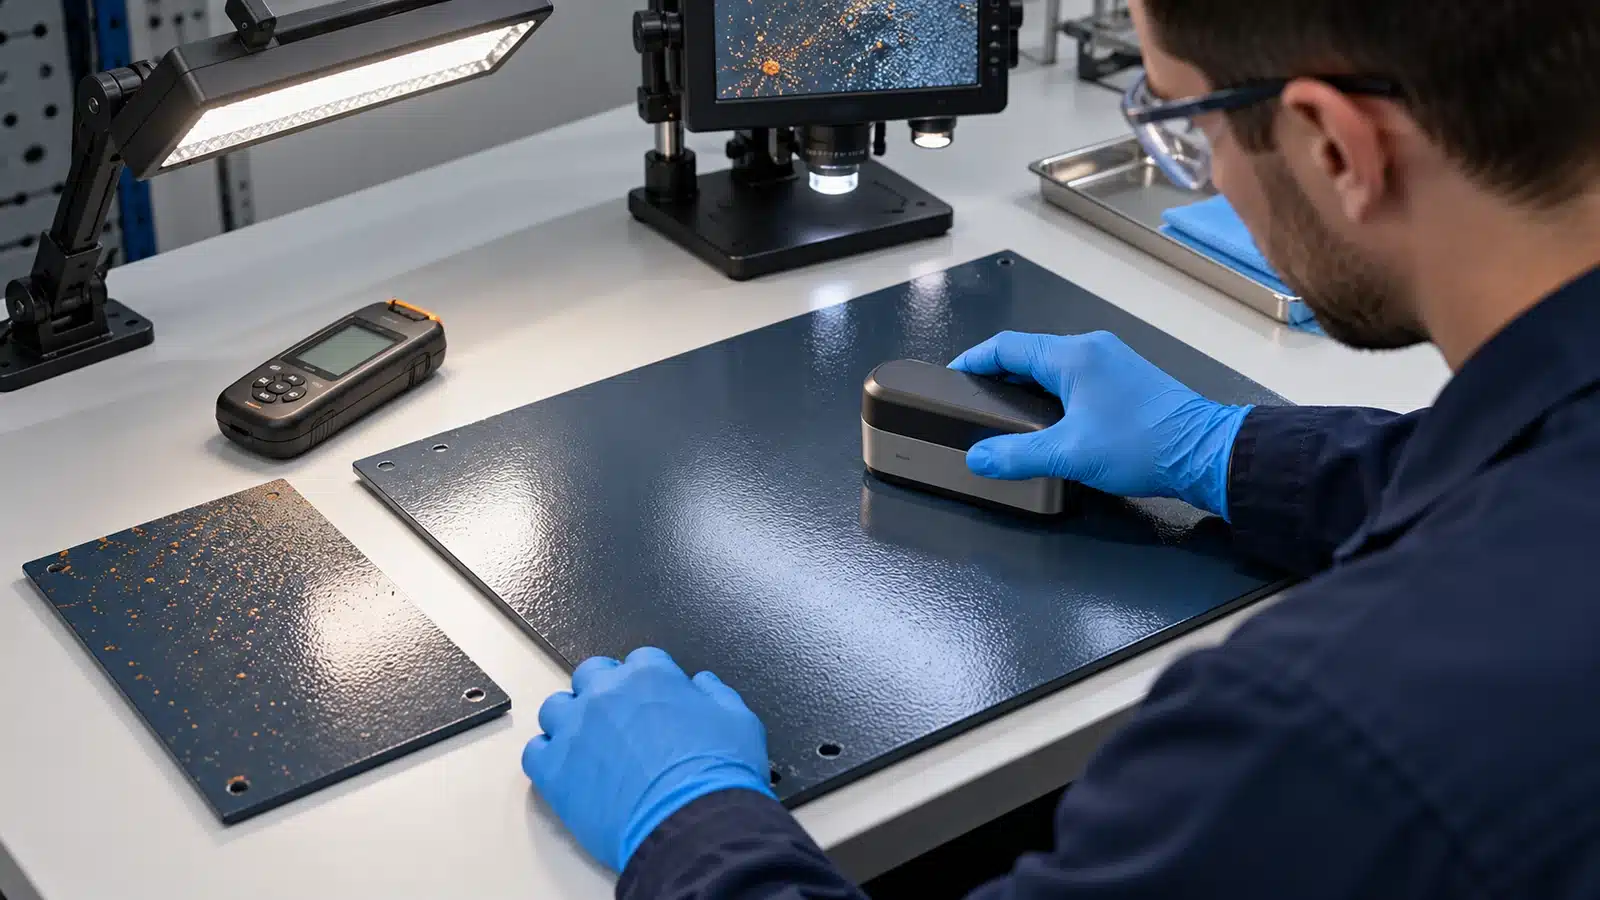
Verification should answer two separate questions: is the overspray gone, and is the required original surface still acceptable? Use the same lighting, viewing geometry, cleaning state, and measurement locations before and after the trial. Keep an untreated reference whenever possible.
Check Residual Particles, Color, Gloss and Surface Texture
Begin with a clean, dry visual inspection under diffuse light and a directional light that reveals raised particles, haze, scratches, gloss patches, and texture changes. View the area straight on and at shallow angles. On suitable smooth surfaces, a clean glove or protected tactile check may reveal remaining raised particles, but do not rub an unknown residue with bare skin.
Photographs are useful only when exposure, white balance, distance, and angle are controlled. A bright “after” photograph can hide haze or color change. For repeated production work, a simple inspection fixture and reference panel are more reliable than unstructured phone images.
If appearance is specified numerically, use a suitable method and agree the tolerance before the trial. ASTM D523 covers specular-gloss measurement at defined geometries, while ASTM D2244 covers calculation of color differences from measured color coordinates. Use each method within its stated measurement scope: D523 addresses gloss measurement on nonmetallic specimens, which can include a retained coating over metal, while D2244 calculates color differences from instrumentally measured coordinates for opaque specimens. Neither standard supplies a universal pass limit for overspray removal. Instrument geometry, surface texture, measurement repeatability, and the customer specification determine whether the result is meaningful.
When Coating Thickness or Other Measurements Are Necessary
Thickness measurement is useful when loss of the retained coating would create a functional or contractual problem and the instrument is suitable for the substrate and film. Measure repeatable locations before and after cleaning and account for instrument uncertainty and surface roughness.
A total-thickness gauge does not necessarily separate clear coat, color coat, primer, and previous repair layers. DeFelsko’s automotive guidance explains that gauge readings and layer interpretation depend on the substrate and instrument capability. Therefore, an unchanged total reading does not prove that the top layer is undisturbed, and a small difference should not be interpreted without repeatability and uncertainty.
Other checks may matter more than thickness: microscopy for residue or pitting, adhesion testing on sacrificial coupons, water-break or surface-energy methods before bonding, roughness measurement on precision surfaces, electrical continuity, dimensional inspection, or a downstream coating-adhesion trial. These methods answer different questions: a water-break or surface-energy check does not by itself prove bond strength or identify every contamination type. Select the check from the part’s next process and failure consequence rather than adding measurements that do not answer the acceptance question.
When Should You Stop Cleaning and Consider Local Refinishing?
Stop when further removal is more likely to enlarge damage than to improve the accepted result. Local refinishing is not a failure of the cleaning plan; it is the controlled option when the original coating cannot be preserved or was already defective.
Damage Warning Signs and Repair Decisions
Stop the trial if the original finish becomes tacky, soft, swollen, whitened, discolored, glossy in a matte area, dull in a glossy area, scratched, pitted, blistered, lifted at an edge, or thin enough to expose primer or substrate. For laser work, also stop for heat tint, melting, reflow, roughness change, smoke behavior outside the extraction plan, or unstable removal from pass to pass.
Before deciding on repair, determine whether the observed defect came from the overspray event, pre-existing coating failure, or the removal method. If the underlying coating has poor adhesion, cracking, corrosion creep, or solvent attack, continuing to clean may create an irregular repair boundary. A defined local strip-and-refinish process can produce a more predictable finish.
Coordinate repair with the coating system. The preparation, primer, color, cure, blend boundary, and inspection need to match the part’s service and appearance requirements. For background on the differences between powder coating and liquid painting, use the coating-system requirements rather than assuming the two finishes accept the same repair route.
How to Prevent Overspray During Future Work
Prevention begins with controlling the spray zone and air movement, not only covering the nearest visible face. Review booth or enclosure capture, spray-gun setup, pressure, nozzle condition, part orientation, masking, fixture shadowing, exhaust balance, and the path by which fine droplets can reach adjacent work.
Use masking materials compatible with the finish and cure temperature. Protect openings, precision faces, labels, and seals without trapping solvent or adhesive residue. Separate spraying from finished-part staging, and inspect protection before each batch. When overspray occurs, identify the coating and respond before it cures if the retained finish’s approved process allows it.
Record recurring events by location, coating, shift, and process condition. A pattern concentrated on one side of a fixture may indicate airflow or orientation; random contamination across storage racks may point to zoning or housekeeping. Preventive action should address that path rather than making removal a routine production step.
Frequently Asked Questions
Can Fresh Overspray Be Wiped Off Before It Cures?
Sometimes, but wiping is not automatically safe. First confirm that the original coating is cured and compatible with the approved cleaner. Lift or blot the deposit rather than spreading it, use clean soft material, and stop if color transfers or the finish softens. For some powder coatings, supplier guidance specifically favors early removal of paint splashes before they dry. Follow the actual coating and paint instructions.
Can Pressure Washing Remove Paint Overspray from Metal?
Pressure washing may remove loose, poorly adhered fresh material from a robust surface, but it is unreliable for cured paint and can drive water into seams, lift weak coating edges, damage labels, or spread contamination. Use it only when the part, coating, seals, drainage, pressure, stand-off distance, and waste controls have been approved. It does not replace a compatibility test or dry inspection.
Can You Use Acetone on Painted Metal?
Do not assume so. Acetone may attack or soften some paints, clear coats, plastics, adhesives, and powder coatings. The Interpon D guidance cited here excludes ketone-containing cleaners for its stated coating scope. Check the original coating supplier’s current instructions and the acetone SDS, then perform a controlled, inconspicuous test only if the coating system permits it. A generic “quick wipe” is not a compatibility standard.
Can You Remove Overspray from Powder-Coated Metal?
Often, but the method must follow the specific powder-coating supplier’s limits. Start with approved mild cleaning and address paint splashes early where possible. Avoid transferring automotive polishing or strong-solvent advice to a powder-coated part without approval. If the overspray has cured or the powder film is weathered, textured, or damaged, use a representative trial and compare the dry result for color, gloss, texture, and coating integrity.
Technical References
- AkzoNobel Powder Coatings. Interpon Guidance Note 6: Cleaning and Maintenance of Powder Coated Architectural Components. Issue 3, September 2022. https://powdercoatings.brand.akzonobel.com/m/3ff4ff8c9f64cbc7/original/Interpon-Guidance-Note-6-Cleaning-and-Maintenance-EN.pdf
- 3M Automotive Aftermarket Division. 3M 38070 Perfect-it III Cleaner Clay Technical Data Sheet. Effective August 19, 2020. https://multimedia.3m.com/mws/media/1399621O/3m-perfect-it-iii-cleaner-clay-38070.pdf
- U.S. Occupational Safety and Health Administration. Solvents: Overview. Accessed October 20, 2026. https://www.osha.gov/solvents
- U.S. Environmental Protection Agency. Risk Management for Methylene Chloride. Current page accessed October 20, 2026. https://www.epa.gov/assessing-and-managing-chemicals-under-tsca/risk-management-methylene-chloride
- Wang, X.; Ding, Y.; Chen, Q.; Li, H.; Wang, L.; Wang, M. “Laser Cleaning Process for Low-Pressure Turbine Blade Paint Removal with Remelting Suppression.” Coatings 15, no. 9 (2025): 1054. https://doi.org/10.3390/coatings15091054
- cleanLASER. Selective Paint Removal. Manufacturer application description, accessed October 20, 2026. https://www.cleanlaser.de/en/applications/application-fields/paint-removal-and-decoating/selective-paint-removal/
- U.S. Occupational Safety and Health Administration. Laser Hazards: Overview. Accessed October 20, 2026. https://www.osha.gov/laser-hazards
- ASTM International. ASTM D523-25: Standard Test Method for Specular Gloss. https://store.astm.org/standards/d523
- ASTM International. ASTM D2244-25: Standard Practice for Calculation of Color Tolerances and Color Differences from Instrumentally Measured Color Coordinates. https://store.astm.org/d2244-25.html
- DeFelsko. How to Use Paint Thickness Gauges for Better Automotive Detailing. Accessed October 20, 2026. https://www.defelsko.com/resources/how-to-use-paint-thickness-gauges-for-better-automotive-detailing