

How to Remove Weld Spatter from Metal: Methods & Prevention
To remove weld spatter, start with the least aggressive method that can detach the unwanted metal: use an appropriate scraper or chipping tool for lightly attached droplets, then controlled local abrasion for deposits that remain firmly attached. Clear loose debris before assessing the surface again. The job is complete when the required spatter has been removed and the part still meets its requirements for thickness, weld shape, finish and subsequent processing.
That second condition matters. A grinder can remove a raised bead and also cut a hollow into the plate beneath it. A surface can look brighter while still needing separate oxide removal or preparation for coating. Choosing a cleanup method therefore starts with two questions: what is attached to the part, and what must remain unchanged?
This guide explains how to make that choice, carry out removal in stages, and reduce the cleanup needed on the next batch.
Why some weld spatter comes off easily—and some does not
Weld spatter consists of metal droplets expelled during welding. Once deposited, those droplets are not all equally easy to detach. The useful distinction is not simply large versus small. It is whether the droplet will release at its attachment before the removal tool begins to alter the surrounding plate, weld toe or finished surface. [1]
Use the first controlled tool contact as a diagnostic observation rather than trying to infer attachment strength from shape alone. If the droplet moves or releases while the adjacent surface remains acceptable, a detachment method is working selectively. If the deposit stays in place while the plate, finish or weld feature begins to mark, the operation is affecting what must be preserved before it has solved the removal problem.
A small trial area therefore provides a better starting point than appearance alone. If a correctly used scraper releases a droplet cleanly, the job is detachment; grinding a wide area would add surface change without solving a remaining attachment problem. If the bead remains while the tool leaves marks in the plate, the operation is becoming less selective. Reassess access, tool choice and the permitted material removal instead of treating more force as the automatic next step.
Also identify the deposit before selecting a method. Metallic spatter is different from slag produced by flux-based welding processes, and both are different from heat tint or oxide discoloration. The intended weld bead and its transition into the plate are not cleanup waste. Confusing these features can turn surface finishing into an unplanned weld alteration.
Which weld spatter removal method should you use?
Choose by the required action, rather than by the most powerful tool available. Detaching a droplet, cutting down an attached projection and blending an abrasive mark are different jobs. A method is suitable only when it changes the unwanted deposit faster than it changes the surface that must be preserved. [2]
Start with the question the tool must answer. If the droplet can release at its interface, use a controlled detachment method and inspect what is underneath. If it will not release, decide whether local stock removal is permitted and how the remaining profile will be checked. Blending belongs after the projection has been removed; it should not be used to hide uncertainty about a hollow, rounded edge or changed weld contour.
| Method or operation | Useful starting condition | Main surface tradeoff | Reassess when |
|---|---|---|---|
| Scraping or controlled chipping | Accessible droplets that release without unacceptable marking | Local tool marks are possible; access controls where force is applied | The plate is marking but the deposit remains |
| Suitable wire brushing | Clearing loose particles and assessing what remains after detachment | Brushing is not a substitute for controlled removal of firmly attached metal | More pressure produces wear or marking without useful removal |
| Local abrasive stock removal | Firmly attached projections where material removal is permitted | The abrasive can cut surrounding metal as well as the projection | A depression, altered edge or weld-shape change begins to develop |
| Blending and finishing | Spatter is removed, but the remaining marks need an approved finish | A larger area is affected; appearance can conceal a local hollow | The finish looks uniform but dimensions or profile remain uncertain |
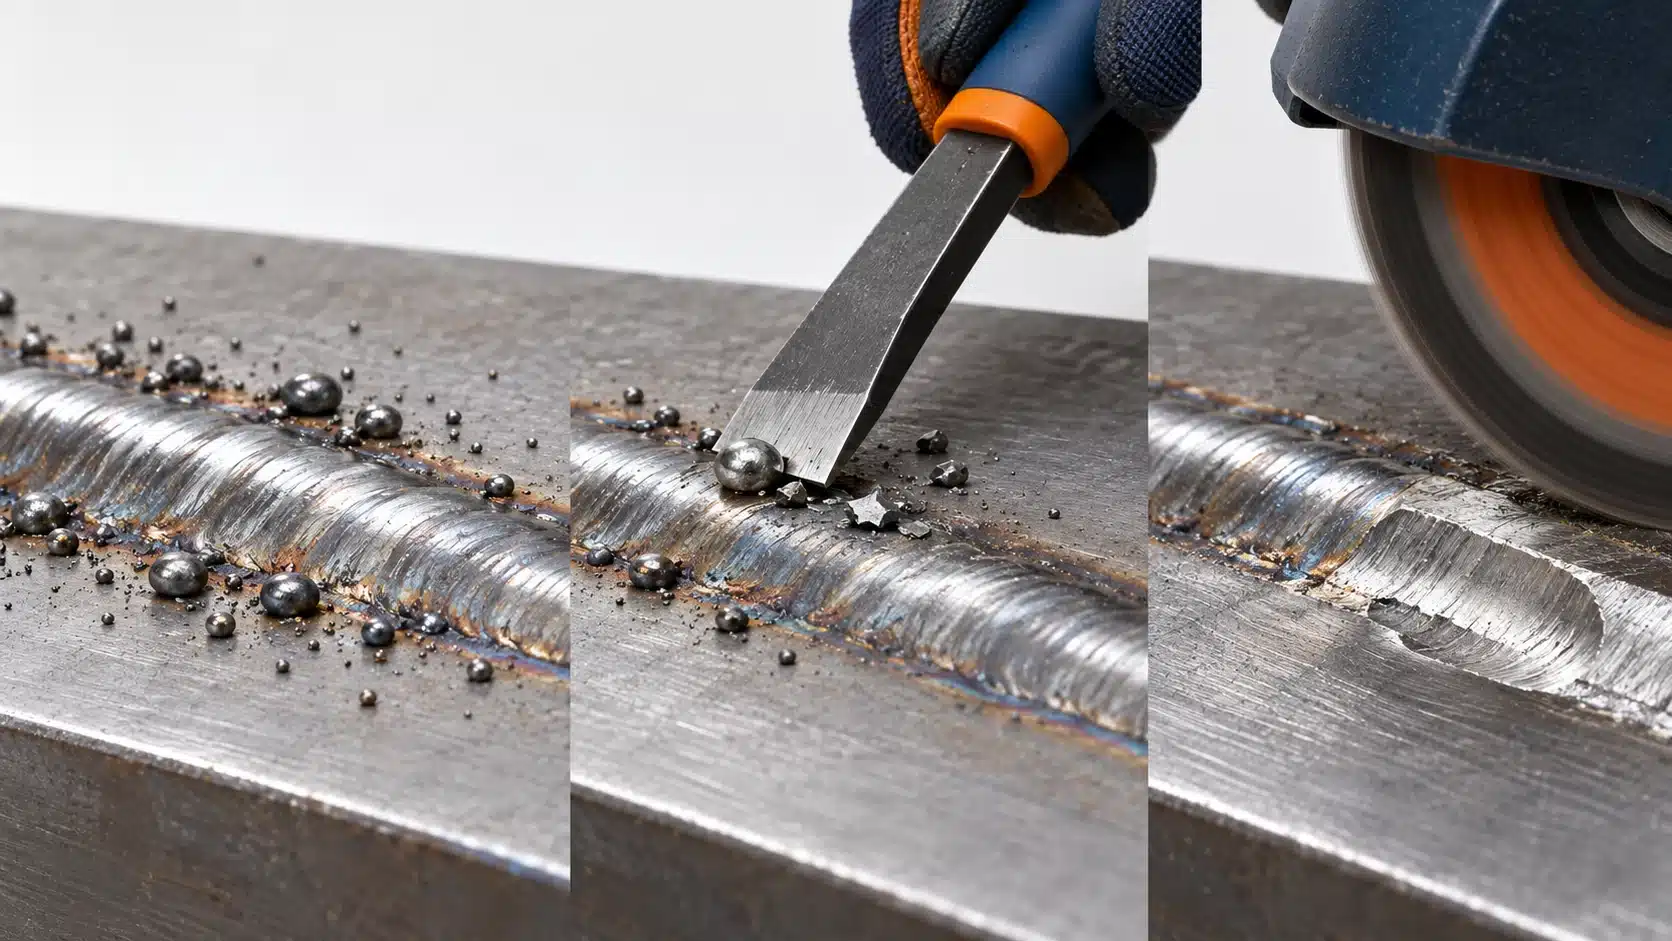
For an illustrative comparison, consider a painted steel bracket and a visible brushed-stainless panel. Both may require raised droplets to be removed. The bracket also needs the surface condition specified by its coating system, while the panel may require preservation of a directional finish and contamination controls. One cleanup sequence should not be copied to the other merely because both parts contain weld spatter. These are planning examples, not reported production trials.
How to remove weld spatter step by step

Prepare the part and define what must be preserved
Identify the alloy, any existing coating, the required final finish and the next operation. Check the drawing and applicable welding or finishing instructions for areas where grinding is restricted. Mark features that need protection, such as sealing faces, edges and the intended weld contour. Establish who will decide whether an unexpected gouge or weld alteration is acceptable before cleanup begins.
Secure the work and arrange lighting so a raised bead can be distinguished from a depression. Select an attachment suitable for the material and the grinder: its rating, mounting arrangement, condition and required guard must all match the equipment instructions. Use the attachment maker's instructions for contact angle and operation; there is no single angle or speed that suits every wheel and brush. Eye and face protection, exposure controls and the work area must address the actual debris and material involved. [3]
Identify coatings and cleaning residues before generating dust or returning the part to welding. CCOHS warns that chlorinated solvent vapours exposed to welding ultraviolet radiation can form hazardous decomposition products. Choose cleaning chemistry through the approved process and safety information, with the required controls, rather than using a convenient solvent beside active welding. [4]
Remove lightly attached droplets and clear loose debris
Begin on a representative accessible area with a tool intended for the task. Direct the operation at the unwanted droplet, not at the weld toe or a finished edge. Inspect the contact area after removal: the useful result is a released bead without unacceptable damage underneath it.
Clear detached particles before deciding how much work remains. A suitable brush can help expose residual projections, but pressing harder is not a reliable way to convert brushing into stock removal. Excessive pressure on a powered wire brush can break wires and increase heat; follow its operating instructions. [3] If beads remain firmly attached, change the removal approach rather than repeatedly scrubbing the whole surface.
Remove firmly attached spatter with controlled local abrasion
Where the part specification permits it, use a material-compatible abrasive to reduce the remaining projection locally. Make short, controlled interventions with inspection between them. As the projection becomes lower, the margin between removing unwanted metal and cutting the surrounding surface narrows. Continuing until the whole area looks uniformly bright is a poor endpoint.
Stop and reassess when the bright worked area keeps spreading but the projection is no longer becoming meaningfully lower, when a surrounding edge begins to round, or when inspection can no longer distinguish the original surface from a developing hollow. At that point, further abrasion may improve appearance while reducing the chance that the part will meet its geometric or finish requirements.
Pay particular attention to deposits close to a weld toe, corner or thin section. If the tool cannot reach the projection without changing a protected feature, the access problem needs a different tool or an approved process decision. It should not be solved by accepting unplanned material loss.
For a repeated operation, retain a representative starting sample and record the attachment, tool settings and inspection method used. This makes the sequence reproducible without pretending that one grit or pressure setting works for every alloy and geometry.
Blend the marks without hiding material loss
Blending is a finishing step after removal, not a remedy for every removal error. An abrasive can make the scratches around a gouge less obvious by extending the worked area, but that does not restore the missing metal. Check the local shape before refining the appearance.
If blending is permitted, select the finish according to the part's next use: a specified visual pattern, a mating requirement or a coating preparation requirement. Avoid chasing a mirror-like appearance where it is neither required nor appropriate. Where a depression or thickness change is suspected, use the inspection required by the drawing or quality plan before continuing.
Adjust the method for stainless steel, aluminum and galvanized steel
Stainless steel: protect the finish and avoid contamination
Keep stainless finishing tools and abrasives clean and controlled so they do not introduce contamination from previous carbon-steel work. For austenitic stainless fabrication, dedicated uncontaminated abrasives and control of heating during finishing are important considerations. On a visible surface, trial the removal and blending sequence against the required finish before working across the whole panel. [5]
Treat the remaining discoloration as a separate question. Removing metallic droplets does not automatically address the oxide or the material condition underneath heat tint. Pickling can remove oxide scale and the chromium-depleted layer; passivation aimed at light iron contamination is a different treatment and is not a substitute for removing heavy oxide. The appropriate treatment depends on the grade, service and approved process. A bright-looking surface alone is not the acceptance criterion. [5]
Aluminum and thin sheet: control abrasive loading and distortion
On aluminum, removed metal can accumulate on the abrasive and cover its cutting points. As cutting becomes less effective, an operator may push harder; that can increase friction and heat and worsen loading. If an attachment stops cutting as intended, inspect it and follow the manufacturer's replacement or maintenance instructions instead of forcing it through the job. Choose an abrasive explicitly suitable for the material. [6]
For thin sheet, make flatness and remaining thickness explicit trial checks. The practical concern is not only whether the bead disappears, but whether the cleanup leaves a depression, visible waviness or another change outside the part requirements. Support the work appropriately, use local controlled removal, and inspect before expanding the operation. A sequence accepted on a thick bracket is not automatically qualified for a thin panel.
Galvanized steel: plan for the zinc coating as well as the spatter
Distinguish between a fabrication that will be hot-dip galvanized after welding and a part that already has a zinc coating. For the first, removal and any anti-spatter product must fit the galvanizer's preparation requirements. For the second, include the surrounding coating in the inspection: removing a projection is not the end of the job if the operation has exposed steel or disturbed the coating.
Recognized repair approaches for damaged hot-dip galvanized areas include zinc-rich paint, zinc solder and zinc spraying. The selected route and acceptance requirements must come from the applicable project specification and responsible coating function. This is not permission to treat any zinc aerosol as equivalent to the original coating. [7]
Where chemicals, blasting and laser cleaning fit
Separate surface-layer cleaning from metal-droplet removal
A treatment that removes oxide, oil or discoloration answers a different question from one that removes an attached metal projection. For example, stainless pickling and passivation have defined surface-treatment purposes; their availability does not establish them as general substitutes for spatter removal. Select the operation by the unwanted material and the required endpoint, not by the broad label “weld cleaning.”
Apply the same distinction when evaluating blasting or needle tools. Do not assume that a surface preparation method will remove every firmly attached bead just because the surrounding surface becomes cleaner. In a representative trial, inspect residual projections and the surrounding finish separately, especially where local material removal or texture changes would be unacceptable. Broader claims about a specific blasting or needle-scaling process need evidence for that process and part.
What a laser-cleaning trial must demonstrate
Laser cleaning depends on how the unwanted material and the substrate respond to delivered energy. Removing a thin surface layer and removing an attached metal droplet are therefore different demonstrations. A video showing heat tint disappearing does not, by itself, establish that raised spatter can be removed while meeting the part's dimensional and surface requirements. This is a reason to ask for a relevant trial, not a conclusion that laser removal is impossible. [8]
Use actual or representative spattered parts, including difficult locations, and agree on what will be inspected before the trial. Record the starting condition, equipment configuration, processing sequence and any additional mechanical finishing. Then assess both the unwanted projection and the surrounding base metal or weld. If a subsequent coating is required, include the preparation and qualification steps that its specification calls for. A successful-looking photograph should not replace those agreed checks.

The trial also needs controls for the actual laser system and work area, including direct and reflected beam exposure and non-beam hazards such as process emissions. Appropriate enclosure, access control, extraction and protective measures must follow the equipment assessment and applicable requirements; protective eyewear alone is not a complete operating plan. [9]
Oceanplayer's laser weld-cleaning information describes oxide and heat-tint cleaning. For a spatter-removal enquiry, provide the alloy, weld process, photographs, difficult features and acceptance requirements, and ask specifically what a trial can establish for attached metal droplets. No fused-spatter removal rate or guaranteed outcome follows from the general weld-cleaning description.
Check the cleaned part before coating or release
Inspect after loose debris has been cleared, so remaining projections and removal marks can be seen. A useful acceptance plan separates cleanliness, geometry, finish and weld inspection rather than combining them into a single “looks good” decision. The following is a planning checklist; actual limits and release authority belong to the drawing, specification and responsible quality function.
| Finding or question | Why it matters | Required decision or follow-up |
|---|---|---|
| Raised droplets remain in a required clean area | The removal endpoint has not been met | Assess access and an approved further removal method |
| A hollow, gouge or changed edge is visible | Uniform appearance does not establish acceptable geometry | Check the relevant dimension or profile and obtain a disposition |
| The weld toe or intended weld contour has changed | Cleanup may have altered a controlled weld feature | Refer to the welding and inspection requirements before release |
| Discoloration, residue or damaged coating remains | Spatter removal and surface preparation are separate operations | Apply the material-specific cleaning or coating plan |
| A crack-like indication or other suspicious feature is found | Cosmetic finishing cannot resolve the acceptance question | Stop local finishing and refer for the required inspection |
| Surface checks pass | Cleanup has met only the checks actually performed | Complete the specified downstream and weld inspections |
Keep a short record of the inspected area, method, relevant measurements or photographs, and disposition. For a first-off sample, include both an overall view and close views of the difficult features. If the method will be repeated in production, record enough process detail to distinguish the accepted sequence from a later operator adjustment.
How to prevent weld spatter and reduce repeat cleanup
Reduce spatter generation by checking the welding process
When cleanup repeatedly exceeds expectations, investigate the welding operation before simply specifying a more aggressive removal tool. Check the setup against the applicable welding procedure and equipment instructions, including the selected program or parameters, wire and consumable compatibility, wire feeding, gas delivery and the condition of relevant wear parts. These checks help identify a process problem that finishing would otherwise repeat on every part. [10]
Avoid turning this into a universal instruction to raise or lower current, voltage or gas flow. The appropriate correction depends on the welding process and setup. Change one identified cause within the approved procedure, then assess weld quality as well as the amount of cleanup. For laser-welding-specific causes, see Oceanplayer's separate guide to avoiding spatter during laser welding.
Reduce adhesion without creating a downstream coating problem
Anti-spatter products address how deposits adhere to protected surfaces; they do not replace correction of an unsuitable welding setup. Their usefulness also has to be assessed beyond the immediate welding operation. A film that makes droplets easier to release still needs to be compatible with subsequent cleaning, painting or galvanizing.
For painted work, confirm the actual product's instructions, residue-removal requirements and compatibility with the intended pretreatment and coating system. “Water-based” or “silicone-free” is not a complete process qualification. [11] For hot-dip galvanizing, some films can survive pretreatment and interfere with coating formation, so obtain the galvanizer's agreement before introducing the product. [12]
The strongest cleanup plan combines a stable welding process, a removal method matched to the part, and a defined inspection endpoint. If you are evaluating laser cleaning as one part of that sequence, contact Oceanplayer with representative part information and the required result so the discussion starts with the application rather than a power rating.
Frequently asked questions
Should spatter be removed between weld passes?
Follow the applicable welding procedure. In flux-based processes, inter-run slag removal is a distinct requirement because material left between runs can contribute to slag inclusions. Do not treat that operation as interchangeable with final cosmetic spatter cleanup. Remove interfering deposits and perform any interpass cleaning or grinding required by the procedure without altering the intended weld geometry on the basis of a general blog instruction. [13]
How should you compare cleanup methods for repeated production?
Compare them at the same accepted endpoint on representative parts. Include preparation, handling, removal, blending, residue cleanup, inspection and any rework, along with relevant consumable use. A method that removes the bead quickly but leaves a larger finishing or repair operation is not necessarily the better production route.
Record where each method succeeds and where access, finish or geometry prevents acceptance. Use the results to define an approved sequence and its checks, rather than assuming the fastest individual demonstration will produce the lowest cost per accepted part. This is a recommended comparison method, not a claim of measured savings.
Technical References
The references below support the stated mechanisms and process boundaries. They do not establish a universal removal allowance, an Oceanplayer performance result or acceptance criteria for a particular component.
- TWI — What Is Weld Spatter?. Formation of weld spatter and established cleanup approaches.
- Norton — Choosing the Right Abrasive Product for Welding and Metal Fabrication. The distinction between stock removal, blending and final finishing.
- CCOHS — Powered Hand Tools: Use of Grinder Attachments. Attachment compatibility, inspection, guarding and operating precautions.
- CCOHS — Welding: Fumes and Gases. Welding exposure controls and the chlorinated-solvent hazard discussed in this article.
- International Molybdenum Association — Practical Guidelines for the Fabrication of Austenitic Stainless Steels, 2nd ed., 2020, §§15.2.3–15.2.7. Stainless finishing, contamination control, pickling and passivation.
- Norton — Aluminum Metal Fabrication Drives Abrasive Developments. Aluminum loading and its effect on abrasive cutting.
- American Galvanizers Association — Repairing Damaged or Uncoated Areas of Hot-Dip Galvanized Coatings. Recognized repair-route overview; the project specification still governs selection and acceptance.
- IPG Photonics — What Is Laser Cleaning?. General explanation of how unwanted material and the substrate respond to delivered laser energy.
- Oregon OSHA — Lasers: Safe Work Practices. Beam and non-beam hazard overview; it is not presented as a substitute for the applicable local requirements or equipment assessment.
- Fronius — Welding FAQ. Process-specific troubleshooting considerations for recurring spatter.
- ABICOR BINZEL — Which Anti-Spatter Is Right for Me?. Formulation and downstream painting considerations; compatibility remains product- and process-specific.
- American Galvanizers Association — What Welding Sprays Are Suitable for Galvanizing?. Anti-spatter film compatibility with galvanizing pretreatment.
- TWI — Defects/Imperfections in Welds: Slag Inclusions. Inter-run cleaning and slag-inclusion prevention; this article does not adopt any acceptance limit from that source.