

Sandblasting Alternatives for Metal: Which Method Fits Your Job?
Power tools, laser cleaning, chemical treatment, dry ice and pure waterjetting can replace particular metal-cleaning tasks performed by sandblasting. Wet or contained abrasive blasting may also solve the problem if the main concern is airborne dust or loose media.
The right choice depends on what must come off, what must remain, and what the next operation needs from the surface. A process that removes a coating is not automatically a complete replacement for a process that also produces the required surface texture.
Start with the finished part rather than the machine. A reusable mold face, a small steel repair and a large structure awaiting repainting may all need cleaning, but they do not have the same acceptable endpoint. Comparing their requirements makes the differences between the available methods much easier to use.
Define the Job Before Choosing a Sandblasting Alternative
First identify the reason for changing the existing process. Is the problem the abrasive material, dust containment, access, cleanup, or an unacceptable change to the metal surface? Those questions lead to different shortlists. Replacing the blasting medium or enclosing the operation changes how abrasive cleaning is delivered; it does not necessarily remove abrasive impact from the process.
This distinction also keeps the comparison fair. A laser treatment should not receive credit for avoiding grit if the job still needs a separate profiling operation afterward. Equally, a wet abrasive route should not be rejected simply because it retains particles if it meets the actual surface requirement and the reason for changing was dust control.
Remove a layer, preserve a finish, or create a profile?
These are three different tasks. Removing a layer exposes the surface beneath it. Preserving a finish means keeping features that matter to the part, such as a working face or an existing coating that must remain. Creating a profile means producing the surface texture required by the next process, rather than merely making the metal look clean.
Write the requirement in that order: unwanted material, features to retain, and accepted final condition. Include the relevant coating or process specification. This prevents a bright, visually attractive test area from becoming the only measure of success.
The following comparison is a starting point for shortlisting. It does not assign universal cleaning rates or declare any method suitable for every metal.
| Process | Action and candidate task | Surface consequence | Main check |
|---|---|---|---|
| Power tools | Local brushing, grinding or impact for accessible repairs | Texture depends on the tool and contact | Remaining material, edge condition and required profile |
| Laser cleaning | Directed optical energy for accessible surface layers | Exposure affects the layer and underlying surface | Removal window, retained finish and beam access |
| Chemical treatment | A selected formulation removes a compatible target layer | Treatment residues may need further removal | Substrate and retained-layer compatibility; complete cleanup |
| Dry ice | Pellet action for suitable deposits; limited light-oxidation applications | Media sublime; do not assume an anchor profile | Actual deposit removal and remaining debris |
| Pure waterjetting | Water removes old surface material | Can reveal an existing profile rather than create one | Revealed texture, flash rust and coating acceptance |
| Wet or contained abrasive blasting | Abrasive action with modified delivery or collection | Media can still affect texture and leave residues | Media choice, containment and final surface condition |
The key dividing line is whether the job needs removal alone or removal plus a specified surface change. The next sections explain why that distinction changes the shortlist.
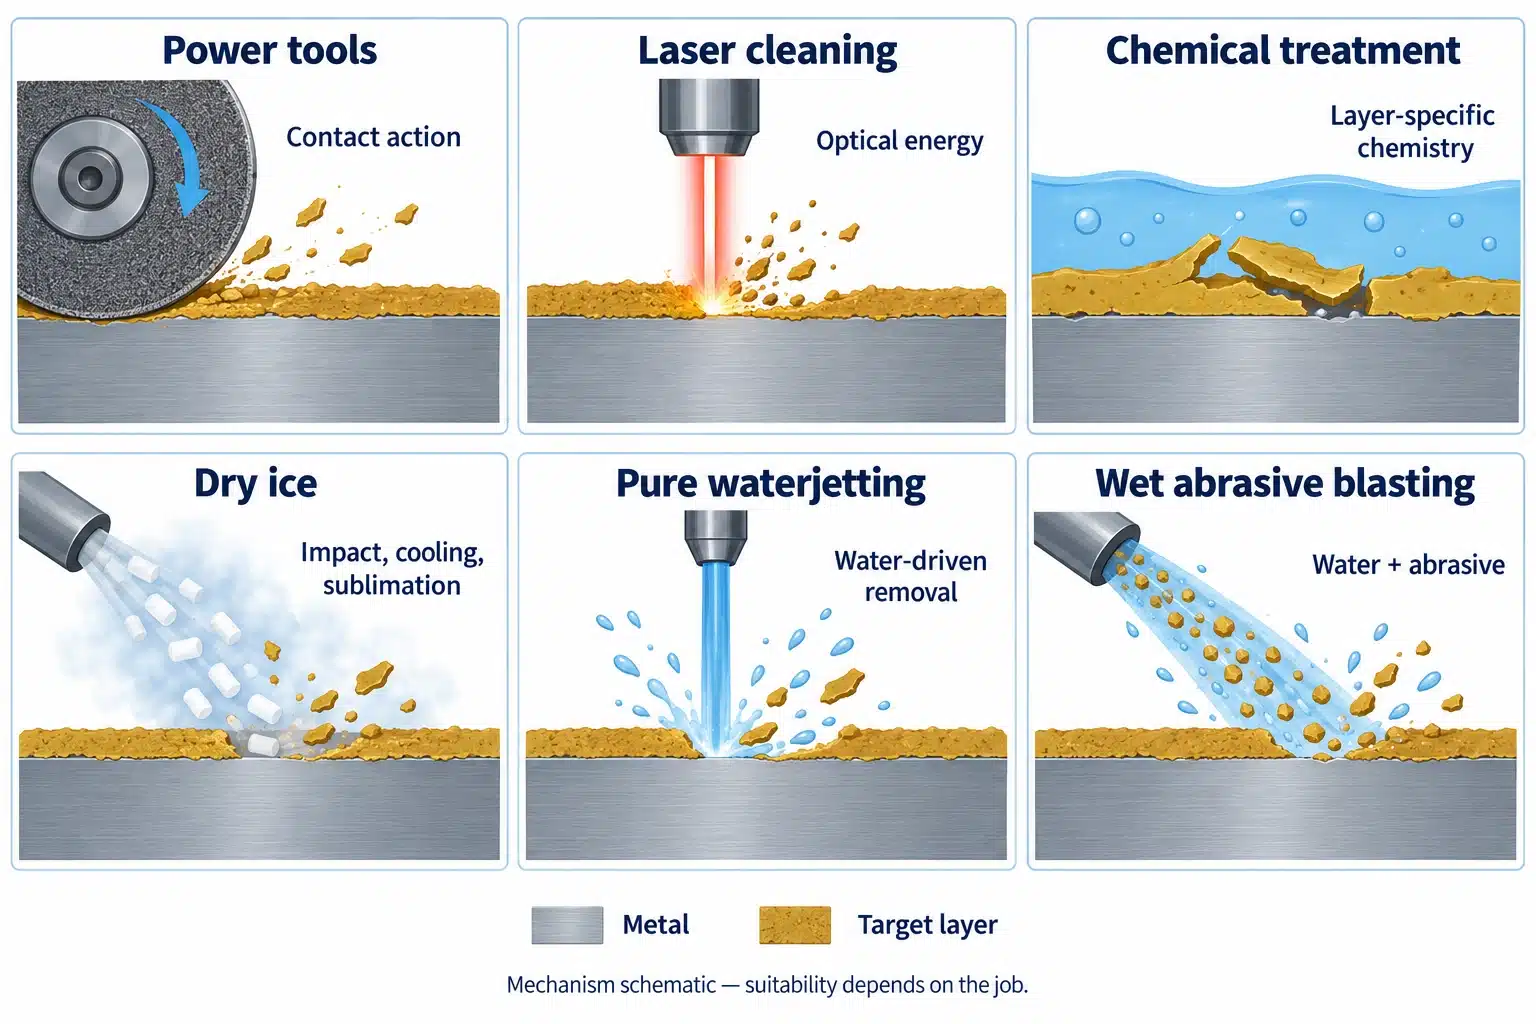
Power-Tool Cleaning for Local Repairs
Power tools apply their action where the tool contacts the workpiece. A brush, grinding disc and impact tool do not act in the same way: brushing works through bristle contact, grinding removes material with an abrasive surface, and impact tools repeatedly strike the surface. This makes tool selection part of the process specification, rather than a minor accessory choice.
For a localized repair, direct contact can let the operator work around a defined area. Access becomes the limiting question: can the effective part of the tool reach the bottom of a recess, the edge of a repair or the area beside a fitting? A successful flat test patch does not answer those questions. Compare the actual difficult features before assuming that a small tool is automatically a flexible solution.
Why a profiling bristle tool differs from a wire brush
A purpose-designed profiling bristle tool uses a particular impact-and-retraction action. It should not be treated as equivalent to an ordinary rotating wire brush simply because both have bristles. The distinction matters when the required result includes a surface profile, not just removal of loose material.
For a trial, specify the tool type and inspect the result under the intended working conditions. If a profiling tool is proposed, measure the parameter required by the coating specification using an appropriate method. If the part has an edge or retained finish, include that feature in the trial and inspect it separately. A tool that produces an acceptable repair area can still be unsuitable for an adjacent feature that must remain unchanged.
Laser Cleaning for Selective Surface Removal
Laser cleaning delivers optical energy instead of driving abrasive particles against the metal. When the unwanted layer absorbs enough energy, material can vaporize or detach from the surface: this removal is called ablation. The practical opportunity is to find exposure conditions that remove the layer before the underlying surface changes beyond its acceptable limit. That opportunity depends on the particular layer and substrate; it is not a guarantee that every coating has a harmless removal setting. Scanning moves the small interaction area across the part.
This makes laser cleaning a candidate when local treatment and avoiding added grit are useful. It does not establish that the metal will retain every original property or that a coating-ready profile will be created. The required result must still be demonstrated on the actual layer and part.
How local exposure changes the cleaning result
Machine power alone does not describe what a small area experiences. Beam delivery, spot size and scanning determine how the available energy is distributed; in pulsed operation, pulse conditions and overlap also matter. Changing those conditions can change the balance between incomplete layer removal and unwanted alteration of the surface underneath.
Both outcomes matter: removal and preservation. Insufficient exposure leaves material behind; increasing exposure is useful only while the retained surface still meets its requirement. The trial record should therefore connect the observed result to the beam configuration and scanning conditions, so a successful patch can be meaningfully repeated.
When layer thickness and access limit the process
Absorption, layer thickness and optical access affect feasibility. The beam must reach the area being treated; a visible outer face and a shadowed recess are different tasks. A result on a thin deposit does not establish the time or exposure required for a thicker coating.
Before selecting a configuration, include the representative coating range and the hardest-to-reach feature in the trial. If repositioning or repeated treatment is required, include it in the complete cycle. Do not turn a supplier's thickness example into a universal cutoff, or infer that a higher-power machine will solve an access problem.
Laser hazards also remain part of the decision. Class 4 equipment presents direct and reflected-beam eye and skin hazards and can present a fire hazard. The trial needs controls appropriate to the actual machine, work area, reflections and removed material. Avoiding abrasive media does not eliminate the need to assess emissions and collect the material removed.
Chemical Stripping and Derusting for Compatible Parts
Chemical treatment changes the unwanted layer so that it can be removed without relying on grit impact. In solvent stripping, a compatible solvent can penetrate a polymer coating and cause it to swell. The swollen film becomes easier to separate and remove; it does not necessarily dissolve completely or disappear into the bath. Research on solvent–polyurethane interactions demonstrates this swelling mechanism, but does not establish a recipe for every industrial paint or recommend a particular solvent for current use.
Derusting asks a different chemical question. Some formulations use chelation: molecules bind iron from the corrosion products and hold it in solution. A chelating rust remover is therefore acting on the oxide rather than mechanically cutting it away. This is one formulation-specific route, not the mechanism of every rust-removal product. Removing oil, loosening paint and treating rust can require different chemistry even when all three are present on the same component.
The practical difference from blasting is that contact with the correct chemistry must do the work before cleanup can finish it. A liquid route can be worth investigating where a tool or beam cannot directly reach, provided the formulation can reach the layer and subsequently be drained and removed. It is a poor choice when the necessary contact or cleanup cannot be achieved, or when a finish that must remain is also vulnerable to the selected treatment.
Contact time matters because the chemistry needs access to the target layer. A formulation that has not penetrated or contacted the contamination cannot be judged by the appearance of the surrounding clean metal. The useful compatibility information therefore names the substrate, retained finish and target layer, rather than simply calling the product a metal cleaner. Its immersion-and-rinse sequence remains product-specific.
Match the chemistry to the layer—and plan the rinse
The treatment is not finished merely when the unwanted layer has loosened. Include removal of the detached material and any specified rinsing and drying. A part that can be immersed may still be a poor candidate if its geometry makes the required cleanup difficult. Consider how the treatment and rinse will reach, leave and be checked in recesses or assemblies.
Use the formulation's approved conditions when defining a trial, including any relevant contact time and temperature. Check both the removal result and the retained surface after the full sequence. If the compatibility of a plated, coated or otherwise sensitive feature is unknown, do not infer it from an acceptable result on plain steel.
Chemical selection also needs current safety and permitted-use information for the location and application. For example, US EPA controls on methylene chloride mean that product availability alone does not establish that a proposed use is permitted. Do not choose a chemistry from an old generic process description and assume its regulatory position remains unchanged.
Dry Ice Blasting for Deposits and Light Surface Oxidation
Dry ice blasting accelerates solid carbon-dioxide particles in an air stream. Their impact supplies mechanical action at the deposit. Rapid cooling can also make a responsive deposit contract and become brittle, helping it crack or separate; as the dry ice changes directly from solid to gas, the expanding gas can help lift loosened material. The contribution of each effect depends on the deposit and its thermal response. A layer that fractures or loses adhesion under these conditions is a more plausible candidate than one that remains firmly attached.
Unlike hard-grit blasting, this route does not rely on leaving a persistent cutting medium at the surface. There is no spent solid dry-ice media to collect after sublimation, but the detached contamination still has to go somewhere. That distinction can make deposit cleaning attractive where added grit is undesirable, while leaving both the removal result and the retained finish to be verified.
Oxide removal needs a particularly careful boundary. A manufacturer's rust-removal application guidance describes light surface oxidation applications and excludes heavy or pitted corrosion and work requiring a white-metal finish. That supports investigating particular light-oxidation jobs; it does not justify a general claim that dry ice replaces abrasive rust removal.
The response of the deposit—not the fact that the medium is cold—determines whether cleaning succeeds. Deposit removal and corrosion preparation are separate acceptance questions, so a trial must show what remains after treatment. If the next coating operation needs an anchor profile, do not assume that a deposit-removal result has supplied it. The process may be only one step in a longer preparation route.
Include CO₂ exposure and cold-contact hazards in the work-area assessment. Media that disappear from the surface do not disappear from the workplace as a hazard. This is especially relevant when considering cleaning around enclosed or poorly ventilated features, where safe conditions need a competent assessment rather than an assumption based on visible cleanliness.
Pure Waterjetting for Recoating Existing Steel
Pure waterjetting converts pump pressure into a fast-moving jet through a nozzle. The moving water delivers mechanical energy to the target layer, eroding or dislodging material rather than dissolving it chemically. For surface preparation, the useful result is removal of the unwanted coating or deposit while leaving the required underlying surface. Nozzle delivery and the actual layer response therefore belong in the trial; a pump-pressure number by itself is not proof of an acceptable finish.
For steel recoating, an important boundary is that pure waterjetting can expose a profile already present beneath an old coating, but does not create a new anchor profile in the way abrasive profiling can. A jet can remove the covering layer without giving smooth steel the texture needed by the next coating. Adding abrasive changes the process, so pure waterjetting and abrasive water treatment should not be treated as interchangeable.

That distinction changes the decision between existing coated steel and smooth new steel. On the existing surface, inspect what the removal reveals and compare it with the next coating's requirements. On the new surface, do not select pure waterjetting on the assumption that removal and profile creation are one operation. An additional qualified preparation step may be necessary. AMPP's guidance explains this existing-profile boundary.
Plan how the surface will move from cleaning to inspection and coating. Water management, flash-rust acceptance and the final observed condition belong in that sequence. High-pressure-fluid injury hazards also need controls specific to the actual equipment and task; a general warning about pressure is not an operating procedure.
Wet Abrasive, Soda and Contained Blasting
These options modify blasting rather than all replacing it with a non-abrasive process. Wet abrasive blasting combines water with abrasive media: the particles still act on the surface, while water helps keep fine debris from dispersing as airborne dust. Contained or vacuum-assisted blasting uses local collection around the blast area to recover media and detached material. They may address the reason for abandoning an open dry-blasting setup while retaining abrasive action.
These modifications solve different problems. Water and collection arrangements address debris dispersion; they do not by themselves remove particle impact on the part. The removed coating hazard and the proposed collection arrangement still determine the necessary exposure assessment. A shroud also has to work with the real geometry; a flat demonstration does not establish effective contact around every edge or obstruction.
Cleaning media and profiling media do different jobs
Do not choose a process by the word “soda” alone. Standard soda cleaning media and formulations containing additional abrasives for more aggressive preparation can have different intended roles. Identify the exact formulation before deciding what surface result to expect.
The same discipline applies to wet blasting: choose the medium and assess the resulting surface, rather than assuming that the presence of water makes the treatment harmless or residue-free. Reduced airborne dust does not remove the need to assess exposure, collect residues or check the condition left for coating. Where water is involved, include the applicable flash-rust requirement in the acceptance plan.
Match the Method to the Part and the Next Operation
Once the mechanisms are clear, a useful shortlist can be much smaller than the initial method list. First exclude routes that cannot meet a mandatory requirement. Then compare the remaining routes on the full part and process, rather than trying to rank every technology from best to worst.
Thin sections, retained finishes and difficult geometry
Identify the actual alloy, section thickness, features and layers to retain. “Metal” is not a sufficient compatibility description, and a stainless or coated part should not inherit a process conclusion from an unrelated steel sample. For a thin section, make dimensional condition part of the trial. For a retained working face, define the acceptable finish. For a recess, require evidence from that recess rather than only from an adjacent flat area.
Those checks have different consequences. A dimensional failure can eliminate a route even when removal is excellent. A profile shortfall can mean that a second preparation operation is needed. An inaccessible surface can make a proposed treatment impractical unless the part can be repositioned or the delivery method changed. The value of the shortlist is that each remaining uncertainty has a specific test.
How the shortlist changes between a mold and coated steel
Consider two illustrative jobs, not measured customer cases. In the first, a mold insert has a deposit to remove and a working finish to preserve. Local laser treatment or dry ice could be investigated if the deposit and access permit; a suitable chemical route could also be considered if the complete treatment and cleanup are compatible. The deciding evidence is removal with an acceptable retained surface, not how bright the insert looks. A more focused dry-ice and laser comparison for mold maintenance addresses that narrower application.
In the second job, steel needs recoating. Existing coated steel may already have a usable profile beneath the layer being removed. Smooth new steel presents a different starting condition. If a route only removes the unwanted material, it must not be credited with producing texture it has not demonstrated. The same method can therefore be useful on one job and incomplete on the other without either conclusion being contradictory.
Qualify the Complete Process on Representative Parts
A trial should answer the outstanding selection questions, not simply produce a clean demonstration patch. Use representative material, contamination and geometry, and agree what constitutes an acceptable result before comparing suppliers or settings. Include the full proposed route: handling, treatment, any rinsing or secondary preparation, inspection and the intended next operation.
Set safety and acceptance conditions before the trial
Identify the coating or deposit as far as practicable before treatment. The removed material can determine the exposure and waste controls even when the chosen cleaning medium changes. Establish the work-area controls with the people responsible for the equipment and process: laser containment and reflections, dust extraction, chemical handling, CO₂ exposure or pressure hazards as applicable. Do not use an unidentified coating as an invitation to run an uncontrolled test.
Give each acceptance requirement an owner and a source. The coating specification, component drawing or downstream-process requirement should determine the criterion; the trial operator should not invent a convenient pass limit after seeing the result. Agree how to handle a partially cleaned area or a retained feature that changes, and keep an untreated reference where it helps the comparison.
Measure the surface the next operation actually needs
Choose a measurement because it answers the acceptance question. A visual inspection can document remaining visible material, but it cannot establish every residue or functional property. Profile measurement addresses texture. A soluble-salt assessment addresses a different concern. Neither should be substituted for the other simply because both are called surface inspection.
ASTM D4417-21 addresses measurement of profiles on blast-cleaned steel, with a note on possible Method B use for power-tool-produced profiles. Its public scope does not make every instrument appropriate for every surface. ISO 8502-9:2020 describes conductometric assessment of water-soluble salts; it does not identify the individual surface density of a named ion. A qualitative water-break test under ASTM F22-21 concerns hydrophobic films. It does not establish a salt level, profile or adhesive bond strength.
Use a small acceptance record to keep these questions separate. Select only the checks relevant to the actual next operation.
| Acceptance question | Evidence to record | Who defines the criterion? | What a gap changes |
|---|---|---|---|
| Has the target layer been removed? | Agreed inspection method, locations and remaining material | Process or coating specification owner | Further removal or rejection of the route |
| Have required features been retained? | Relevant finish, dimensional or retained-layer checks | Component owner or drawing requirement | Reconsider treatment conditions or method |
| Is the required texture present? | Specified parameter, suitable measurement method and locations | Downstream process specification | Qualify a profiling step if needed |
| Are relevant residues acceptable? | Target-specific test method and reported result | Applicable coating or process requirement | Improve cleanup or change the route |
| Does the next operation perform acceptably? | Agreed coating, bonding or other functional validation | Responsible downstream-process owner | Resolve the preparation/process combination |
Record the treatment configuration, sequence, observations and inspection results together. If a second step is needed to pass, it becomes part of the qualified route and its cost. A successful first pass alone is not the production process.

If laser remains on the shortlist, contact Oceanplayer with the material and layer details, part photographs, access constraints and required final condition. Use those inputs to discuss feasibility; agree the actual trial and inspection scope rather than assuming that a quotation includes every acceptance test.
Compare Total Job Cost, Not Just Cleaning Time
Compare routes only after defining the same accepted output. A faster removal pass can still belong to a longer job if it needs extra handling, cleanup or surface preparation. Conversely, a method with a slower treatment step may deserve consideration if its complete qualified sequence fits the production requirement better. These are comparison principles, not claims that one technology has lower cost.
Include handling, cleanup and any second preparation step
For each candidate, record preparation and masking, access or repositioning, removal, cleanup, required secondary treatment, inspection and evidence-based rework. Include the appropriate equipment, consumables, labor, controls and waste-handling costs. Keep one-time qualification work separate from recurring production work so the comparison remains interpretable.
Also distinguish elapsed time from labor time. If two activities overlap, adding their durations does not give the elapsed cycle; if a worker must remain occupied, that labor still belongs in the cost. Record the actual sequence and resource use rather than filling a comparison table with guessed industry averages.

The purchase decision should explain which complete route meets the required surface and production conditions, and which assumptions still need confirmation. A cleaning-speed figure without that context is insufficient for a payback calculation.
Frequently Asked Questions
Can two cleaning methods be combined in one preparation route?
Yes, a combined route can be considered when the steps address different requirements, such as removal followed by qualified surface preparation. Validate the sequence as a whole. Check that the first step does not leave a condition that defeats the second, and that cleanup and handling are included. Results from two unrelated demonstrations do not prove that the combined route works on the production part.
Can an alternative satisfy a specification that calls for blasting?
It may be considered, but a similar appearance does not establish acceptance of the substitution. Determine whether the specification requires a named process, a measured endpoint, or both. Have the responsible specification owner review the proposed route and supporting evidence before treating it as an accepted replacement. Do not assume that a laser, chemical or tool-cleaned surface automatically carries a particular blasting grade.
Technical References and Acceptance Standards
The references below support the process distinctions and verification boundaries discussed here. Public standard summaries identify scope; use the applicable complete specification when defining a production acceptance procedure.
- AMPP: Waterjet and wet abrasive blast cleaning methods — existing profile, wet abrasive treatment and flash rust.
- ASTM D4417-21, ISO 8502-9:2020 and ASTM F22-21 — public scopes for profile, conductometric salt assessment and water-break testing respectively.
- OSHA Technical Manual, Section V, Chapter 3 — descriptions of power-tool, chemical, dry-ice and vacuum-blasting methods. Its historical cost and chemical-regulation discussions are not used as current guidance here.
- IPG: What is laser cleaning? and cleanLASER: Technical feasibility — energy delivery, layer response and access considerations.
- Solvent–polyurethane interaction study and CRC chelation explanation — bounded examples of coating swelling and chemical derusting; neither is a universal chemistry or material-compatibility prescription.
- Cold Jet: Dry-ice mechanism and Flow: Pressure-to-velocity principle — qualitative physical mechanisms only; cutting-machine performance and manufacturer-wide safety promises are not adopted.
- MontiPower: Bristle Blaster, CRC: Evapo-Rust use instructions and ARMEX FAQs — specific tool action, a product-specific cleanup sequence and formulation distinctions; not universal performance guarantees.
- Cold Jet: Rust-removal application scope — the light-oxidation boundary discussed above; no supplier speed or damage-free promise is adopted.
- FDA laser safety FAQ, HSE abrasive-blasting guidance, NIOSH carbon dioxide guide and HSE fluid-injection bulletin — bounded hazard references, not a substitute for task-specific controls.
- US EPA: Methylene chloride risk management — jurisdiction-specific context for chemical selection; no universal permitted-use conclusion is implied.