
When Should You Not Use a Laser Cleaning Machine? 9 Poor-Fit Jobs
Laser cleaning is not suitable for every removal task. It may be a poor choice when the process cannot remove the unwanted layer without unacceptable change to the surface below, cannot reach the contamination, cannot deliver enough accepted output over a complete production cycle, or creates hazards the worksite cannot control.
The nine situations below are screening cases, not universal bans. Some call for an immediate stop. Others justify a controlled trial or a different method. The useful question is not whether a laser can make a small area look clean; it is whether the complete job can meet its surface, production and safety requirements.
In this article
Quick Answer: When Is Laser Cleaning the Wrong Choice?
Stop when an essential condition cannot be met: the protected surface would be altered beyond its limit, hazardous material cannot be captured, or the work area cannot be made suitable for the operation. Test first when the layer stack, material response, inaccessible features or cycle time is uncertain but can be investigated safely. Choose another method when it can reach the whole part and meet the same acceptance standard more reliably or economically.
These decisions depend on the actual part. Laser energy interacts with the unwanted layer and, once that layer thins or disappears, with whatever lies underneath. Wavelength, intensity, exposure time and material properties all influence what happens at that boundary, as Fraunhofer ILT's process explanation describes. Increasing power can accelerate removal in one trial while narrowing the margin before substrate change in another. Changing the laser alone does not solve a blocked line of sight or an uncontrolled work area.
When Do Materials and Surface Requirements Make Laser Cleaning a Poor Fit?
Three material-related jobs deserve early screening. They share a practical problem: removing the visible contaminant is not enough if the protected layer, dimensions or function changes in the process.
1. Can You Clean Surfaces with Unknown or Inconsistent Coatings?
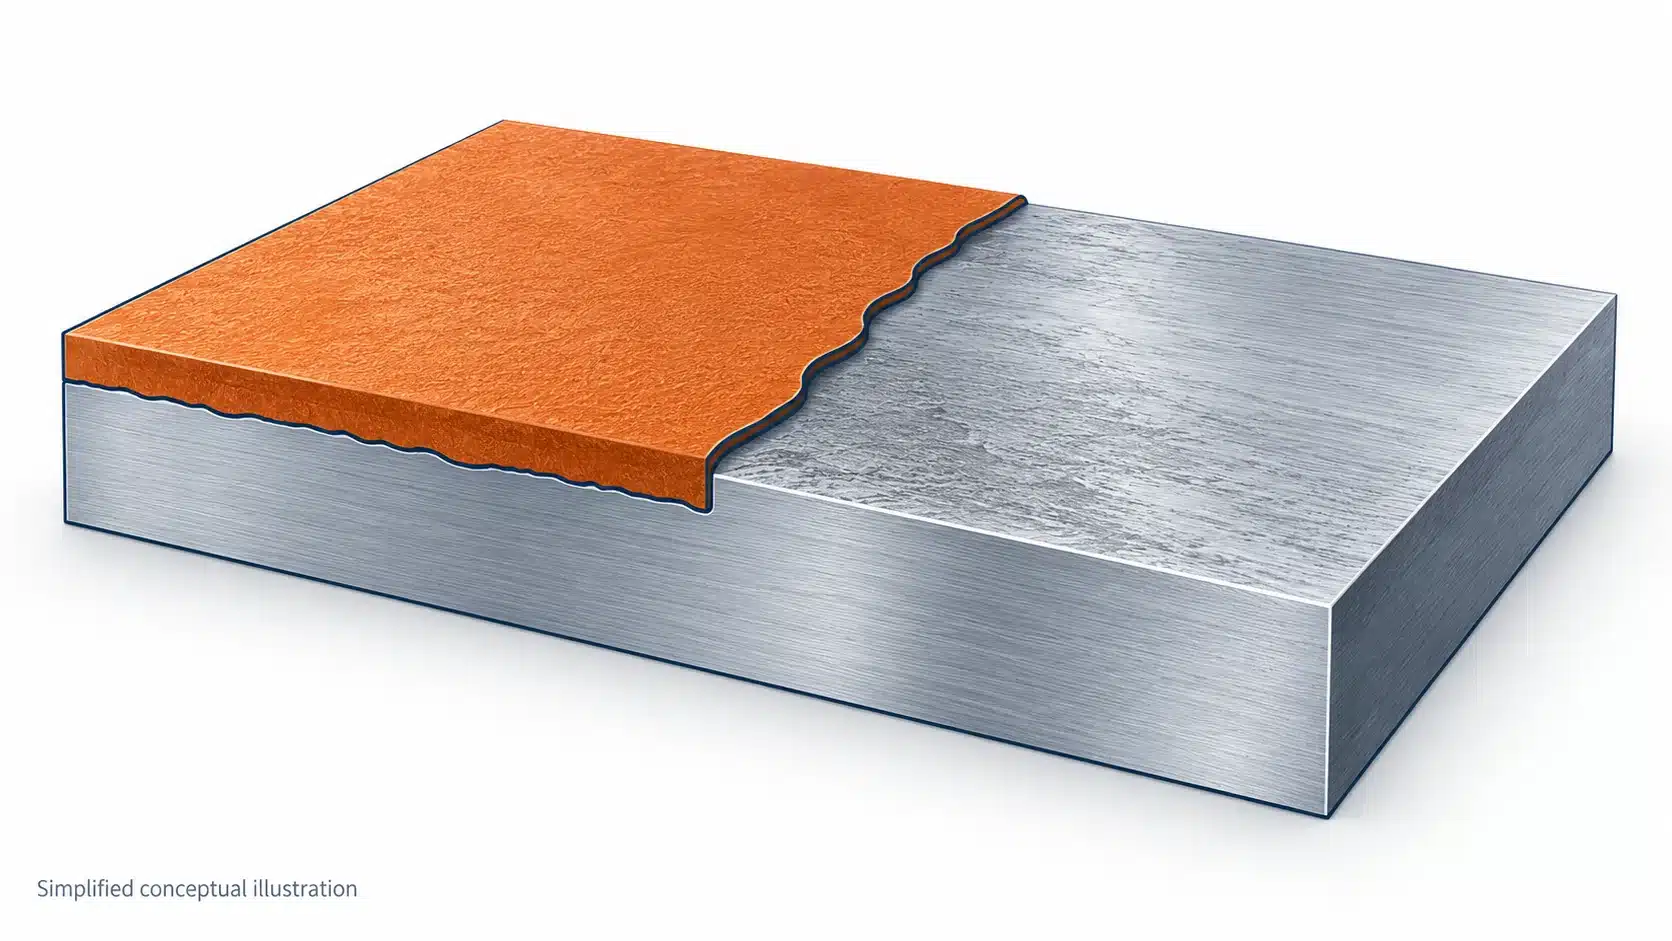
A structure may contain original paint, repair paint, primer, filler, corrosion products and oil in different places. A setting that removes a thin topcoat may leave a thicker repair patch; another pass may expose or alter the primer that the job required you to retain. Color alone cannot identify the layer sequence or tell you whether a coating contains hazardous constituents.
First separate the removal question from the hazard question. A test can show whether a known stack can be cleaned to a defined endpoint. It cannot make an unidentified coating safe merely because the surface looks acceptable. Review available coating and maintenance records, identify suspect materials, and map the variation across representative areas before selecting a process. If that information cannot be obtained, pause the laser trial and consider a characterization or containment route first.
2. Is Laser Cleaning Suitable for Heat-Sensitive Plastics, Rubber, or Composites?
Polymers and composites do not respond like a steel plate. A coating may absorb energy, but the resin, adhesive or elastomer underneath can also soften, decompose, shrink or lose a required property. In a published infrared nanosecond CFRP paint-stripping experiment, substrate damage appeared under the studied material and process conditions. That result is a warning to test the actual stack, not a conclusion that every composite is impossible to process with every laser.
Ask what the part must retain after cleaning: bond strength, sealing behavior, fiber integrity, geometry, appearance or electrical properties. A trial should compare the treated area with an untreated control using methods that can detect the earliest unacceptable change. If a conventional cleaning setup cannot remove the deposit before the protected material changes, screen a compatible solvent, controlled manual method, dry ice or a specialist laser process according to the part specification. None of these alternatives is automatically safe for the material either.
3. Should You Use Laser Cleaning on Precision, Plated, or Optical Surfaces?
On a precision part, “clean” may mean more than the absence of visible residue. A slight change in roughness can matter on a sealing face; loss of a thin plated layer can change electrical contact; a change in reflectance can make an optical surface fail its purpose. Cosmetic finishes can fail because of a color or gloss difference even when the base material is structurally sound.
The removal target and protected property must therefore be measured separately. A study of paint removal from a specific aluminum alloy examined both a cleaning threshold and a damage threshold, illustrating why the acceptable operating range must be established for the actual coating and substrate; its reported values are not settings for another part or machine (published study record). Define the allowable coating thickness, roughness, dimension, reflectance or functional result before the trial. If the required limit cannot be measured, a bright-looking sample is not a qualification result.
When Do Geometry and Production Requirements Limit Laser Cleaning?
Laser cleaning can succeed on an exposed test patch and still fail as a production route. The complete workpiece determines beam access, the number of passes and how much accepted output remains after handling and inspection.
4. Is Laser Cleaning Practical for Thick Coatings or Large Surface Areas?
Removing more material generally requires more energy delivery, pass time and management of the removed material. A thick or strongly adhered layer may need multiple passes; a large structure multiplies repositioning and access work. A high scan speed quoted for one pass says little about how long it takes to produce an inspected, acceptable part.
Measure the worst representative coating rather than relying on a universal thickness limit. Record treated area, passes, setup, movement, extraction, inspection and rework. Then compare accepted area per hour or accepted parts per shift with the same boundary for abrasive, water or chemical alternatives. A laser may still make sense for a small critical zone after bulk removal, even if it is uneconomic for the entire surface. Conversely, successful removal on one coupon does not establish the cost of treating a whole asset.
5. Can Laser Cleaning Reach Blind Holes, Internal Channels, or Hidden Surfaces?
The beam must reach the required location at a workable angle and focus. A lip, bend, assembled joint or deep channel can shadow the target. Even where the beam reaches an opening, the cleaning head and extraction arrangement may not reach a position that provides a consistent result. A clean outer surface says nothing about a hidden internal passage.
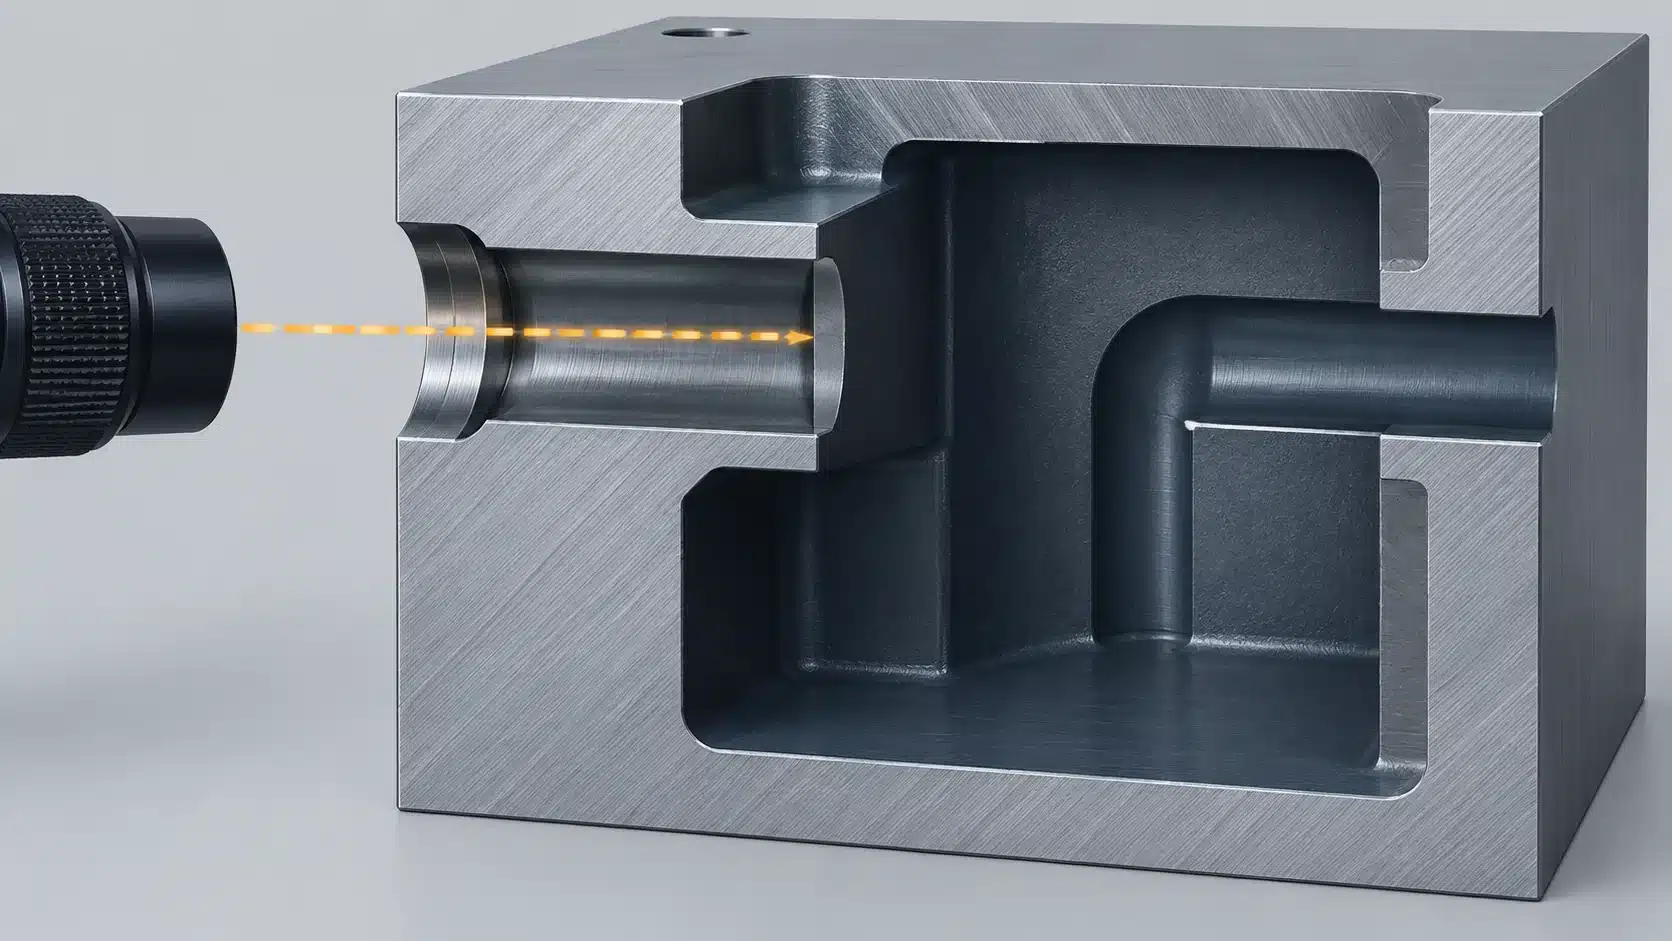
Map every required cleaning location on the drawing and on a representative part. Check access with the actual optics, fixture, standoff and extraction setup. Disassembly, a dedicated delivery system or a different process may make the job possible, but each changes the cycle and must be tested. If the hidden surface is a required acceptance area and cannot be reached or inspected, do not qualify the process based on visible features alone.
6. Can Laser Cleaning Remove Contamination Embedded in Pores or Deep Pits?
Laser cleaning acts where energy reaches the material. Removing the top of a deposit can expose clean-looking metal while contamination in pits, pores or interfaces remains untested. In a published study of contaminated oxidized steel surfaces, residues integrated into oxide layers required attention to the removal depth, and the researchers used laser analysis to check the cleaned surface. That study does not establish that lasers cannot clean pits; it shows why appearance alone is an incomplete endpoint. Whether remaining contamination matters depends on the next operation and the specified acceptance limit.
Specify which contaminant must be removed and from what depth or location. Then choose a method capable of measuring the relevant residual condition, such as a process-specific extraction, chemical analysis, microscopy or downstream performance test. Do not claim full-depth cleanliness from a photograph. If the required depth cannot be reached or verified, compare a method that flushes, dissolves or otherwise accesses the contamination—while also checking its compatibility with the part.
When Do Safety or Preservation Requirements Rule Out Laser Cleaning?
The following cases are not problems to solve by turning up the machine. They require hazard identification, a qualified work plan or a decision to use another route.
7. Should You Laser-Clean Unknown or Hazardous Coatings Without Verified Fume Control?
Laser removal converts part of a coating or deposit into airborne material and collected waste. The material being removed determines what the plume and filters may contain. Knowing that a paint is present is not the same as knowing its constituents, the products created during processing or whether the capture arrangement controls exposure.
For hand-held Class 4 laser cleaning and decoating, DGUV's FBHM-139 guidance addresses both laser radiation and hazardous substances, including capture close to the source. Its scope is specific; the applicable requirements for another installation or jurisdiction still need to be determined. Identify suspect lead, chromate or other hazardous coatings before processing, establish the exposure and waste controls for the actual material, and verify that extraction works in the real geometry. If those controls cannot be established, stop production cleaning rather than relying on “no abrasive media” as a safety argument.
8. Can You Use Laser Cleaning in Flammable or Potentially Explosive Environments?
Flammable vapor, mist, gas or combustible dust changes the decision. Laser radiation and heated surfaces or particles can create ignition hazards. IEC 60079-28:2025 defines additional requirements for specified optical-radiation equipment exposed to explosive atmospheres; citing the standard does not certify an ordinary cleaner for a particular site.
Assess the actual area, atmosphere, surrounding materials and equipment configuration through the site's qualified hazardous-area process. Draining a tank does not by itself establish that the interior is suitable for laser work. The operation may need isolation, cleaning, testing, a different location and correctly assessed equipment—or it may need to be rejected. A routine open-beam cleaner should never be assumed suitable merely because it can remove the deposit.
9. Should You Laser-Clean Irreplaceable Artifacts or Parts That Cannot Tolerate Damage?
For a historic surface, unique master or one-off high-value component, there may be no replaceable sample on which to discover the damage threshold. The original finish, patina, tooling marks or evidence of manufacture may be part of what must be preserved. A technically successful removal can still be an unacceptable intervention.
Document the existing condition, define exactly what may change, and place the decision with the responsible conservator or engineering authority. Cultural-heritage technical guidance emphasizes assessment and monitoring for laser interventions; this does not mean lasers are categorically unsuitable for heritage work. Where reversibility matters, consider it explicitly rather than assuming that a noncontact method is reversible. If there is no acceptable test location, measurement method or specialist approval path, choose a less intrusive approach or leave the surface untreated.
What Cleaning Methods Work Better When Laser Cleaning Is a Poor Fit?
Choose the alternative against the same required end state. A process that removes coating quickly but changes the substrate, leaves trapped residue or creates an unacceptable waste stream has not solved the job.
How Do Abrasive, Chemical, Water, Dry-Ice, and Manual Cleaning Compare?
| Method to evaluate | Where it may fit | Main qualification question |
|---|---|---|
| Abrasive blasting or mechanical tools | Accessible metal areas needing bulk removal or a specified profile; local tools for small zones | Will the media or tool remove or deform base material, and can dust, noise and spent media be controlled? |
| Chemical stripping or compatible solvents | Coatings that can be dissolved or loosened on compatible parts, including some complex shapes | Will the chemistry attack the substrate or protected finish, and how will residue, rinsing and waste be managed? |
| Aqueous or high-pressure water cleaning | Washable contamination or broad accessible surfaces where water is acceptable | Can the part tolerate water and pressure, and will the required surface profile or dryness be achieved? |
| Dry-ice blasting | Some deposits on surfaces where retained abrasive media is undesirable | Does the deposit respond to the process, and can ejected contamination, ventilation and visibility be controlled? |
| Manual cleaning or controlled disassembly | Small, delicate or otherwise inaccessible zones | Can every required location be reached consistently without unacceptable labor, damage or residue? |
These are candidates, not recommendations made from the method name alone. For example, OSHA's abrasive-blasting fact sheet describes its use for cleaning and surface preparation while also identifying dust, toxic-material and noise hazards. A safer choice for one site or substrate may be worse for another. Compare removal completeness, protected-surface condition, access, worker controls, waste and accepted output under a common test plan.


When Is a Hybrid Cleaning Process More Practical?
A combination can separate tasks that one process handles poorly. Bulk blasting or water removal might treat a large accessible area, followed by a localized laser pass where selective cleaning is valuable. Alternatively, disassembly may expose a hidden zone for a controlled manual or laser treatment. The sequence must not carry contamination or moisture into the next step, and the final surface still needs one agreed acceptance check.
Hybrid processing can add setup, transfers and inspections as well as remove passes. Compare its complete accepted cycle with a single-process alternative before calling it faster or cheaper.
How Can You Determine Whether a Borderline Job Is Suitable for Laser Cleaning?
A trial should answer a defined engineering question, not merely produce a before-and-after photograph. Agree on the acceptance result and safety boundary before selecting settings.
Step 1 — Define the Required Cleaning Result and Surface Limits
Record the substrate, layer stack, area, geometry and next operation. State what must be removed, what may remain, what must be protected and how each result will be checked. A visual inspection may identify remaining visible coating; it cannot alone establish chemical cleanliness, bond strength or the integrity of a thin functional layer. Use the drawing, process specification or qualified owner's acceptance criteria rather than a generic blog limit.
Step 2 — Test Representative Materials and Worst-Case Conditions
Include the thickest and most variable coating, difficult angles, sensitive substrate areas and realistic fixtures. Record the actual laser source/mode, beam and spot conditions at the workpiece, scan strategy, overlap, number of passes and any relevant material response. Inspect both the removal target and the protected surface after the part has reached the condition in which it will be accepted. Document the work-area controls and the nature of the collected material. A result from an easy flat coupon does not qualify a hidden corner or a different coating batch.
Step 3 — Measure Accepted Output and Total Process Cost
Start and stop the clock at a stated production boundary. Include loading, positioning, cleaning, repositioning, extraction maintenance, inspection, rework and waste handling when they occur in the actual cycle. Report accepted area or accepted parts, not only scan speed or laser-on time. Compare alternative methods using the same quality requirement and cycle boundary. A single successful test establishes feasibility for its conditions; repeated representative runs are needed to judge stability.
Step 4 — Decide Whether to Proceed, Modify, or Reject the Process
| Trial outcome | Next decision |
|---|---|
| Removal and protected-surface requirements pass; site controls and accepted throughput are adequate | Proceed to the site's production qualification process. |
| Removal passes, but access or complete-cycle output does not | Rework the fixture, sequence or process choice; retest before specifying equipment. |
| Surface damage or residual contamination exceeds an agreed limit | Investigate another process window or method; reject the route if the limit cannot be met. |
| Essential exposure, beam or ignition hazards cannot be adequately controlled | Stop the work and do not implement the process. |
The decision record should name the tested part and configuration, measurements, acceptance criteria and person responsible for release. It should also state where the conclusion does not apply, such as a thicker coating or a different location.
Frequently Asked Questions
Can More Laser Power Make an Unsuitable Cleaning Job Suitable?
Sometimes more delivered energy can remove a layer faster, but it can also change the substrate, increase the material that must be captured or worsen heat accumulation. Power alone does not fix blocked access, an unidentified coating or an unsuitable work area. Retest the complete result rather than treating rated watts as a pass/fail answer.
Is Pulsed Laser Cleaning Always Safe for Delicate Surfaces?
No. Shorter individual exposures can help localize energy under some conditions, but pulse energy, spot size, repetition, overlap, absorption and repeated passes still determine what the part receives. A delicate surface needs a measured removal endpoint and protected-surface limit for the actual configuration.
Can Laser Cleaning Work When Some Surfaces Are Difficult to Reach?
Possibly, if a fixture, repositioning, disassembly or qualified beam-delivery arrangement exposes every required area and permits adequate extraction. If a critical hidden surface remains unreachable or uninspectable, a clean visible area cannot qualify the whole part. Compare another method that can reach the location and meet the same acceptance criteria.
Technical References
- Fraunhofer ILT, Laser Cleaning — process interaction and governing variables.
- Shan et al., Surface integrity control of laser cleaning of an aluminum alloy surface paint layer, Applied Optics (2020) — one material-specific cleaning/damage-window study.
- Investigation on laser paint stripping of CFRP: Morphological evolution, damage mechanism, and adhesive performance, Journal of Materials Research and Technology (2024) — material-specific composite damage mechanisms.
- DGUV, FBHM-139: Blasting work — cleaning and decoating with laser radiation (2024) — hand-held Class 4 cleaning and decoating risk-assessment scope.
- IEC, IEC 60079-28:2025: Explosive atmospheres — optical-radiation equipment — scope and ignition mechanisms; not equipment approval by itself.
- Analytical Methods Committee, Introduction to laser cleaning in cultural heritage, Analytical Methods (2026) — assessment and monitoring; source consulted at abstract level.
- OSHA, Protecting Workers from the Hazards of Abrasive Blasting Materials — abrasive-blasting uses and hazards in its U.S. guidance context.
- Fox et al., A novel laser-based approach for cleaning contaminated metallic surfaces coupled with rapid residue analysis, Proceedings of SPIE (2013) — contaminated oxidized steel and the need for analytical confirmation under the studied conditions.