
Laser Cleaning Speed: Why Demo Rates Differ from Real Production Throughput
A laser cleaning speed quoted during a demonstration may not represent the output achievable in production. Actual throughput depends on the required cleaning quality, effective treatment width, number of passes, part geometry, handling, inspection, and rework. To compare systems fairly, buyers should measure accepted output over a clearly defined production cycle rather than relying on scan speed or an isolated demonstration rate.
The useful question is not simply “How fast can the beam move?” It is “How many acceptable surfaces or parts can this process deliver under our operating conditions?” A supplier can answer both questions honestly and still give very different numbers. The difference becomes clear when the unit, quality endpoint, sample and clock are written down together.
What Does Laser Cleaning Speed Actually Mean?
Scan Speed vs. Cleaning Rate vs. Production Throughput
Scan speed describes the beam's movement along a programmed path, commonly in millimeters per second. A scanning head may sweep rapidly across a workpiece while the head itself advances more slowly. The same line can also be scanned more than once. Beam travel therefore describes a machine motion, not the area that passes inspection in an hour.
Cleaning rate usually refers to treated area per unit time, but the phrase is incomplete without a definition. Does “treated” mean the beam crossed that area, visible contamination disappeared, or a specified condition was met? A nominal scan width may include edge zones that need another pass. If those zones fail the agreed endpoint, they cannot be counted as accepted output just because the beam covered them.
Production throughput is the accepted area or number of accepted parts delivered over a defined operating period. This is the figure that can be compared with a line requirement. It depends on the cleaning recipe and on everything needed to present, process and release a part. Manufacturing KPI research distinguishes good quantity, rework and operating time when constructing production measures; the NIST-hosted production KPI study supports this measurement distinction, not a laser-specific performance rate.
Why mm/s, m²/h, and Parts per Hour Are Not Interchangeable
These units measure different things. Millimeters per second describes one motion. Square meters per hour describes an area rate, provided the area and clock are defined. Parts per hour counts finished items, provided the part mix and acceptance decision are defined. A large flat panel and a small bracket may have the same total target area but very different access, edge work and handling time.
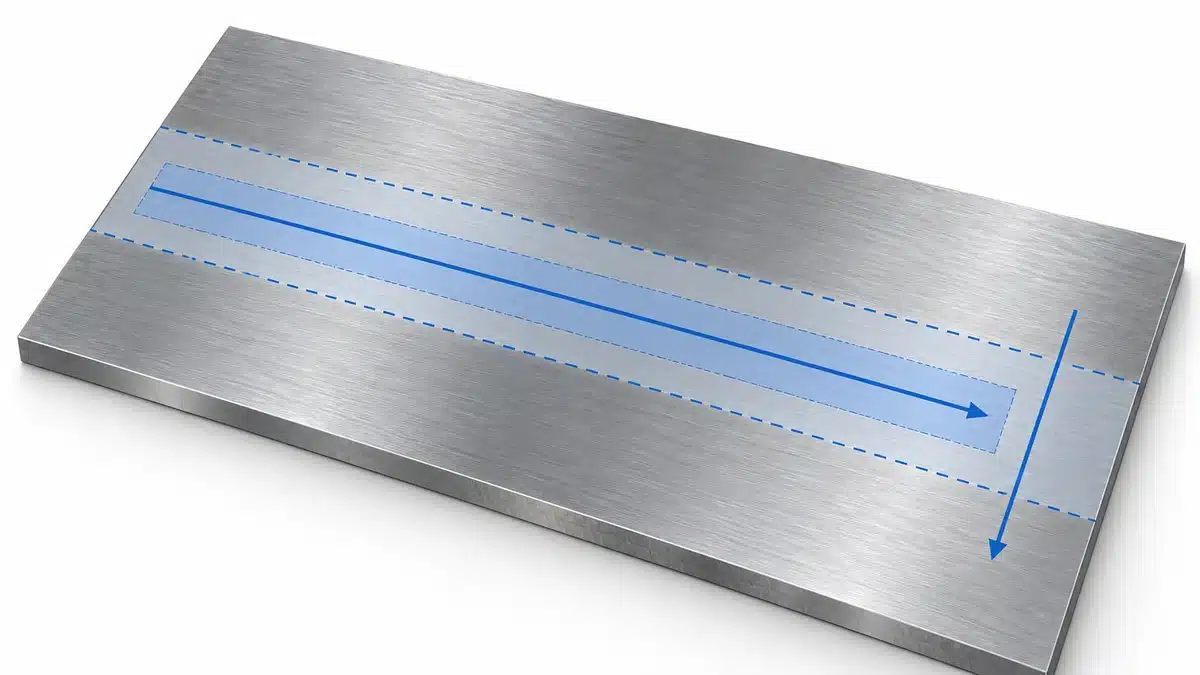
To estimate area coverage from motion, a process engineer may multiply an effective accepted path width by a stable workpiece-relative feed rate and then account for repeated paths. That is a geometric estimate, not a measured production rate. It is invalid if the width is only a brochure scan field, if passes overlap differently on the actual part, or if cleaning quality changes along the path. The result also cannot be converted to parts per hour without knowing each part's target area and complete cycle.
| Reported figure | What must be specified | What it can answer |
|---|---|---|
| Beam scan speed, mm/s | Path, workpiece position and scan settings | How fast the beam traverses a line under those settings. |
| Accepted area rate, m²/h | Area that meets the endpoint and exact time boundary | How much qualified surface was produced during the measured period. |
| Accepted parts per shift | Part mix, inspection result and full shift period | Whether the process delivered the required number of usable parts. |
Laser-On Time vs. Complete Production Cycle Time
Laser-on time begins when the beam is processing and ends when it stops. It is useful for comparing recipes on the same sample and endpoint. A complete production cycle also includes the activities necessary to process that part: loading, locating, moving between regions, inspection and any rework included in the agreed test boundary. Depending on the installation, extraction checks or access-control steps may also affect the cycle.
Write the clock boundary before testing. For example, “from the operator's first loading action to the recorded acceptance decision” is a different test from “beam enabled to beam disabled.” Neither is inherently wrong; they answer different questions. If a measured full cycle already includes inspection and rework, subtracting a separate “inspection allowance” or multiplying by another yield factor would count the same loss twice.
Why Do Demonstration Cleaning Rates Differ from Production Results?
Effective Cleaning Width, Scan Overlap, and Multiple Passes
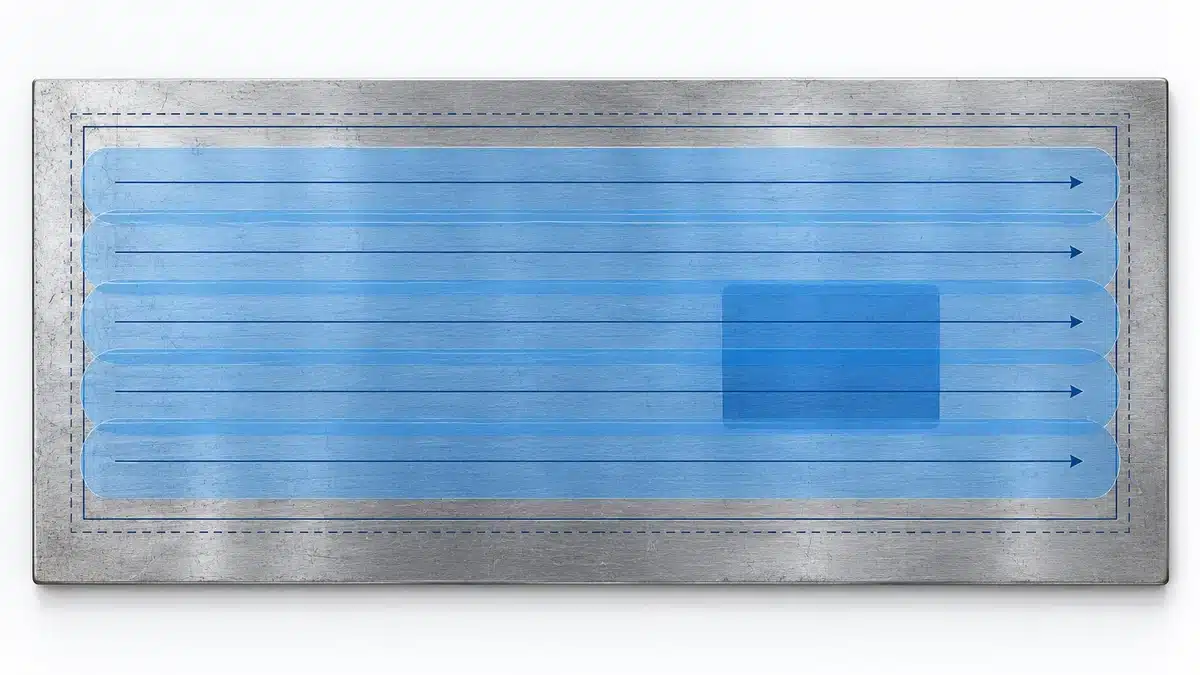
A demo often uses an accessible, uniform strip. The beam may scan a much wider field than the strip that consistently meets the removal target. Near the path edges, local exposure can differ from the center. Adjacent tracks therefore need a defined hatch spacing and overlap. If the spacing is too wide for the actual layer, untreated bands may remain; if it is made smaller to protect quality, more paths are needed to cover the same area.
Changing speed or widening the path can also change the energy received at a point. A fast first pass may leave adhered material that requires a second pass. That extra work is part of the real rate. Record effective accepted width and actual pass count on representative samples, rather than multiplying the maximum scan width by the fastest programmed motion.
Complex Surfaces, Corners, and Hard-to-Reach Areas
Edges, ribs, holes and recesses interrupt the simple flat-panel calculation. The operator or robot may need a new angle to expose the contaminant without sending the beam onto a surface that must be preserved. A curved part also changes working distance and beam incidence as it moves. Those changes can narrow a qualified process window or require separate paths for different regions.
The practical test is to divide a representative part into regions that actually need cleaning. Record which regions can be reached in one setup, which require repositioning and which remain outside the validated path. A high area rate on the easiest face does not describe the full part if the last corner controls completion.
Part Loading, Positioning, and Equipment Movement
Production output depends on how reliably each part reaches the programmed cleaning position. Fixtures may be needed to expose the required area and prevent movement. Handheld work can spend time moving the head, checking access and resetting the workpiece. An automated cell can reduce some handling but introduces loading, clamping and motion between paths.
Measure these activities as they occur in the intended production arrangement. If a demonstration operator manually places one coupon in an open workstation while production will run enclosed fixtures and mixed parts, the demonstration clock does not describe that production workflow.
Inspection, Rework, and Process Interruptions
Inspection is part of production when release depends on it. If a region fails, the result must be recorded along with the extra pass, repair or rejection. A report showing only the time for successful first passes hides the work needed to deliver accepted output.
Required beam control and fume extraction are likewise part of the process, not optional penalties added to a speed formula. The exact arrangement depends on the system and workplace risk assessment. Health Canada's laser-product guidance identifies direct and reflected beam hazards and fire hazards for Class 4 lasers; the ISO 11553-2:2026 scope addresses hand-held or hand-operated laser processing machines specifically. A fixed automated installation may fall under a different part of that safety framework. Record the controls actually used during the trial instead of assigning a universal percentage for “safety downtime.”
How Does the Required Cleaning Quality Affect Speed?
Define the Removal Target and Acceptable Surface Condition
“Clean” must be an observable endpoint. One job may require removal of a loose surface deposit; another may require removal of a bonded coating without unacceptable change to the base metal. Before timing, specify the starting layer, target region, permitted residue, allowed substrate or coating change, and who decides acceptance. Otherwise the fastest setting may simply stop too early.
This is also why two suppliers' area rates cannot be compared if one test stops when the dark color fades and the other continues until the surface meets a downstream specification. Faster visual change is not the same as faster accepted production.
Why a Visually Clean Surface May Still Fail Inspection
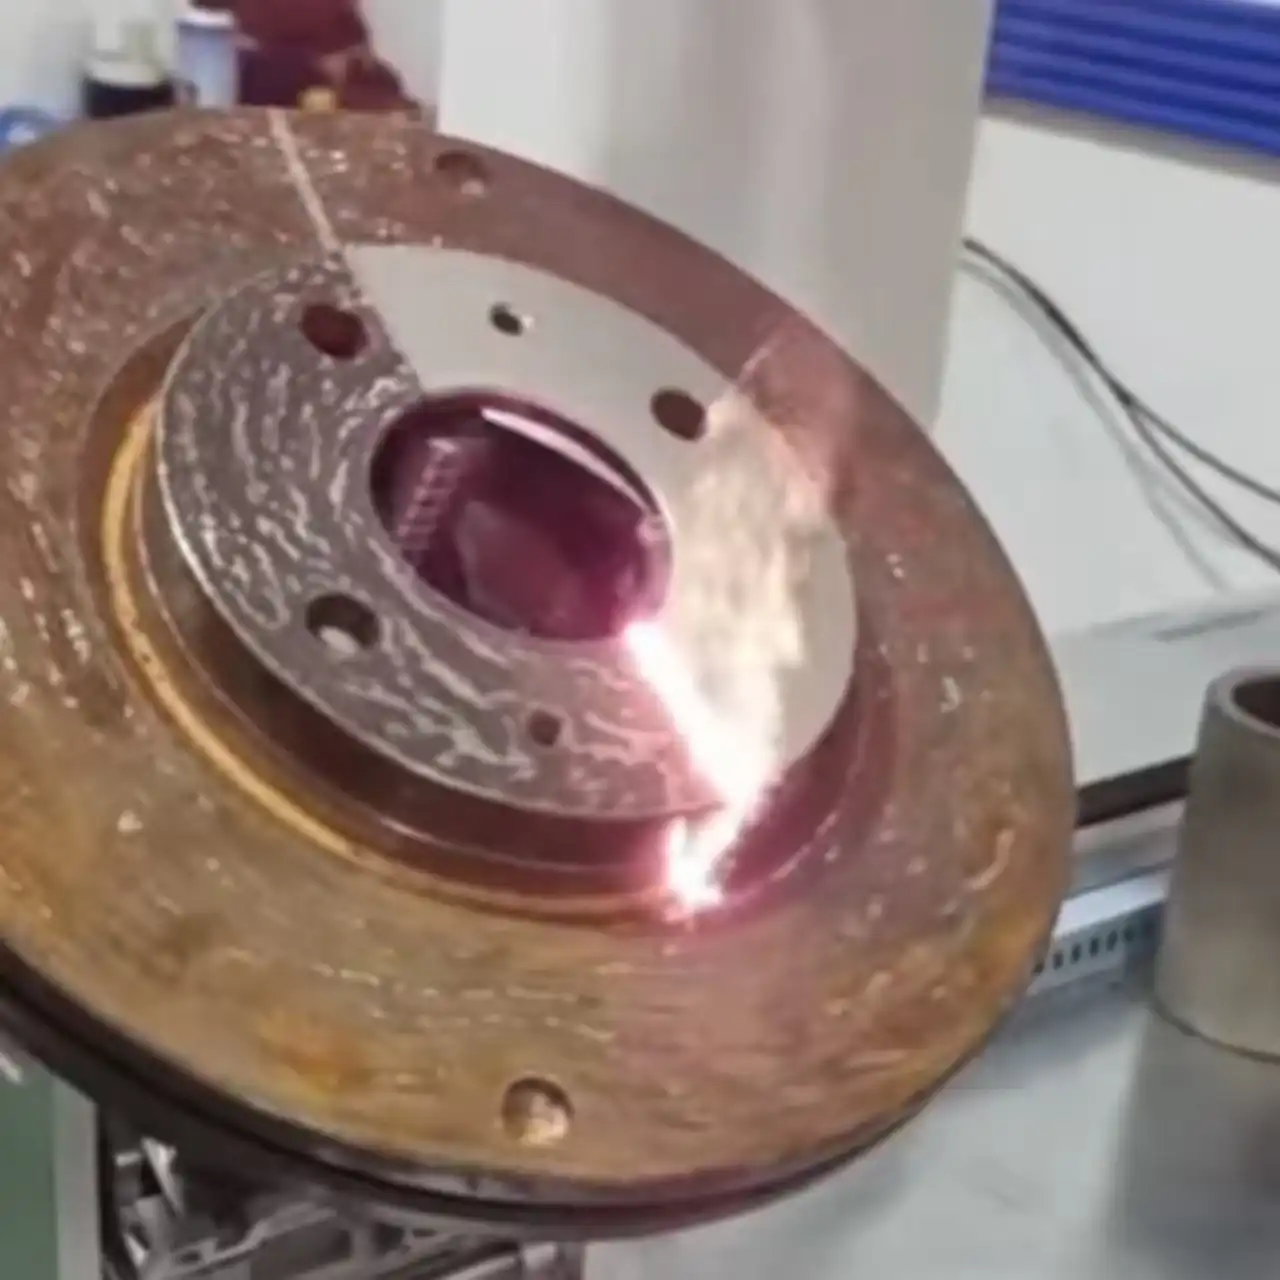
Lighting and viewing angle can hide a thin residual film or reveal discoloration that is not the same as remaining contamination. Visual inspection is useful when the requirement is visual, but it does not measure every chemical or functional property. For applicable steel prepared for painting, ISO 8501-1:2007 defines visual rust and preparation grades within a specific scope; it is not a universal laser-cleaning pass/fail rule. Where a steel-coating specification also calls for soluble-salt assessment, ISO 8502-9:2020 describes a field conductometric method; it does not identify each individual ion or set one universal acceptable limit.
Choose an inspection method that answers the actual release question. A part can look clean yet fail a specified residue, profile, dimensional or functional requirement. Conversely, a harmless color variation should not automatically trigger another pass unless the acceptance criteria say it matters.
Different Requirements Before Welding, Painting, or Bonding
The next process changes what the cleaning step must accomplish. A welding procedure may focus on removing material that interferes with the defined joint region while preserving fit-up and dimensions. A coating specification may require a stated visual condition, contamination control and a suitable surface profile; cleaning alone does not necessarily create that profile. Bonding may need its own surface preparation and validated adhesion outcome. None of these can be reduced to “bright metal.”
Agree on the downstream requirement before choosing a cleaning recipe. Then run the quality check after cleaning, not only after the downstream process fails. The accepted cleaning rate is the rate at which the surface meets that requirement without unacceptable substrate change.
How Do Laser Parameters and Material Conditions Affect Cleaning Speed?
Contamination Type, Layer Thickness, and Adhesion
A loose oxide, a thin paint film and a tightly bonded thick coating do not present the same removal problem. They differ in how they absorb energy, how they separate from the substrate and how much material must be removed. The base metal, surface finish and part thickness also affect how much thermal or surface change is tolerable. A rate measured on one layer/substrate combination cannot be assigned to another merely because the area is the same.
In a published nanosecond laser study on paint-coated Q345 steel, changing scan conditions changed both residual paint and the cleaned surface's appearance under the studied setup. That result illustrates the need to judge removal and substrate condition together. Its tested settings and rates are not Oceanplayer Laser performance figures and are not a recipe for another material.
Laser Power, Spot Size, Pulse Settings, and Scan Strategy
Rated power describes a source or system specification, not the energy delivered to each location on a moving part. At the workpiece, spot size changes the area over which energy is distributed. For a pulsed laser, average optical power, energy per pulse, pulse duration and repetition rate are distinct quantities; peak power is not the same as average power. The relationships are explained in the University of Illinois laser lecture. For a continuous-wave source, irradiance and dwell depend on delivered power, spot and motion. Scan speed, hatch spacing and repeated exposure then determine how those interactions build across the surface.
Increasing one setting can improve removal on a given sample and still worsen the accepted rate if it creates substrate change, leaves edge bands or forces extra inspection and rework. A useful parameter record therefore includes the source mode, measured or specified power basis, workpiece spot/working distance, pulse settings where relevant, scan and feed speeds, overlap, passes and the accepted surface result. It should not be reduced to a power number on a quotation.
Pulsed vs. Continuous-Wave Laser Cleaning: Why Rated Power Alone Is Not Enough
Pulsed and continuous-wave (CW) systems deliver energy differently. A short pulse can concentrate energy in time, but closely spaced pulses or repeated paths can still accumulate heat. CW exposure is continuous while the beam is on, but its effect on the part depends on dwell, spot, motion and material response. Neither mode has a universal speed or damage advantage.
For a fair choice, test both candidates, if relevant, against the same contaminant, substrate limits, geometry and acceptance endpoint. Compare accepted output over the same type of full cycle. If one configuration needs additional passes or a different safety arrangement, those conditions belong in the comparison. Rated watts alone cannot settle the buyer's production question.
How Do You Calculate Actual Laser Cleaning Throughput?
Calculate Accepted Area per Hour from a Complete Production Cycle
For an area-based job, use:
Accepted area rate (m²/h) = accepted target area (m²) ÷ measured complete-cycle time (h).
“Accepted target area” means the specified surface that passed the agreed checks. The denominator is the elapsed time within the test boundary, including the activities that boundary defines. If the test covers several parts, add only their accepted target areas and use the elapsed period for the same set. Do not mix a beam-on numerator with a shift-time denominator from a different run.
The result is a measured rate for the tested part mix and conditions. It is not automatically a guaranteed rate for thicker contamination, other geometries or another production schedule.
Calculate Accepted Parts per Shift
When the business requirement is part output, count the parts released during the defined shift: accepted parts per shift = number of parts that meet the agreed endpoint within that shift. Record the scheduled shift length, actual run time, part mix, rejects and rework. If area per part varies, an area rate alone will not describe capacity.
A short trial can inform a planning estimate, but it cannot by itself prove an eight-hour shift result. An estimate needs explicit assumptions about availability, setup, replenishment, inspections, part variation and handoffs. A buyer who needs a shift commitment should request a representative extended run or a documented production record rather than extrapolating a few minutes of beam-on time.
Worked Example: Demonstration Rate vs. Accepted Production Output
Hypothetical example—not an Oceanplayer Laser test or machine specification. A flat demonstration coupon has 0.25 m² of target area. It is visibly cleaned during five minutes of laser-on time. The reported demonstration area rate is 0.25 ÷ (5/60) = 3.0 m²/h of laser-on coverage. That number says nothing yet about a production part's acceptance or handling.
Suppose a later representative trial processes four parts, each with 0.25 m² of target area. The logged 54-minute complete cycle includes 24 minutes of primary cleaning, eight minutes of extra passes, 12 minutes of handling and repositioning, six minutes of inspection, and four minutes of rework. All four parts then meet the defined endpoint. Accepted area is 1.00 m², so the measured complete-cycle rate is 1.00 ÷ (54/60) = 1.11 m²/h, or four accepted parts in 54 minutes. The difference comes from a different geometry, endpoint and time boundary—not from a proved percentage loss inherent to lasers.
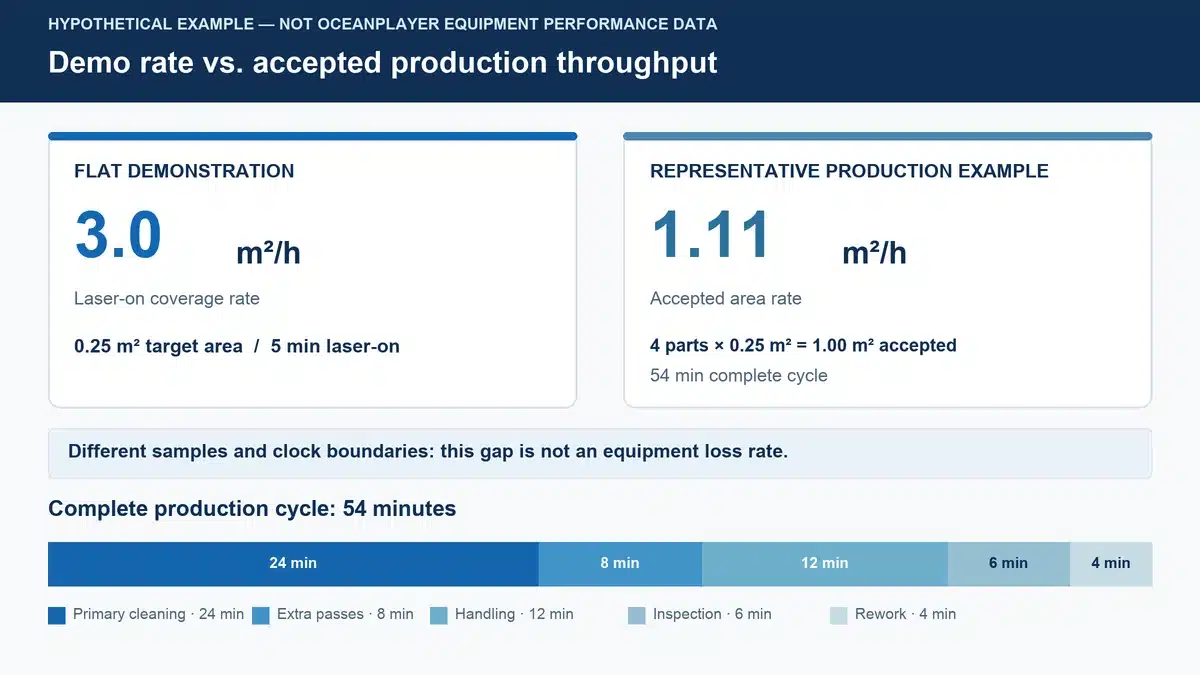
Do not apply another “utilization” or “first-pass yield” multiplier to 1.11 m²/h: the 54 minutes already includes handling, inspection and rework. If one of the four parts had remained rejected, both the accepted area and accepted part count would need to fall. To claim parts per shift, measure or transparently model the actual shift rather than multiplying this short-run result by eight hours without further evidence.
How Should Buyers Test Laser Cleaning Speed Before Purchasing?
Select Representative Parts and Define Acceptance Criteria
Choose samples that cover the conditions likely to govern production: the substrate and finish, contamination range, relevant thickness or adhesion, part geometry and the regions that must be reached. Include a normal part and, where practical, a difficult but realistic one. A perfectly flat coupon may help compare recipes, but it cannot represent a recessed production component on its own.
Before the run, record the release condition: what must be removed, what may remain, what substrate change is unacceptable and what test or inspector decides. If the customer requires a welding, painting or bonding outcome, identify the applicable downstream qualification separately. This prevents a visually impressive pass from being counted as accepted output under an unstated standard.
Record Cleaning Parameters, Pass Count, and Cycle Time
Use a simple run sheet. Record sample ID, starting condition, machine/source configuration, working distance and spot basis, power and pulse settings where relevant, scan pattern, hatch spacing, head or part feed, number of passes and any change of recipe. Also record the safety enclosure or controlled work arrangement and extraction used in the test.
Start and stop the clock at the agreed points. Keep laser-on time and complete-cycle time in separate fields. A run with different operator assistance, fixturing or access arrangements must be labeled as such rather than merged into a single headline rate.
Measure Accepted Output and Document Rework
After each run, record the target area or part count inspected, how many passed, which regions failed and why. Log additional passes, touch-up, repair and rejects. Retain photographs or measurements when the acceptance method calls for them, with the sample and viewing or measurement conditions identified.
The output report should show raw runs as well as any summary. If a failed first pass becomes acceptable after rework, it contributes to accepted output only when the full rework time is in the same clock boundary. This keeps the numerator and denominator honest.
Repeat Trials Under Comparable Production Conditions
Repeat enough runs to expose relevant part and process variation. The appropriate count depends on the variability of the incoming parts and how precise a capacity commitment must be; there is no universal number for every cleaning task. With a small set, show the individual results and range instead of presenting a percentile with false precision.
When the installation includes a factory acceptance test or site acceptance test, compare the recorded part mix, recipe, work area, operator or automation arrangement, inspection method and time boundary. A changed coating batch, fixture or acceptance endpoint may justify a new test. The point is not to make two environments artificially identical; it is to show which difference explains any change in accepted output.
What Evidence Should Support a Supplier's Cleaning Speed Claim?
Demonstration Videos vs. Test Reports vs. Production Records
A video can show that a visible effect occurred on a particular surface. Unless it identifies the starting condition, full elapsed time and inspection result, it cannot establish accepted production throughput. A controlled test report is stronger when it includes the sample, configuration, raw times, acceptance decision and failed runs. A production record adds evidence about repeated operation and actual handling, provided its part mix and quality rules match the buyer's job.
These are different levels of evidence, not a reason to dismiss a demo. A demonstration is useful for screening whether a process is plausible. The buyer should then ask for the next level of evidence before relying on a capacity figure in a purchasing decision.
What to Include in a Supplier Throughput Comparison Sheet
Use the same fields for every candidate supplier or configuration. A compact sheet can make hidden differences visible:
| Field | Record for each candidate |
|---|---|
| Input and part | Material, contamination or coating, distribution, geometry and target area. |
| Accepted endpoint | Removal target, permitted substrate change, method of inspection and decision owner. |
| Configuration | Laser mode and relevant parameters, working distance, scan strategy, fixture, controls and extraction. |
| Time and output | Laser-on time, complete-cycle boundary, accepted area, accepted parts, passes, rework and rejects. |
| Transfer conditions | Operator/automation, part mix, repeated-run variation and changes that require retesting. |
Compare the accepted output and the conditions behind it, not just the highest single-run number. If one candidate was tested on a cleaner sample or with a looser endpoint, ask for a matched retest before ranking the machines.
Agree on Acceptance Criteria and Retest Conditions
Before purchase, agree on the part family, representative sample plan, acceptable surface, inspection method, minimum accepted output if a minimum is needed, timing boundary and how rejected or reworked parts are counted. State which configuration changes or input variations trigger another trial. These are project-specific engineering and procurement terms, not universal laser performance values.
A useful final request to a supplier is concrete: provide representative parts or drawings, the contaminant and its range, the downstream requirement, the planned work arrangement and the output the line needs. Those inputs make a meaningful test possible. Without them, an apparently precise cleaning-speed quotation is still only a conditional estimate.
Frequently Asked Questions About Laser Cleaning Speed
Can a Flat-Surface Test Predict Production Cleaning Speed?
It can help screen a recipe on a known layer and substrate, but it rarely predicts a complete production cycle by itself. Edges, recesses, fixturing, handling and inspection may change both the time and the accepted result. Use the coupon to identify a plausible process window, then measure representative parts under the intended arrangement before using a rate for capacity planning.
Does Higher Laser Power Always Mean Faster Cleaning?
No. More available power can support a faster process under some matched conditions, but accepted throughput also depends on spot size, delivery mode, scan path, contamination, substrate limits and extra passes. A setting that removes material quickly but damages the surface or increases rework does not improve accepted output. Compare qualified runs, not rated watts alone.
Why Does the Same Laser Clean Different Materials at Different Speeds?
The laser interacts with the surface layer and substrate together. Layer thickness, adhesion and optical or thermal response affect how much exposure is needed and what change the base material can tolerate. Geometry and the required finish also alter the path and acceptance decision. The same machine can therefore have different qualified recipes and output rates on different jobs.
How Many Test Runs Are Needed to Estimate Production Throughput?
There is no useful universal count. A stable, uniform part family may require fewer exploratory runs than a mixed lot with variable contamination and access. Decide first how much variation matters to the purchasing decision, then retain every raw run, failure and rework event. A few runs can screen feasibility; a capacity commitment needs a sample plan and operating duration appropriate to the actual variation.
Technical References
- ISO 8501-1:2007, visual assessment of steel surface cleanliness. Used only to illustrate a scoped visual preparation criterion for applicable steel coating work.
- ISO 8502-9:2020, conductometric assessment of water-soluble salts on steel. Used only to illustrate that some coating specifications require a different surface test from visual inspection.
- ISO 11553-2:2026, safety requirements for hand-held or hand-operated laser processing machines. Used only for its defined equipment scope; the actual installation needs its own applicable safety assessment.
- Health Canada, Laser Products. Used for the limited statement about Class 4 beam and possible fire hazards.
- Kang et al., A Hierarchical Structure of Key Performance Indicators for Operation Management and Continuous Improvement in Production Systems (2016). Used to distinguish good quantity, rework and time in production measurements; it is not a laser-cleaning rate study.
- Influence of ns-Laser Cleaning Parameters on the Removal of the Painted Layer and Selected Properties of the Base Metal. The cited experiment concerns paint-coated Q345 steel under its stated nanosecond-laser setup; it is not Oceanplayer Laser performance evidence.
- University of Illinois, laser lecture slides. Used for the distinction among pulse energy, repetition rate, average power and peak power.